How a granule bagging line keeps 25 kg sack dispatch steadier in a busy woven-bag warehouse: fewer handoffs, cleaner feeding, steadier weighing, and a more controlled outfeed path from bag setup to pallet flow.
Old workflow: too many handoffs, too much waiting
Manual sack presentation, separate weighing and transfer steps, and loose outfeed control usually slow down a granule line. That is why searches for фасовочная линия, фасовочно упаковочная линия, or упаковочная линия для сыпучих продуктов all point to the same need: steadier output, less spill risk, and fewer operator corrections.
Why this bagging layout fits granules better
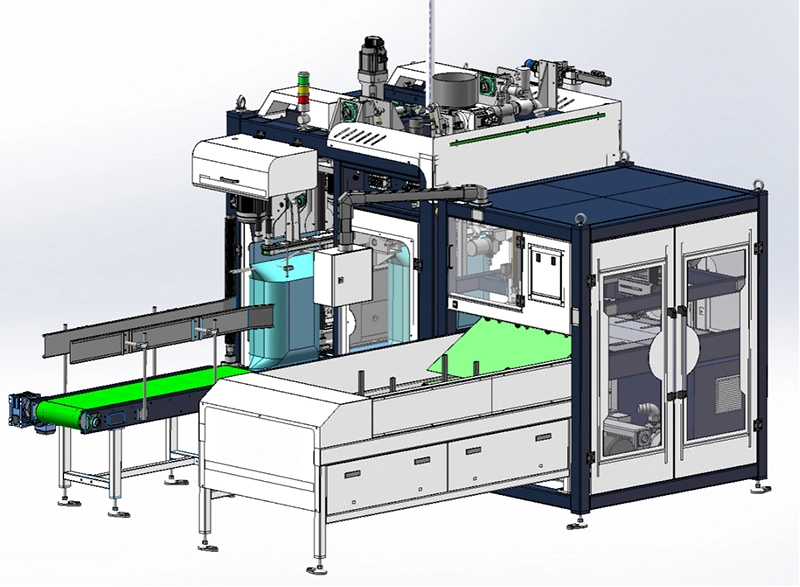
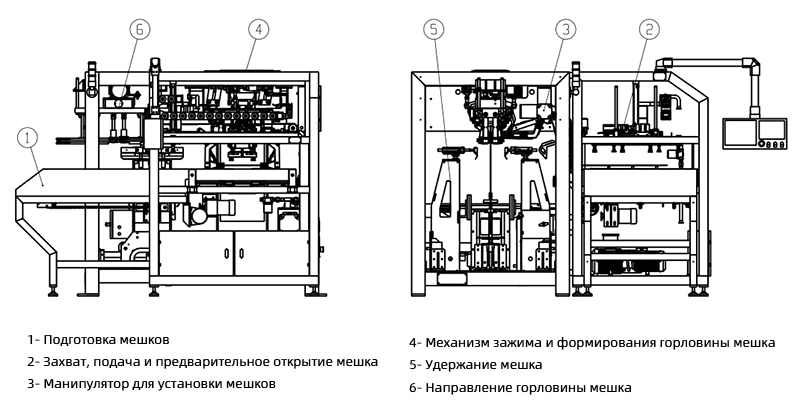
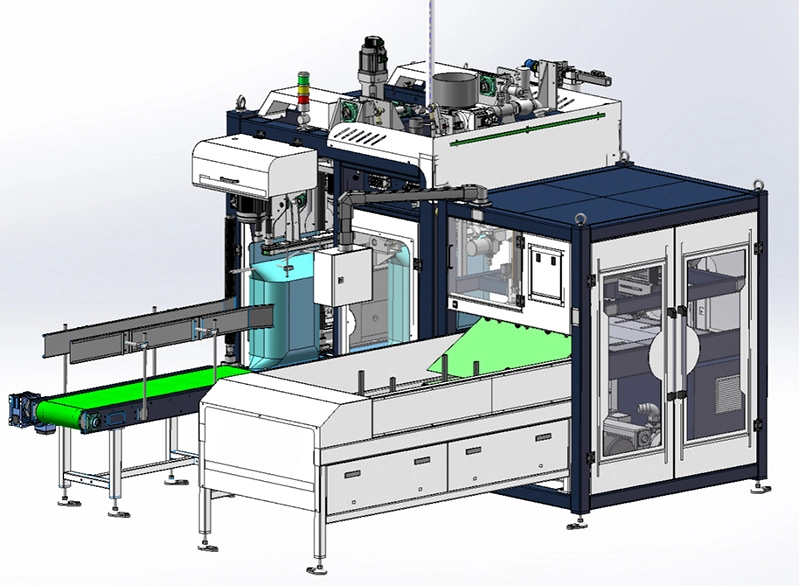
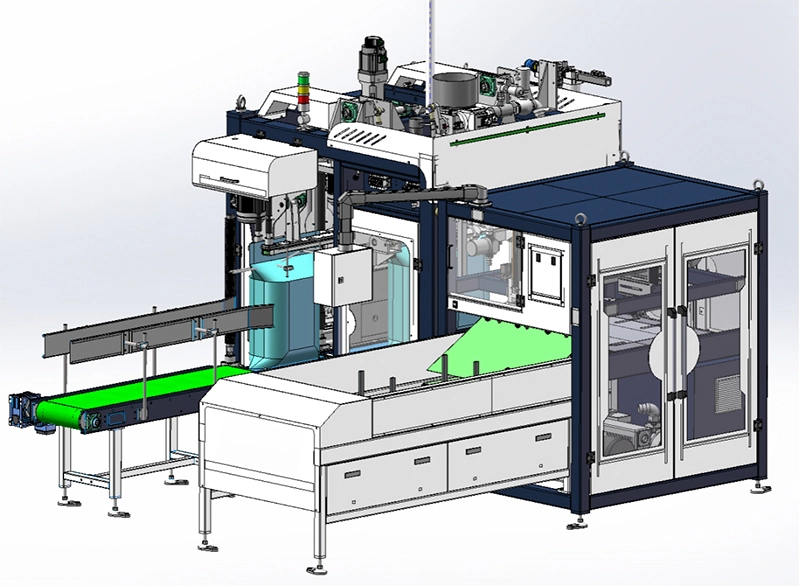
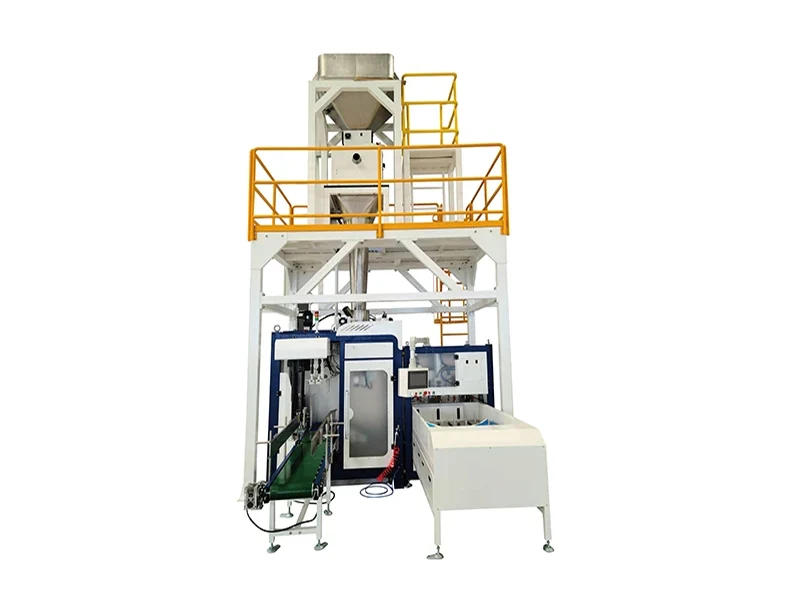
The image set shows a compact working unit with a bag magazine, guided bag handling, control-side operation, and a discharge conveyor. This structure reduces re-gripping, lowers transfer loss, and keeps the sack moving in one planned direction.
Evidence from structure and operating scene
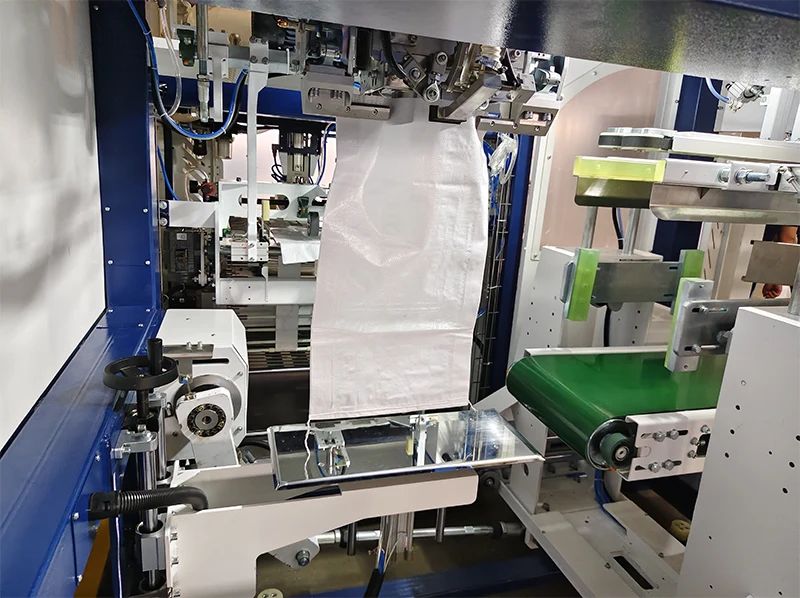
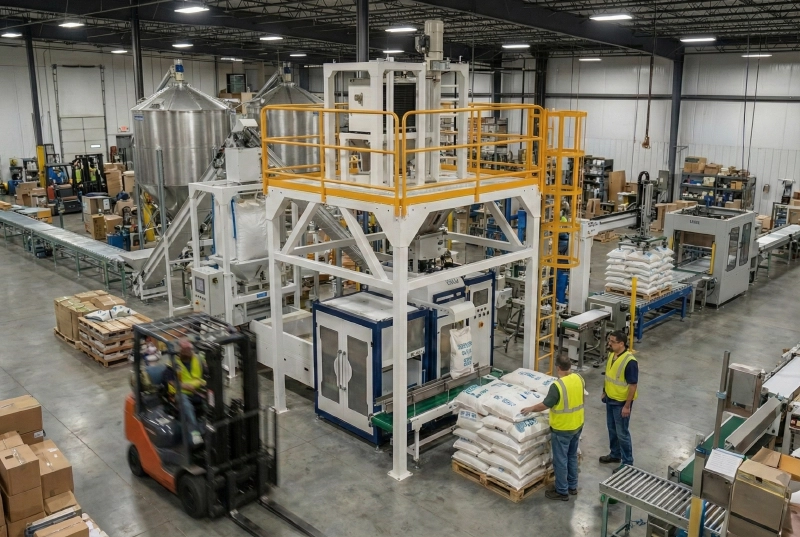
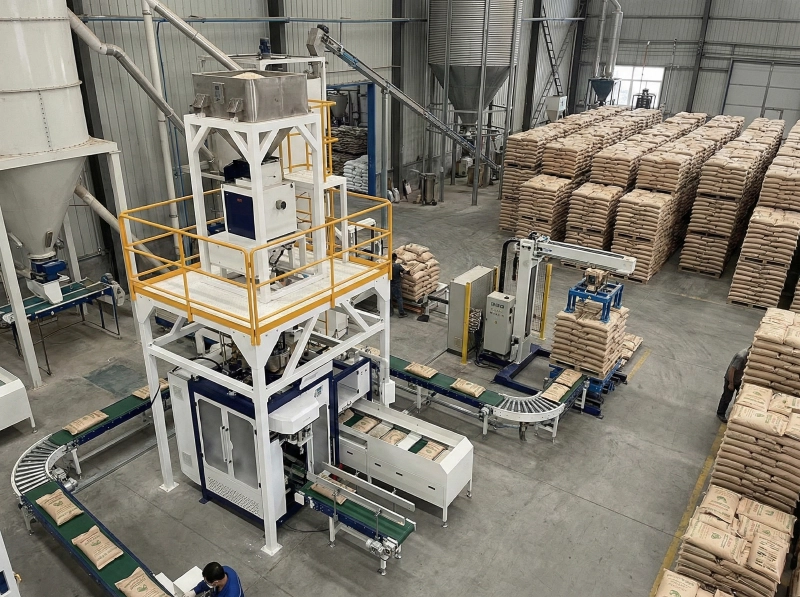
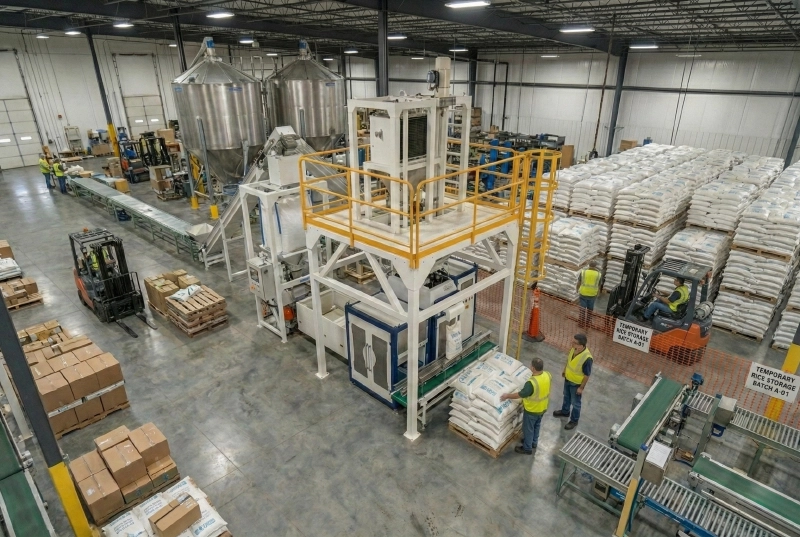
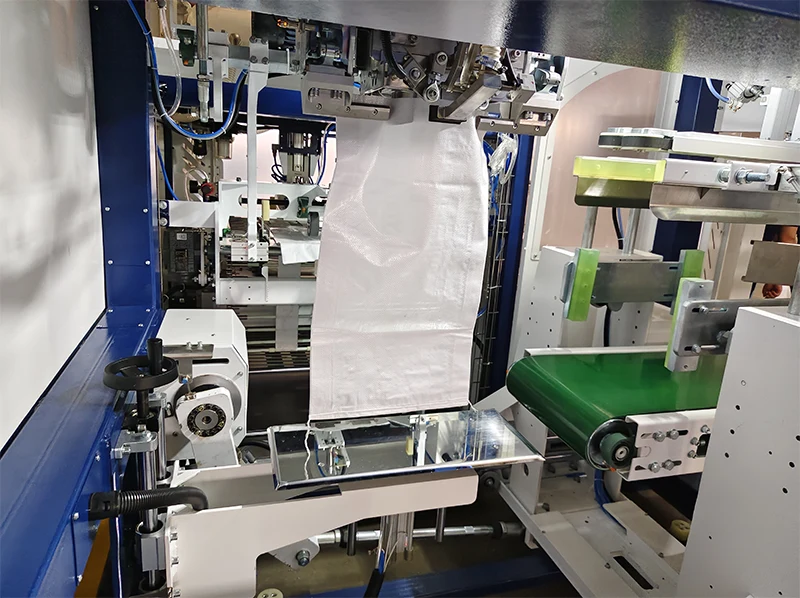
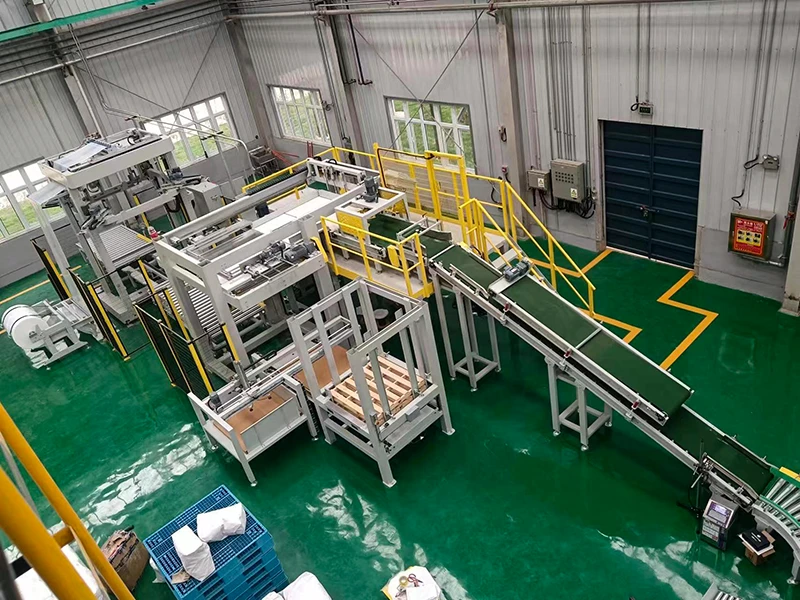
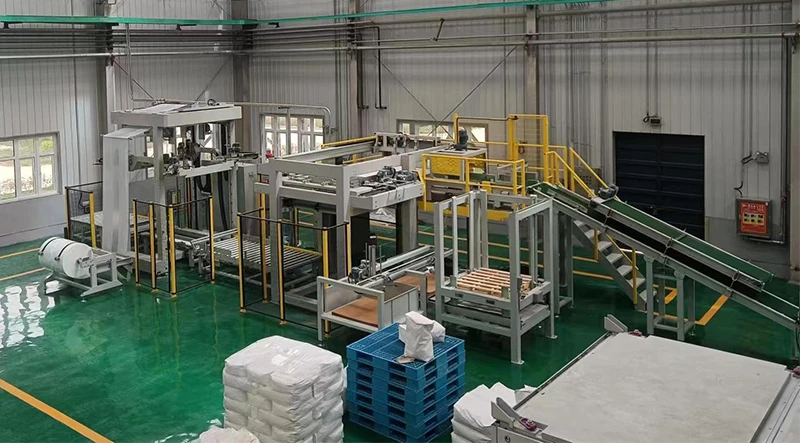
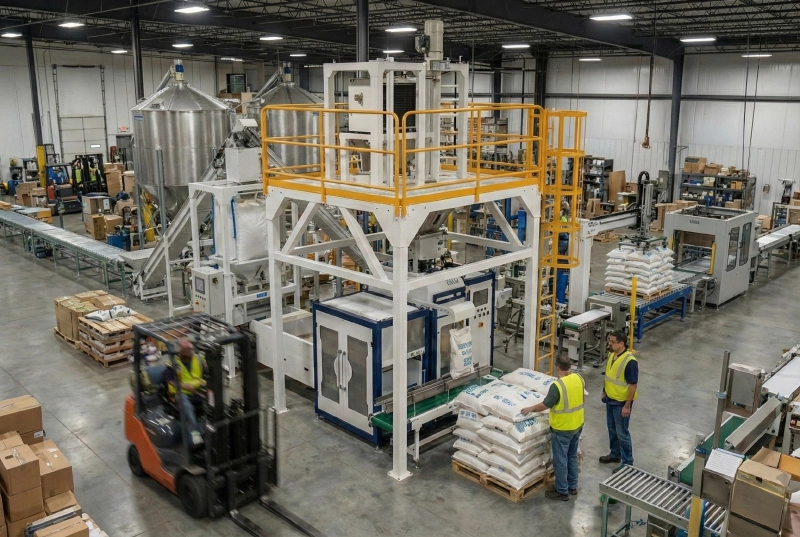
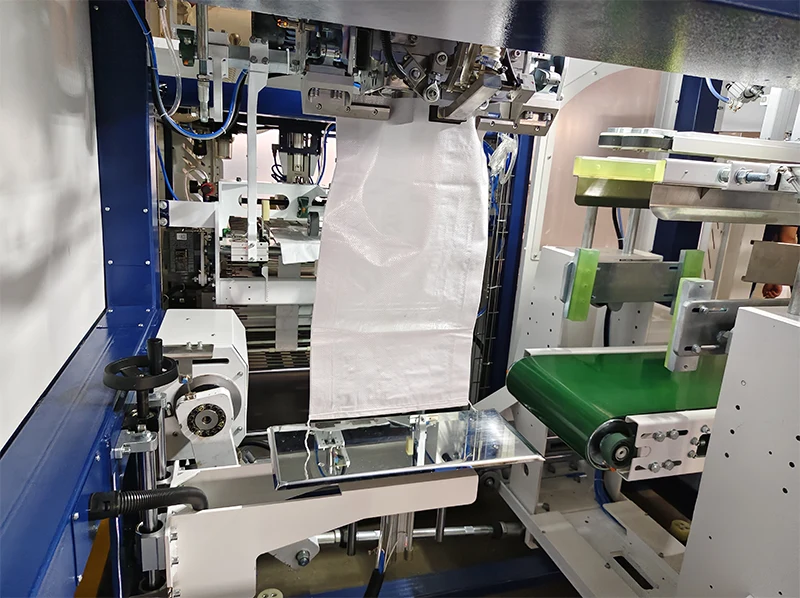
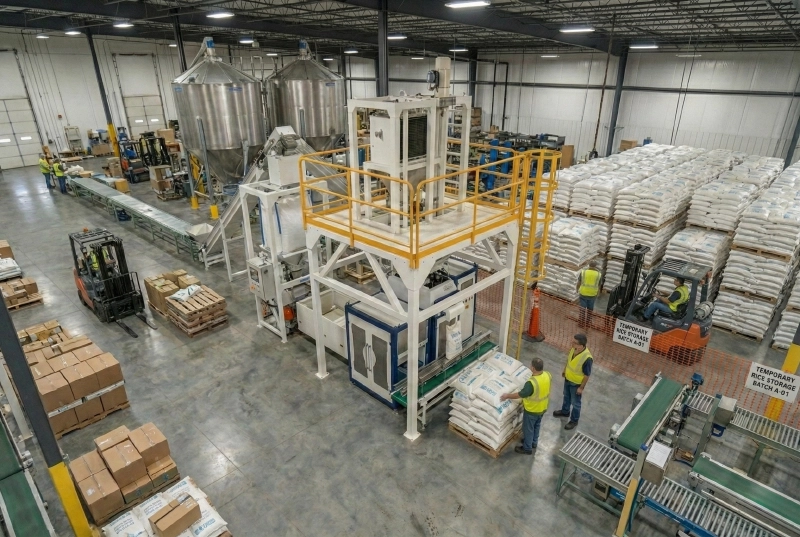
The internal close-up shows vacuum suction cups and a robotic placing arm holding the woven sack before filling. The high-angle factory scene shows the line working with forklift movement and pallet handling. The 3D render shows the bagging line feeding a robotic palletizer without breaking the packing rhythm.
What result the buyer gets
For a grain, feed, salt, or mineral warehouse, the result is steadier 25 kg sack dispatch, fewer manual corrections, a cleaner bag transfer path, and a line layout that supports higher throughput without turning the workshop into a congestion point.
When a warehouse needs steadier output for 25 kg sacks, the real problem is not only filling speed. The line also has to keep feeding stable, dosing accurate, bag handling clean, and discharge organized enough that the next pallet move does not slow down the whole shift.
Why manual 25 kg bagging starts to break down
In powder and grain workshops, 25 kg filling often begins as a practical manual job: one operator feeds, one operator weighs, one operator ties or sews, and another person clears the finished sack. That works for a short run, but it quickly creates three familiar issues. First, the feed becomes uneven, so the weight drifts. Second, the bag mouth gets twisted or poorly aligned, so closure quality becomes inconsistent. Third, the transfer area turns messy, which makes stacking and forklift movement slower than the filling itself.
This is exactly where a фасовочная линия for bulk products earns its keep. The target is not only a bag on the pallet. The target is a cleaner rhythm: stable feed, controlled dosing, aligned bag handling, and a discharge path that keeps the 25 kg sack moving without unnecessary rework.
Why this ppline layout fits 25 kg sacks better
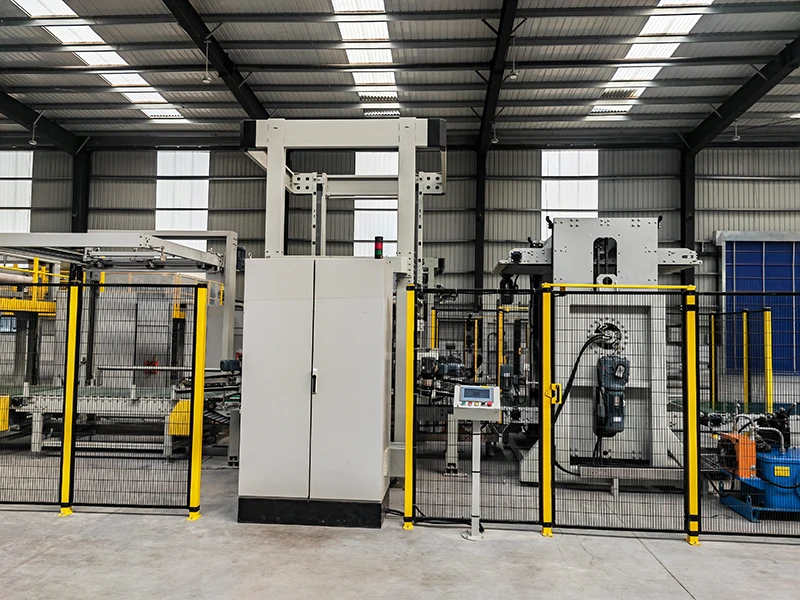
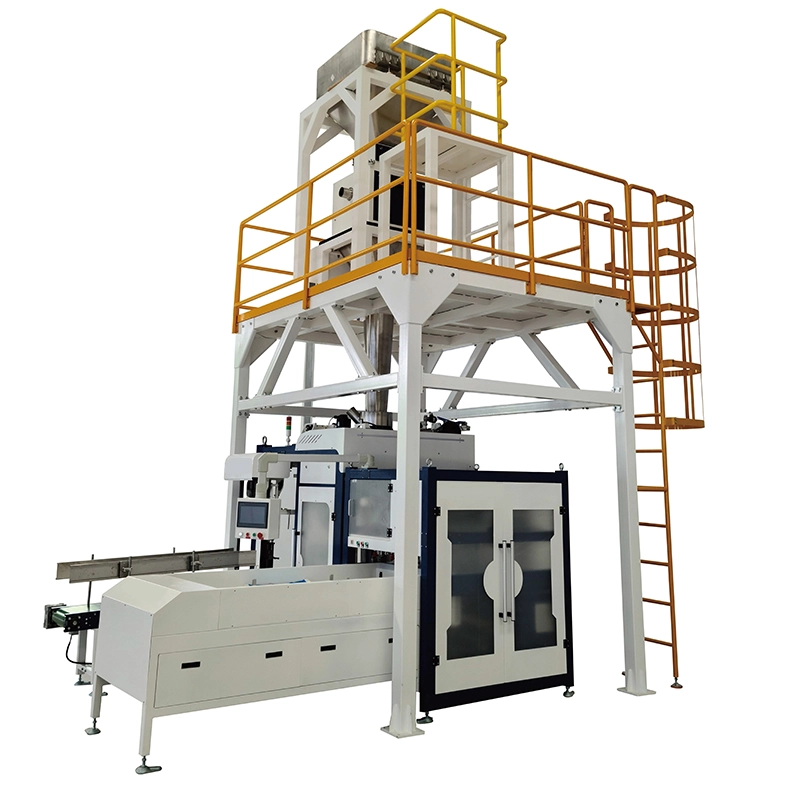
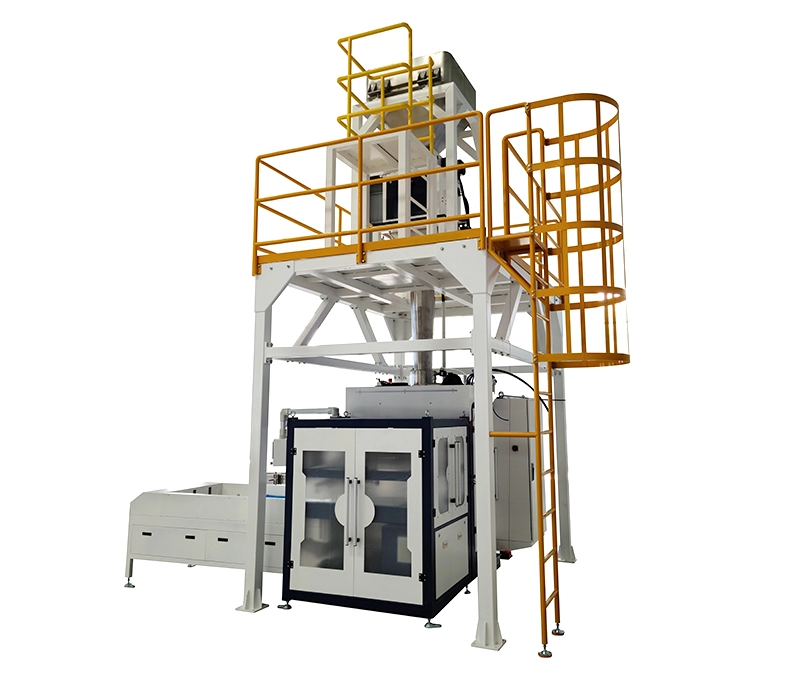
The ppline layout is built around the physical flow that bulk products need. A hopper feed and gravity dosing section reduce the chance of sudden surges. The elevated steel framework keeps the machine body organized and makes maintenance easier to access. The enclosed cabinet protects the working zone, while the swing-arm HMI gives the operator a clearer control point without crowding the bagging area.
The key advantage is that the line treats the sack as part of the process, not as an afterthought. Bag clamping, opening, filling, and discharge all stay in one controlled sequence. For 25 kg applications, that matters because the bag is heavy enough to punish weak handling, but still light enough that any wasted motion shows up fast in output per shift.
What the bagging workflow looks like on the floor
On the floor, the sequence is straightforward. Product enters from the storage side, the machine keeps the feeding zone stable, the operator controls the run from the HMI side, and the outfeed belt carries the filled sack away from the filling point. That separation matters. It keeps the front end focused on accurate packaging while the back end focuses on handling and dispatch.
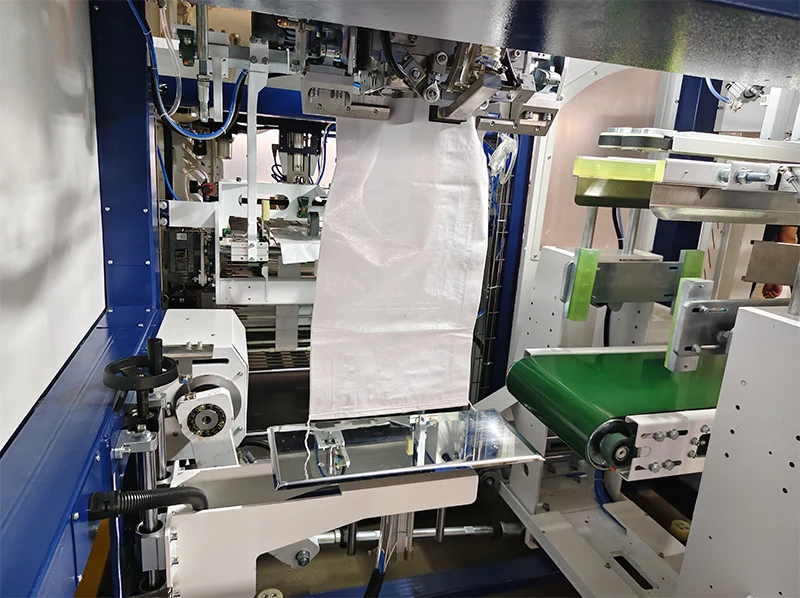
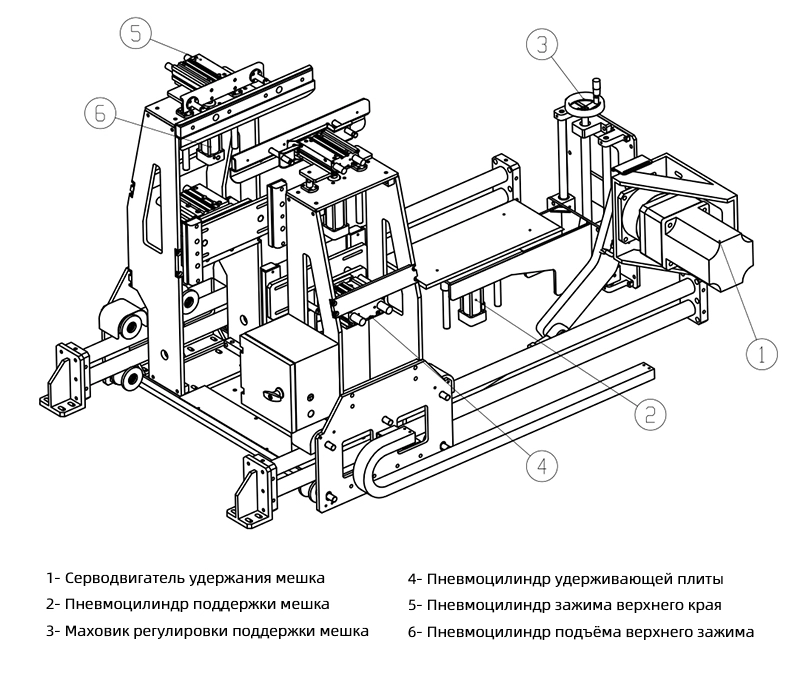
The close-up internal structure shows why this flow stays cleaner. Vacuum suction cups and the placing arm help the woven bag open and sit correctly before filling. The green conveyor and adjustment hardware support the bag path so the sack does not fight the machine. In practice, that means fewer bad starts, fewer bag mouth corrections, and less time lost at the sealing or stitching station.
Image evidence: the structure behind steadier output
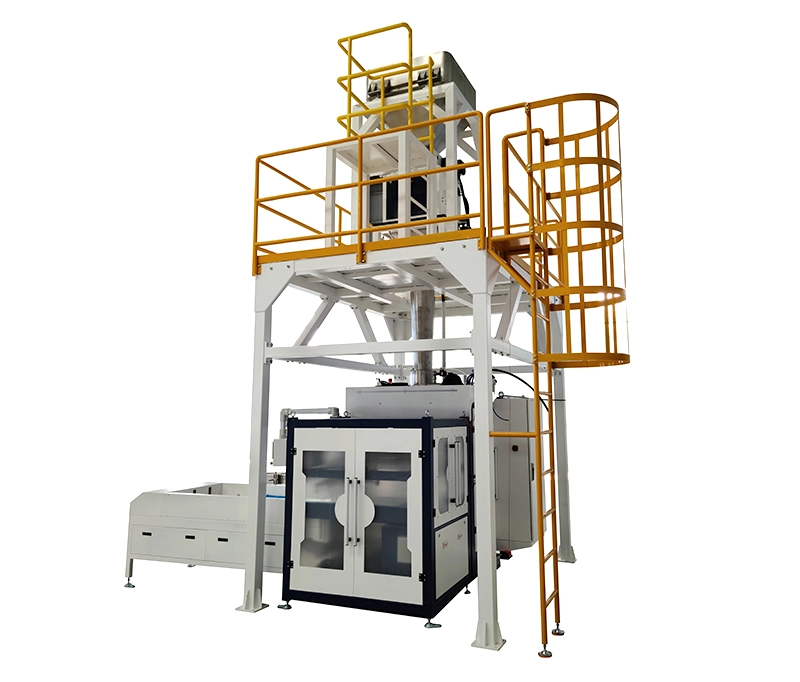
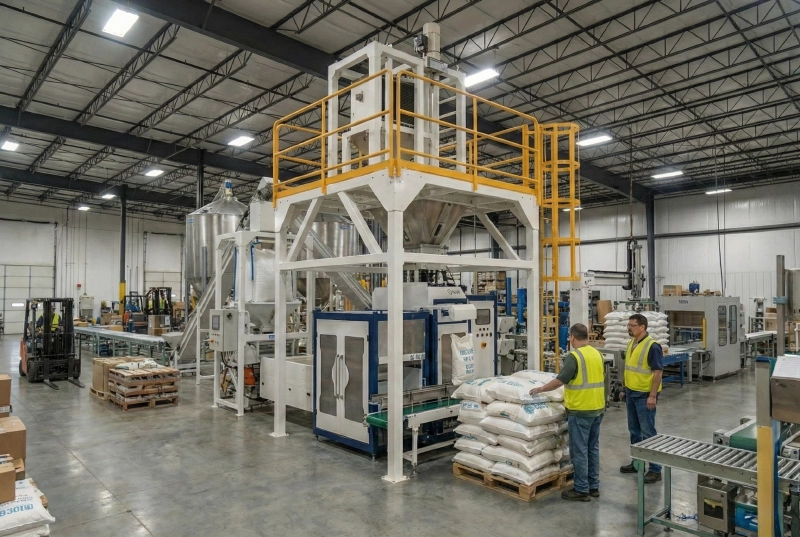
The product photos and workshop views point to the same conclusion: a steadier 25 kg line comes from structure, not slogans. The twin silos and conveyors keep upstream supply organized. The platform and safety cage ladder support access and maintenance. The enclosed cabinet and visible control panel reduce operator friction. And the discharge conveyor keeps the sack moving so the filling zone does not become a bottleneck.
For bulk product packaging, that structure is what turns a rough process into repeatable production. Whether the material is grain, powder, pellets, or a mixed bulk product, the line must keep the same three things under control: weight, bag mouth behavior, and transfer timing.
Quick configuration check for a 25 kg bagging project
Project question
What the line needs
Почему это важно
How steady is the feed?
Hopper feed plus gravity dosing
Reduces weight drift and operator correction
Can the bag mouth stay aligned?
Bag clamping and suction-assisted opening
Improves sealing or stitching consistency
Will the shift stay organized?
Outfeed conveyor and clear transfer path
Keeps the filling zone from backing up
Is the machine easy to run?
Swing-arm HMI and enclosed control cabinet
Simplifies control and protects the working zone
Result: steadier sacks, cleaner transfer, less rework
For a warehouse running 25 kg sacks, the real value of a bagging line is not one isolated number. It is the combined result of steadier dosing, cleaner bag handling, safer access, and a smoother discharge rhythm. That is what helps a team keep output more predictable across the full shift and makes the line easier to integrate into palletizing, storage, or shipping work.
If you are planning a фасовочно упаковочная линия for bulk products, the right starting point is to match the feed style, bag closure method, and transfer flow to the material itself. Once those three parts are aligned, the rest of the plant becomes much easier to manage.
Why an FFS Packaging Line Keeps Pellet and Polyethylene Bag Output Steady Without Manual Trimming
For pellet and coarse powder jobs, the real test is not whether a machine can make one good bag. It is whether the line keeps forming, filling, sealing, and discharge moving at the same pace shift after shift, with PE or PP roll film and no one standing by to clean up bag edges by hand.
Start with the film path, not with the bag at the end
Manual trimming usually shows up when the film path is loose, the bag form is inconsistent, or the next station pulls at a different speed from the previous one. That is why an FFS line works better for steady pellet output than a set of separate stations stitched together on the floor. The bag is formed inside the machine from roll film, then filled and sealed in one chain. There is less handling, fewer drop points, and fewer chances for the bag mouth to drift out of square.
For bpmpack FFSline, the usable film and bag range matters. The brief calls out PE or PP roll film, a normal film width of 350-450 mm, a maximum roll outer diameter of 1500 mm, and a 150 mm inner core. Film thickness sits in the 0.14-0.18 mm range for regular projects. Those numbers are practical, not decorative. They tell you whether the film feed will stay calm enough for a clean form-fill-seal cycle on pellet, granule, or coarse powder jobs.
Practical point: if the process still needs people to touch each bag before it leaves the station, the line balance is off. A stable FFS setup should take care of film forming, dosing, sealing, and discharge in one flow.
What usually breaks the flow?
Bagging lines lose stability when the feed changes too fast, the transfer section is too exposed, or downstream equipment waits for the bagger instead of matching it. The result is familiar: people trim, reposition, re-stack, and recover from minor drift all day. That is labor you do not get back.
Keep the discharge steady before you worry about the pallet
FFSline is meant for continuous output, so the feed side needs a buffer and the back end needs a clear path. The project brief mentions a 3 m³ surge hopper, which is what helps the line hold material while the machine works through the next cycle. That buffer is useful when pellets flow well but the upstream supply is still uneven. It also helps with coarse powders that move well enough for FFS, but still need a bit of protection from sudden feed changes.
The other detail that matters is control. FFSline uses PLC plus a touch screen, so the operator is not guessing where the slow-down comes from. When the target is 20 kg, 25 kg, or 50 kg bags, the line should stay on the same logic across the whole shift. The brief lists 10-50 kg as the working range, with project references around 500 bags/h and higher material-dependent figures in some cases. That is enough to plan around, but the real target should still be tied to the product, bag size, and film spec.
Once the bag leaves the sealer, the line should not leave it hanging. A good setup can connect to incline conveyors, reject and recheck stations, palletizing, pallet label printing, stretch hood, and dust collection. That is how the packaging line stays steady after the bag is formed. If the back end waits in line, the front end starts to drift, and someone ends up trimming or correcting by hand.
Match the line to the output, not the other way around
For pellet and polyethylene bag output, the machine spec should match the materials first. If the roll film width is too narrow, the form drifts. If the bag weight range is too ambitious, filling becomes unstable. If the palletizing section is not ready for the output rate, the whole line slows down and the front end starts looking messy. That is why FFSline is best treated as a line design problem, not just a packaging machine purchase.
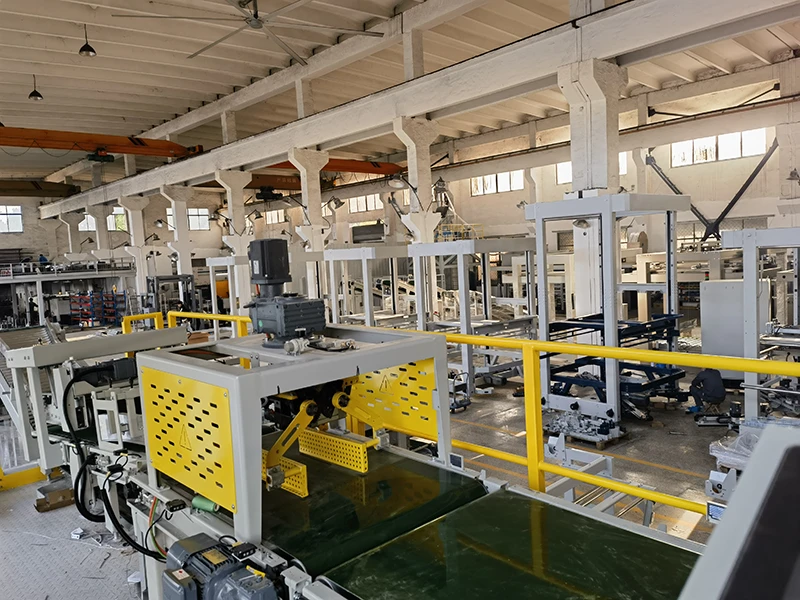
The wide workshop layout also matters. It gives space for service access, safety rails, conveyors, and the downstream equipment that keeps the bag stream moving. The point is not to make the line look busy. The point is to keep the process calm enough that operators do not need to correct every bag by hand.
Planning item
Почему это важно
What it prevents
PE / PP roll film
Matches the FFS forming path
Loose bag shape and edge drift
350-450 mm film width
Fits the planned bag size
Excess trimming and unstable mouth formation
3 m³ surge hopper
Buffers uneven upstream feed
Stop-start filling and weight swings
PLC + touch screen
Keeps operation visible and repeatable
Guesswork during speed changes
Need a steadier FFS line for pellets or polyethylene bags?
Share the bag weight, film spec, and target output. bpmpack can map the forming, filling, sealing, and downstream flow into one line plan instead of leaving the end of the process to manual correction.
На участке фасовки порошка у белорусского производителя главный риск был не в самом наполнении мешка, а в том, что мешок приходил к следующей операции неровно. До сшивки пакет мог смещаться, заваливаться на кромку или терять геометрию после передачи от одного узла к другому. В итоге оператору приходилось делать ручную подправку, а это замедляло линию и ухудшало стабильность выпуска.
Именно для таких задач и была выбрана упаковочная линия Mipline для порошка. Ее задача — не просто подать мешок, а удержать его в контролируемом положении от точки передачи до сшивки и дальнейшего вывода. Для порошковой продукции это критично: мешок должен идти ровно, без лишней вибрации, без закусывания кромок и без потери устойчивости на переходах между участками.
Почему старая схема давала сбой
Типичная проблема на линиях для порошка — слишком резкий переход между подающим и принимающим узлом. Если мешок идет по неудачно согласованной направляющей, он теряет ось, начинает разворачиваться и требует участия оператора. На короткой смене это кажется мелочью, но на длинной партии такие микрозадержки превращаются в постоянные потери времени.
Еще один слабый момент — недостаточная жесткость и слабый контроль бокового положения. Когда мешок идет по легкой рамной конструкции без нормальных направляющих и без понятной зоны стабилизации, любое отклонение сразу отражается на передаче к следующей операции. Для белорусского производителя сухих смесей это было особенно чувствительно: нужен был не просто конвейер, а ровный, предсказуемый участок подачи.
Что в Mipline оказалось подходящим
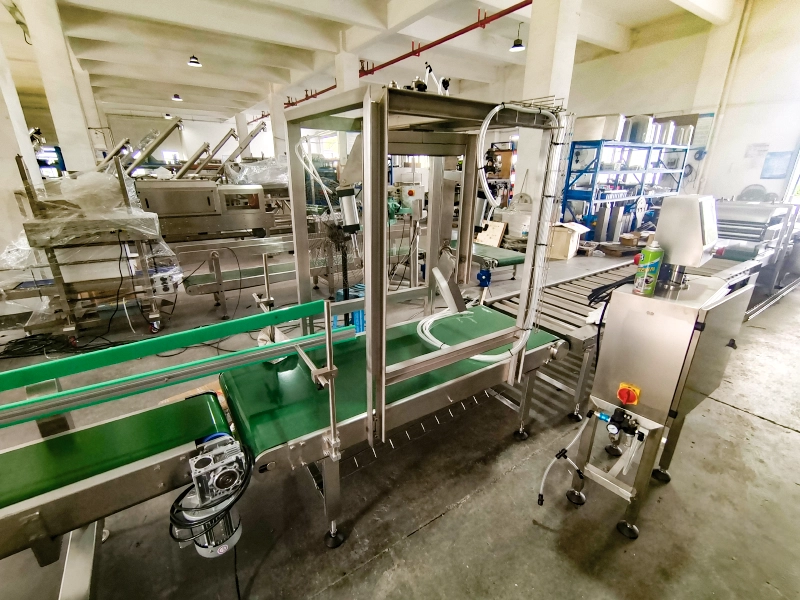
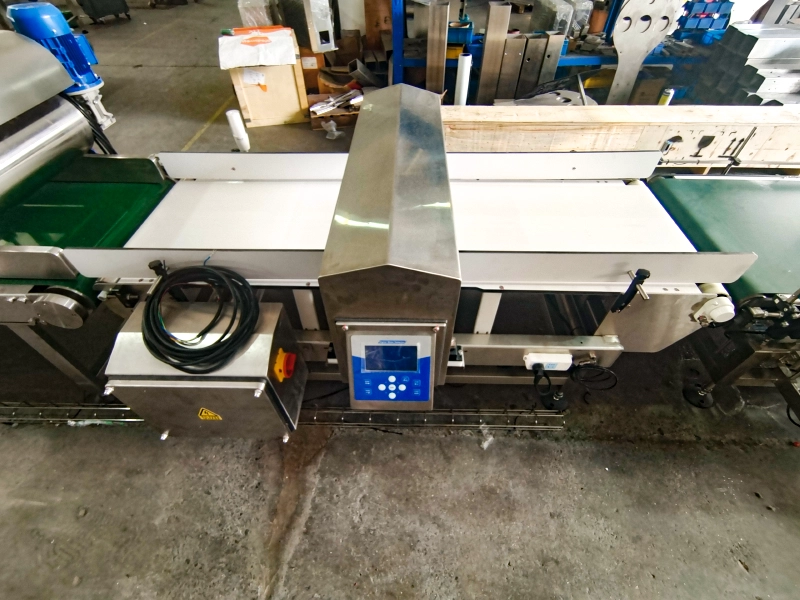
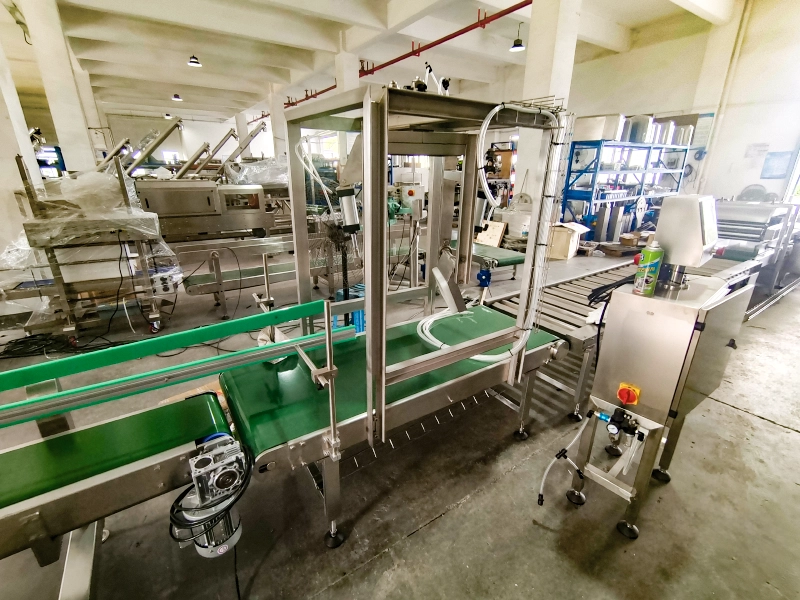
На фото видно, что линия собрана на нержавеющей раме, а рабочий участок дополнен зелеными транспортными лентами, вертикальной направляющей рамой и отдельным блоком аварийного останова. Такая компоновка полезна именно там, где мешок должен сохранять траекторию и не гулять по ширине. Жесткая геометрия каркаса снижает паразитные смещения, а направляющие помогают удерживать пакет в оси перед следующей операцией.
Вторая важная деталь — визуально понятная и сервисно удобная конструкция. Оператору проще контролировать линию, когда у него есть четкий доступ к зоне подачи, понятные границы транспортного канала и отдельный блок управления. Это снижает вероятность случайных остановок и упрощает обслуживание.
Какие узлы дают стабильность на практике
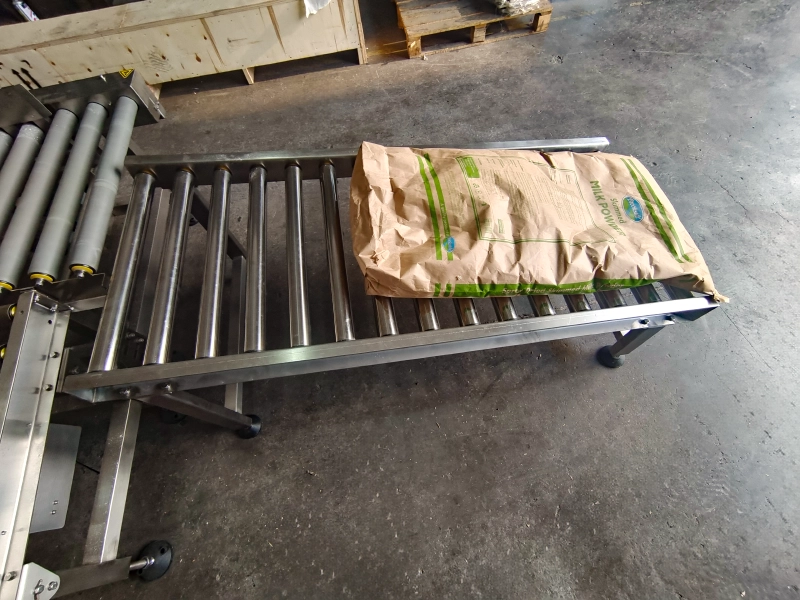
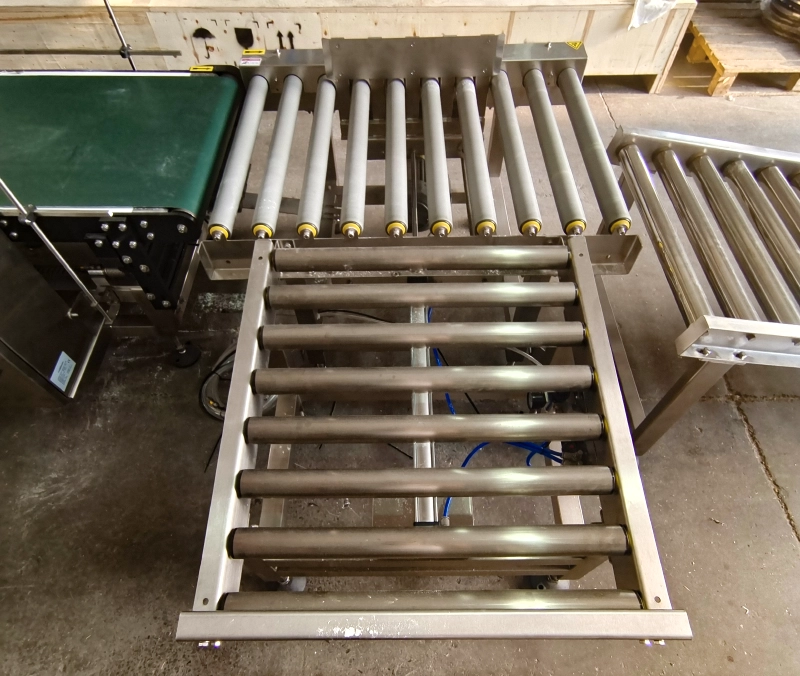
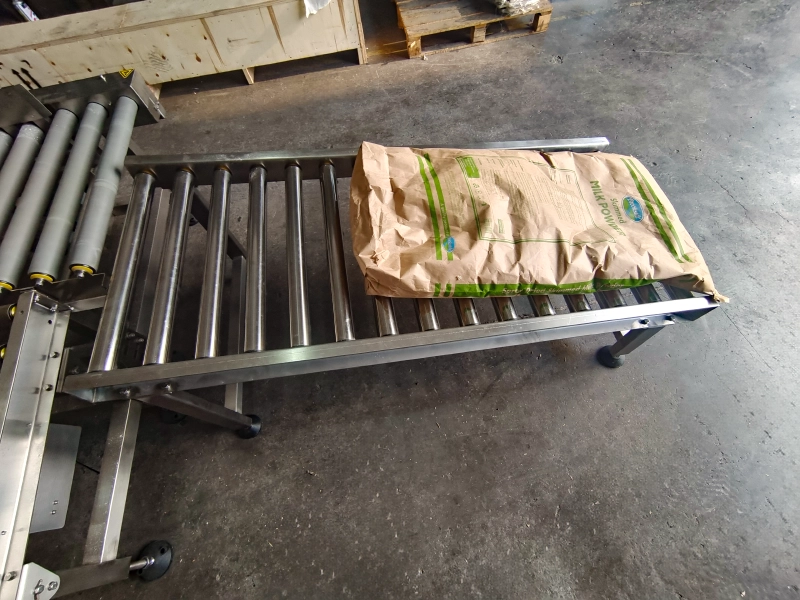
На второй фотографии видно, как мешок идет по роликовой секции на нержавеющем основании. Для порошковой упаковки это важный участок: мешок не должен проваливаться, цепляться за край или терять опору. Роликовая передача дает более мягкий и равномерный ход, особенно если перед ней уже выровнена подача и мешок вошел в рабочую линию без перекоса.
Именно сочетание роликовой секции, жесткого каркаса и согласованного направления движения убирает ручную подправку. По сути, решение работает не за счет одной «сильной» детали, а за счет правильно собранной связки: подача, удержание, передача и вывод идут как единая логика.
Для этого проекта это означало более спокойный ритм участка фасовки, меньше вмешательства персонала и более ровный мешок перед сшивкой. Там, где раньше оператор ловил положение вручную, теперь линия удерживает мешок сама.
Почему это важно именно для порошка
Порошковые продукты особенно чувствительны к нестабильной передаче. Любой перекос мешка делает кромку неудобной для следующей операции, а любая задержка на участке подачи бьет по общей производительности. Поэтому для упаковочной линии для порошка важен не только сам узел фасовки, но и весь путь мешка после наполнения.
Mipline здесь закрывает именно этот промежуток. Линия не пытается решать все задачи сразу, а точно фиксирует тот этап, где чаще всего теряется стабильность. Это и есть причина, почему решение подошло белорусскому производителю: мешок идет ровно, участок не требует постоянной ручной корректировки, а сшивка получает уже подготовленный пакет.
Итог для заказчика
В результате заказчик получил не просто еще одну транспортную секцию, а ровный участок подачи для порошковой линии. Это сократило ручную подправку, сделало передачу мешка стабильнее и помогло держать ритм участка перед сшивкой. Для предприятия, которое работает с порошковыми продуктами в промышленном режиме, такой эффект особенно ценен: меньше вмешательства, меньше простоя и более предсказуемый выпуск.
Если задача на вашей стороне звучит так же — удержать мешок ровным до сшивки и убрать ручную корректировку на порошковой линии, то Mipline можно рассматривать как практичное решение именно для этой точки процесса.
Для белорусского производителя сухого порошка главная проблема была не в самом наполнении мешка, а в том, что дальше мешок должен пройти короткий, но очень чувствительный участок: от подачи к зоне сшивки. Если мешок теряет геометрию, оператор тратит время на ручную подправку, а линия начинает жить рывками. На практике это означает лишние остановки, риск смещения шва и ненужную нагрузку на персонал.
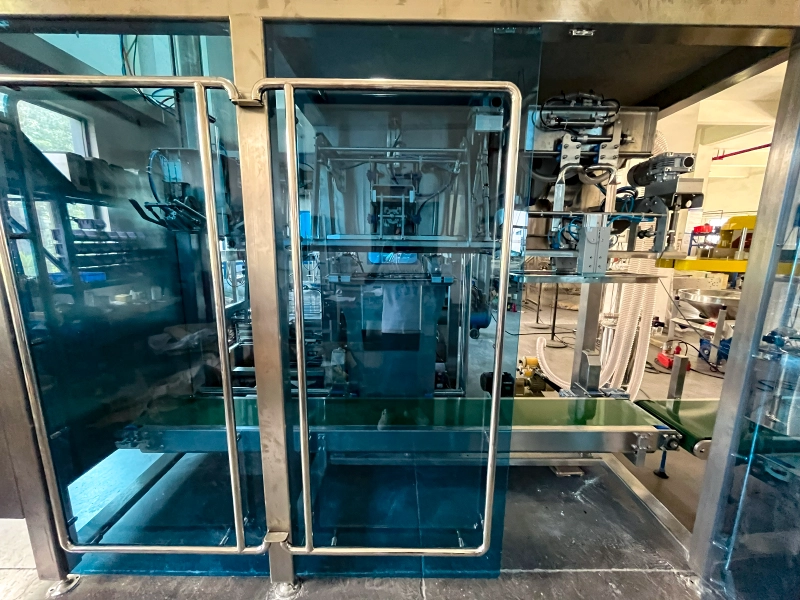
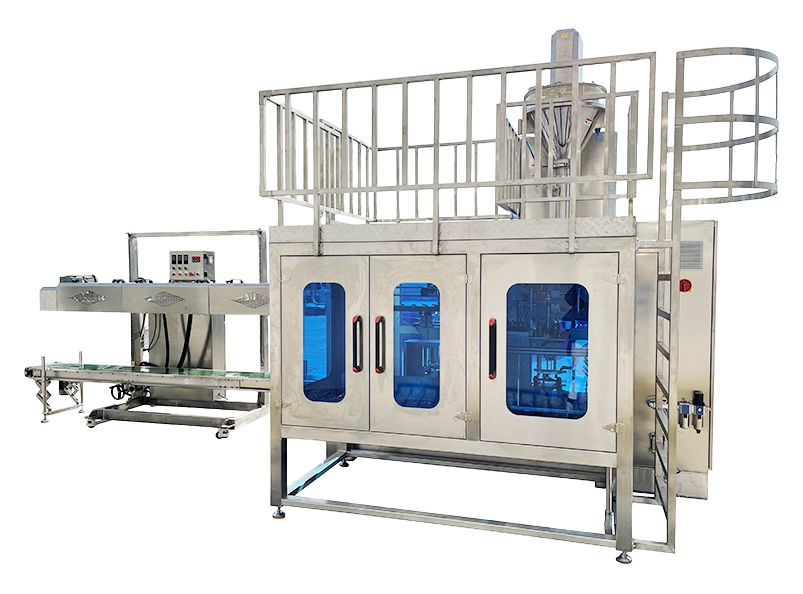
Mipline закрывает этот участок не «общими словами», а железом. На фото видно, что линия построена как закрытая нержавеющая система с безопасными дверями и интерфейсом конвейера. Это важно именно для порошка: поток должен идти внутри понятного контура, без открытых участков, где мешок может зацепиться, раскрыться или уйти в сторону до следующего поста.
Закрытая линия порошковой упаковки с защитным кожухом и понятным стыком к транспортеру.
Почему ручная подправка мешка ломает ритм линии
На старых участках мешок часто выходит из подачи уже с небольшим перекосом: край не сел в направляющую, дно повело, пакет чуть развернулся после захвата. Для оператора это выглядит как мелочь, но для линии это прямой стоп-фактор. Каждый раз, когда мешок нужно ловить руками, вырастает разброс по такту и снижается стабильность шва.
Поэтому в Mipline ставка сделана на контролируемую передачу. Сначала мешок удерживается и направляется в зоне подачи, затем его подхватывает межоперационный транспорт и только потом он уходит к следующему этапу. Такой сценарий лучше подходит для сухих порошков, где любая лишняя тряска сразу влияет на форму мешка и на аккуратность дальнейшей сшивки.
Станция мешковки с закрытым кожухом и зеленым конвейером на входе.
Что на фото показывает подачу мешка без лишних движений
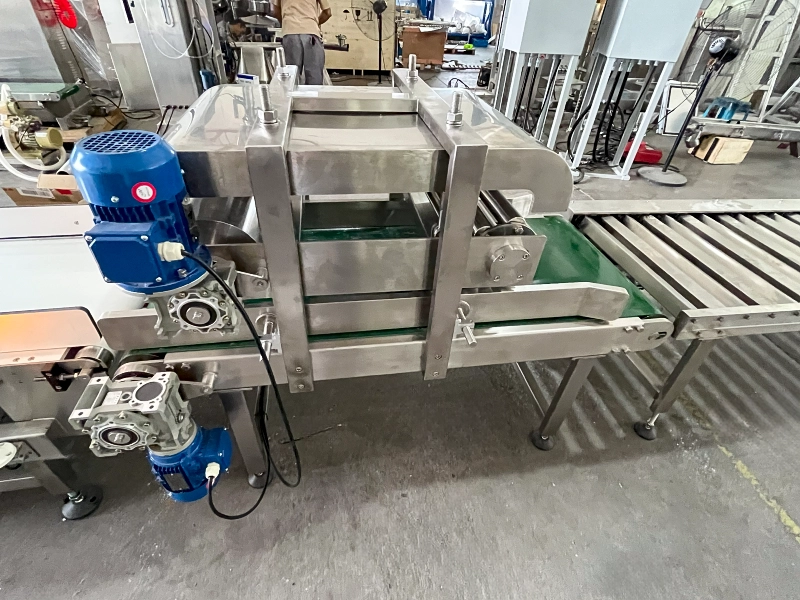
На одной из ключевых фотографий виден конвейер подачи мешков с двумя редукторными приводами и рамой захвата. Для линии порошка это важная конструкция: привод работает не один разово, а как стабильный транспортный узел, который удерживает мешок в заданной траектории и не дает ему «гулять» перед следующей операцией.
Именно такая механика помогает свести к минимуму ручное выравнивание. Когда мешок идет по заданной оси, оператору не нужно поправлять его после каждого перехода. Линия становится ровнее, а downstream-пост получает уже подготовленный мешок, а не проблемную заготовку, которую еще надо ловить на месте.
Подающий конвейер с двумя приводами и рамой захвата для стабильного перемещения мешка.
Двухленточный перенос: удержать мешок в центре, а не просто перевезти его
Следующий участок — двухленточный передаточный конвейер с центральным кожухом и регулируемыми направляющими. Это уже не просто транспортировка, а именно выравнивание. Две ленты дают более уверенную опору по ширине, а направляющие помогают удерживать мешок в центре даже тогда, когда геометрия упаковки немного плавает после заполнения.
Для белорусского производителя порошка такой узел особенно полезен, когда линия работает с разными партиями мешков или с небольшими отклонениями в упаковочном материале. Вместо того чтобы перекладывать ответственность на оператора, Mipline берет стабилизацию на себя: мешок проходит участок одинаково, а форма подачи сохраняется до стыка со следующим постом.
Двухленточный передаточный узел с центральным кожухом и регулируемыми направляющими.
Роликовая стыковка как спокойный финал перехода
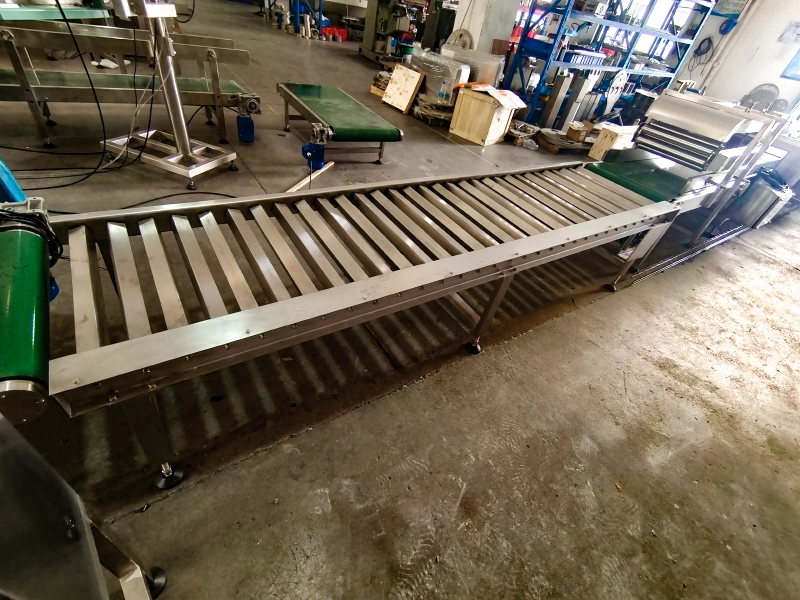
Последний визуальный узел в этой серии — секция роликового транспортера для плавной передачи мешка между постами. Именно здесь хорошо видно, что линия проектировалась не как набор разрозненных машин, а как единый маршрут для мешка. Роликовая секция убирает резкий переход, сглаживает перемещение и помогает мешку не терять направление на самом чувствительном отрезке.
Если смотреть на задачу глазами производства, то ценность такого узла простая: меньше рывков, меньше ручной коррекции, меньше причин для брака на стыке. А если смотреть глазами эксплуатанта, то это еще и более понятная работа линии в течение смены: оператор меньше вмешивается, такт становится предсказуемее, а мешок приходит к сшивке уже в рабочем положении.
Роликовая стыковочная секция для спокойной передачи мешка между рабочими постами.
Итог для порошковой линии
В случае с Mipline результат строится не на красивой подаче, а на понятной механике: закрытая нержавеющая оболочка, узел подачи с приводами, двухленточная стабилизация и роликовая стыковка. Вместе они решают ровно ту проблему, с которой сталкивается любой производитель порошка на реальной линии: мешок должен идти дальше без перекоса и без ручной борьбы за геометрию.
Для OOO BELRUSPRODUKT это означает более спокойный переход от подачи к сшивке, меньше пауз на поправку мешка и более ровную работу участка, где обычно теряется больше всего времени. На порошковой упаковке это и есть практический результат: не просто отгрузить мешок, а передать его дальше в стабильном состоянии.
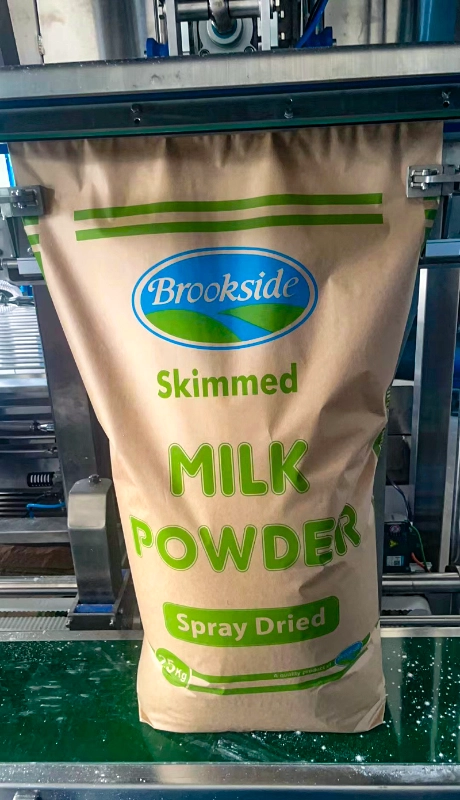
Why a Belarusian Dairy Powder Producer Chose a Cleaner Bag Handoff Before Sewing
On a 25 kg powder line, the hard part is not filling the sack. It is handing the bag over in a straight, calm position so the sewing head can work without manual correction. Mipline was selected to solve that transfer point first.
The old handoff problem was mechanical, not cosmetic
For a dairy powder producer, the bag rarely fails at the filling point. The real trouble starts after filling, when a kraft paper sack must travel from the bagging station to the next operation without twisting, folding, or dropping out of square. If the mouth is skewed, the operator has to correct it by hand. If the bag body bends too early, the sewing head loses consistency. If the transfer is rough, the whole rhythm of the line slows down.
This is why the customer brief was not just about higher output. It was about a more disciplined interface between the powder packaging line and the downstream sewing step. The goal was simple: keep each 25 kg bag supported, aligned, and ready for the next motion without extra touching.
What was hurting the line
When the sack arrives crooked, the sewing head becomes the bottleneck. Manual straightening adds labor, introduces small timing errors, and creates a wider quality gap between the first good bag and the tenth bag. In powder packaging, that gap is expensive because it shows up as wasted motion, unstable line speed, and avoidable rework.
Why Mipline fit this line
Mipline matched the job because the machine is built around the transfer point itself. The enclosed bagging station with inspection windows protects the working area. The bag magazine conveyor and guided transfer section present the sack in a controlled way. The top access platform makes maintenance practical without turning the line into a cluttered manual station.
Just as important, the structure is not a loose collection of frames. The guide rails, conveyor interface, and clamp zone are arranged to keep the bag mouth square and the bag body stable. That is the difference between a line that simply moves product and a line that prepares product for the next step.
Engineering point: the line does not win by brute speed. It wins by removing the small misalignments that slow down sewing and create operator intervention.
What the floor images prove
The transfer conveyor image shows the real job of the middle section: move a heavy powder bag while keeping the body straight and the base supported. The clamp-station image shows the other half of the story: once the sack is held correctly, the operator or downstream device can finish the cycle without fighting the bag shape.
That is why the final result was not just a prettier machine layout. The production team got a cleaner handoff, less manual rework, and a more predictable rhythm between filling, transfer, and sewing. On a powder line, that usually means the line feels quieter, easier to supervise, and more repeatable shift after shift.
Line point
Mipline adaptation
Результат на производстве
Bag transfer
Guided conveyor handoff with stable support
Less skew and less manual straightening
Bag mouth presentation
Controlled bagging station and clamp zone
Cleaner alignment before sewing
Maintenance and safety
Enclosed frame with access platform and inspection windows
Safer service and easier line oversight
Need a cleaner 25 kg bag handoff on your powder line?
Send us the bag type, target throughput, and the next operation after filling. We will map the transfer, clamp, and guarding section to the line you already have, then show where Mipline can remove manual correction.
Когда на линии порошка мешок выходит из упаковочного узла с небольшим уводом, дальше это быстро превращается в ручную доработку: оператор ловит кромку, выравнивает пакет и только после этого отправляет его на следующий этап. Для белорусского производителя порошка именно этот участок и стал узким местом. Задача для Mipline была простой по смыслу, но жёсткой по исполнению: удержать мешок ровно, не потерять геометрию потока и передать пакет к прошивке без лишних касаний.
Узел подачи мешка с направляющей рамой и зелёными транспортёрами — именно здесь линия удерживает пакет в нужной оси перед дальнейшей передачей.
Что ломал старый сценарий
В старой схеме мешок часто приходил на переход под углом. Это означает сразу три проблемы: оператор тратит время на подравнивание, возрастает риск перекоса перед прошивкой, а сам переход начинает зависеть от человека, а не от механики. Для порошковой упаковки такой режим особенно заметен: мешок мягкий, шов на нём легко увести, а любое лишнее касание добавляет хаос в конце линии.
Поэтому здесь важен не только сам факт транспортировки, а именно стабильная геометрия передачи: мешок должен идти по линии, а не искать её.
Роликовый участок с мешком из крафт-бумаги показывает, как Mipline удерживает пакет в зоне транспортировки без лишнего ручного вмешательства.
Почему Mipline подошёл именно для порошка
В этой конфигурации линия опирается на жёсткую нержавеющую раму, направляющую геометрию и связку транспортных модулей, которые не дают мешку «гулять» по ширине. Зелёные ленты и роликовый переход работают как единая подача: пакет не рвётся с места, а спокойно переходит из одного участка в другой. Для оператора это означает меньше ручной правки и более предсказуемый конец цикла.
Отдельный плюс — закрытый и безопасный контур. Когда порошок идёт по линии, вокруг всегда есть пыль, риск контакта и вопрос удобства обслуживания. Поэтому на Mipline важны не только транспорт, но и ограждения, доступ к управлению и понятная компоновка вокруг узла.
Закрытая нержавеющая упаковочная линия с защитными дверями и интерфейсом транспортёра — это та среда, где порошковый мешок идёт стабильно и безопасно.
Что видно на реальной компоновке
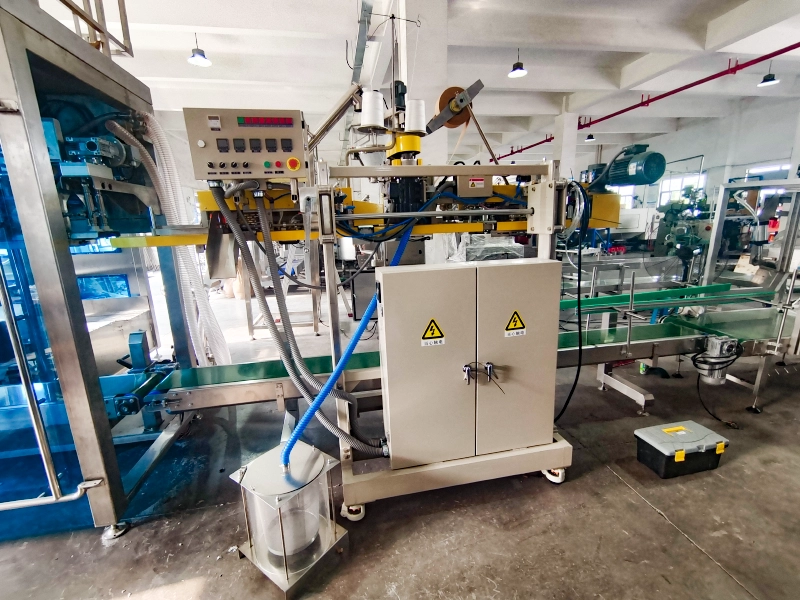
На фото с автоматической станцией хорошо читаются два практических решения: контрольная часть вынесена отдельно, а вакуумная линия помогает держать работу узла под контролем. Это важно для порошковой упаковки, потому что в конце линии оператору нужна не сложная логика, а понятная механика — чтобы мешок пришёл, был удержан и передан дальше без лишних остановок.
Именно поэтому Mipline в таких проектах выбирают не за «красивую подачу», а за рабочую связку: подача, фиксация, переход и дальнейшая передача на следующий этап.
Автоматическая станция с конвейером, шкафом управления и вакуумной линией подтверждает, что узел рассчитан на стабильную работу в составе всей линии.
Итог для линии клиента
Для белорусского производителя порошка результат был в том, что мешок перестал зависеть от ручной поправки на переходе. Линия стала вести пакет ровнее, участок прошивки получил более чистую подачу, а оператор — меньше лишних движений у транспортного узла. В таких проектах это и есть основной выигрыш: не абстрактная автоматизация, а конкретный участок, где Mipline убирает нестабильность и делает упаковку повторяемой от мешка к мешку.
When a bag leaves the filling point already skewed, the stitching head, conveyor transfer, and palletizing team all inherit the same problem. This article shows how a purpose-built bulk bagging line keeps the bag square from the hopper to the sewing station.
Integrated bagging equipment for bulk products that need controlled feeding, stable transfer, and a clean stitching finish.
Why the old setup fails first
A typical bulk-products plant often starts with a simple hopper, a manual bag correction point, and a stitching operator standing too far downstream. The result is familiar: the bag mouth arrives twisted, the product settles unevenly, the bag drifts on the conveyor, and the sewing head has to compensate for a problem it did not create. That is not a stitching problem. It is a transfer problem.
On higher-output shifts, operators also spend time nudging sacks back into position, which slows the line and adds avoidable handling. For materials such as salt, grains, pellets, or powder blends, even a small misalignment can affect seam quality, presentation, and pallet stability.
Why PPLINE fits this scenario
PPLINE is a better fit when the line must do more than simply fill a bag. The line needs to guide product from feed to discharge with enough control that the bag keeps its shape before sewing. The hopper-fed structure gives a stable starting point for dosing, while the elevated frame and conveyor routing help maintain a clean process line. The operator sees the process, but the machine does the alignment work.
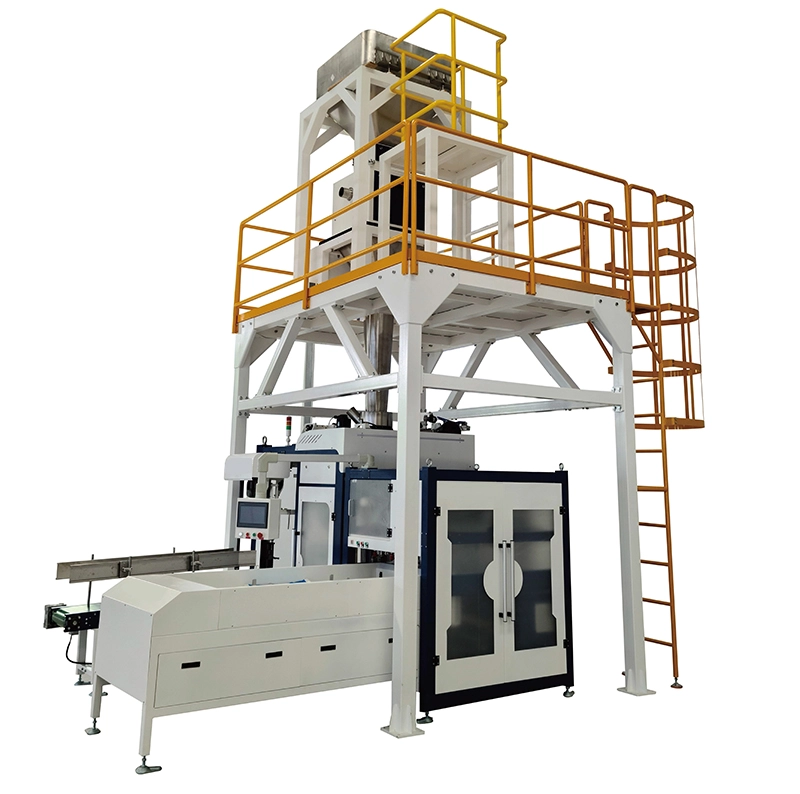
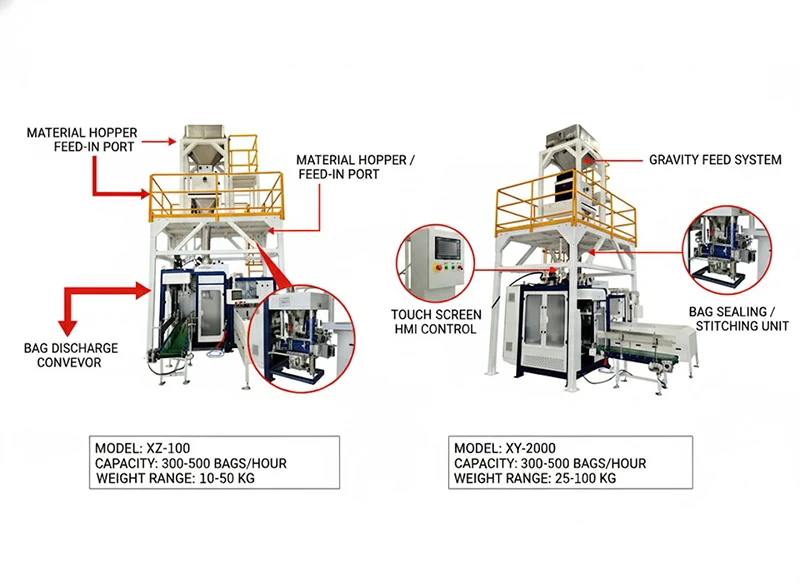
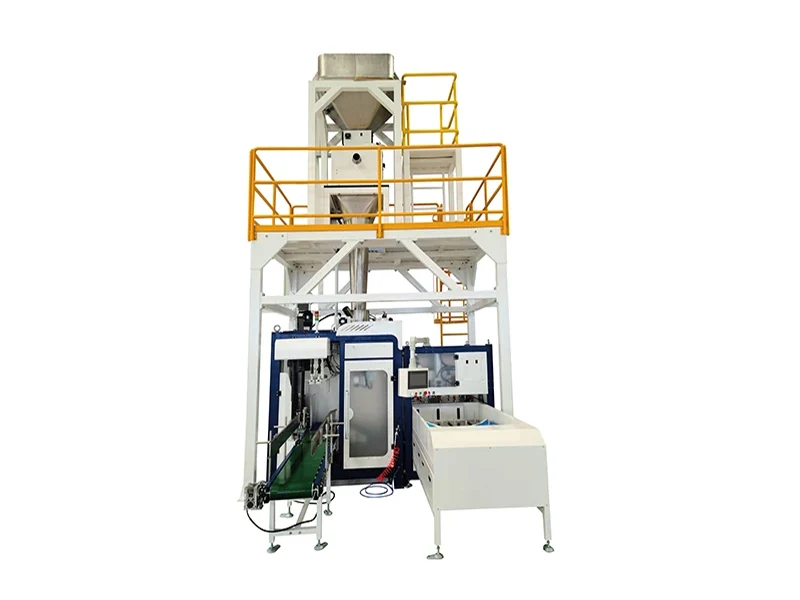
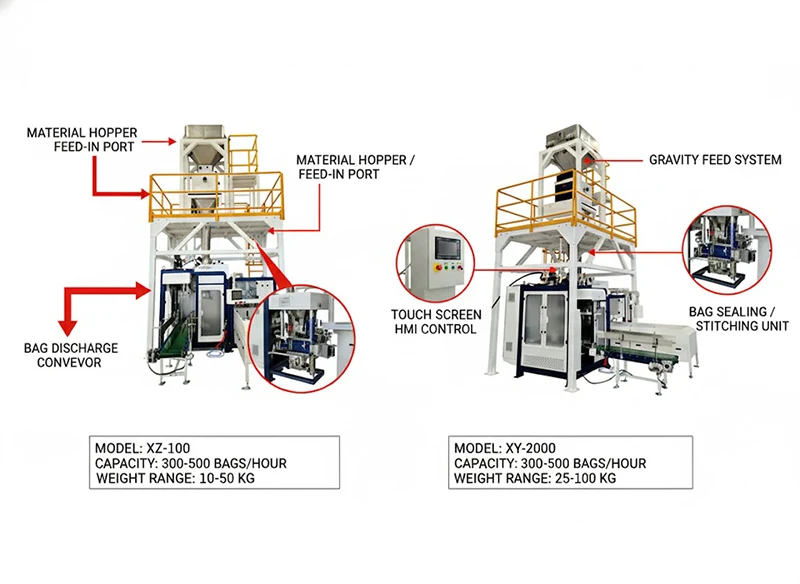
The image set matters here. The front-view bagging machine shows the hopper feed, the HMI touchscreen, the enclosed structure, and the optional sewing closure. The elevated platform image shows why service access, safe observation, and controlled material movement belong together. The internal close-up proves that the bag is not being guessed into position: vacuum suction cups, a pressing element, and a guided conveyor section are already working on the alignment before stitching begins.
Image evidence: what each unit is doing
The main bagging machine combines feed control, operator interface, and sealing or sewing output.The elevated platform and inclined conveyor support cleaner flow and easier maintenance access.The internal transfer zone shows how the bag is stabilized before it reaches the sewing stage.
Structure and parameters that solve the real issue
Feed pointHopper-fed input keeps material supply consistent and reduces sudden surges.
Transfer controlGuided conveyor movement and clamping help the sack stay straight before stitching.
Operator accessElevated frame and service platform allow inspection without interrupting the line.
Process visibilityHMI control keeps the operator close to the process without forcing manual correction.
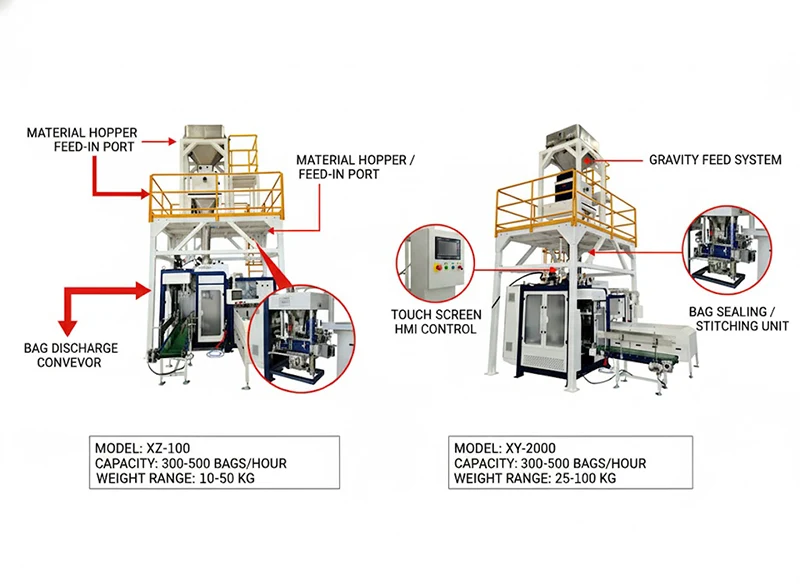
Throughput fitThe machine family shown in the image set is presented for 10-50 kg and 25-100 kg bulk bagging ranges, with 300-500 bags per hour configurations visible in the indexed materials.
That last point is important. When the application is bulk products, the line is not just judged by how fast it fills. It is judged by whether the bag arrives to the next station square, stable, and easy to stack. PPLINE’s frame, conveyor direction, and bag-handling logic are built around that requirement.
Final result at the plant level
For a Russian bulk-products plant, the practical result is not a fancy headline. It is fewer manual corrections, less seam rework, better bag appearance, and a smoother handoff to palletizing. The line becomes easier to run because the bag is controlled earlier in the process. The sewing operator no longer carries the burden of correcting a bag that arrived crooked.
In other words: the hopper starts the process cleanly, the frame keeps the path controlled, the conveyor preserves alignment, and the sewing station receives a bag that is already in the right position. That is the difference between a line that merely packs and a line that actually finishes the job well.
A modular layout can be adapted when the project needs accumulation, bag handling, and discharge coordination in one flow.
If your bulk-products line is losing time at the transfer stage, the first fix is usually not the sewing head. It is the bag path before sewing.
Stable bag alignment from hopper feed to the final stitch head
For a bulk-products plant, the real problem was not filling the bag. It was keeping the bag straight, calm, and predictable in the last meters before sewing. PPLINE is built for that exact handoff.
The line concept combines controlled feed, guided transfer, clamping support, and a clean discharge path so the operator does not have to rescue every second bag by hand. That matters when the product is dense, the pack weight is high, and the stitching area must stay in position.
The indexed machine set shows hopper feed, gravity dosing, HMI control, and a sealing or stitching unit in one view.
What usually goes wrong in the old setup
On older lines, the bag often leaves the filling zone slightly twisted, then drifts again on the short transfer before sewing. The result is familiar: crooked mouths, manual straightening, slower cycles, and a stitch head that works harder than it should.
In bulk-product packaging, that small instability creates a bigger business cost. The operator slows the line to protect the seam, the transfer conveyor accumulates bags, and the plant loses the smooth rhythm needed for steady output.
Bag mouth not centered before the stitch head
Product weight and bag inertia pulling the package off line
Extra manual correction between filling and sewing
Uneven output when the feed path is not buffered
Why PPLINE fits this job
PPLINE is a good match when the main requirement is not just packaging, but stable transfer. The indexed equipment set shows a controlled hopper feed, a gravity dosing / filling concept, a guided discharge conveyor, and a bag-handling zone designed to keep the bag position predictable.
The 1 (10) image is especially useful here: it shows a machine family rated at 300-500 bags per hour and designed for 10-50 kg or 25-100 kg packs. That is exactly the kind of range where bag handling becomes a mechanical problem, not a simple filling problem. The line has to hold the bag mouth, keep the bag body level, and hand it off without introducing twist.
That is why the structure matters. A stable hopper feed keeps the upstream flow consistent. The transfer zone reduces shock. The clamp and support zone takes the load off the seam area. Together, these features reduce rework and let the plant keep its target cadence.
Structure, parameters, and image evidence
Image
What it proves
Why it matters for the line
1 (10).webp
Hopper feed, HMI control, dosing, and sewing-ready discharge
Shows the full bagging concept and the operating range of 300-500 bags/h
2 (11).webp
Secondary bagging layout with accumulation belt and discharge conveyor
Provides a buffering zone so the bag stays aligned before the next transfer
2 (12).webp
Bag clamp, bottom support, pneumatic cylinders, and height adjustment
Keeps the bag body and mouth stable during the final positioning stage
1 (7).webp
Elevated platform, hopper, and inclined conveyor integration
Explains the cleaner feed path and the practical maintenance access
2 (17).webp
Running line with conveyor transport, operators, and palletized sacks
Shows the final plant result: steady output and less manual rescue work
Result: a cleaner final handoff and a steadier shift
When the plant stops fighting bag twist at the end of the line, sewing becomes more consistent, the operator intervenes less, and the conveyor can run at a more stable pace. That is the practical value of PPLINE for bulk products: not just moving product, but protecting the last handoff before the seam.
The indexed running-line photo confirms the result in real plant conditions: bags move, pallets accumulate, and the flow stays organized without turning every package into a manual correction task.
A Russian bulk-products plant needed a steadier handoff before the sewing station. The main pain was bag skew, unstable discharge, and too much manual correction after filling. PPLINE solves that by keeping the bag controlled from the hopper side through the conveyor discharge and into the sewing head.
Bag control starts at the internal gripping and positioning stage, not at the sewing head.
What was wrong with the old setup
The customer was working with loose, flowable material and woven bags that had to stay straight until stitching. On the old line, the bag often arrived slightly twisted, the discharge point was not stable enough, and operators had to fix alignment by hand. That created three repeat problems: lower throughput, inconsistent sewing quality, and more wear on the crew.
Bag mouth position changed during transfer.
Operators had to touch the bag before sewing.
Unstable discharge made the sewing station work harder than it should.
Why PPLINE fits this job
PPLINE is a good fit when the line needs more than basic filling. The value is in the handoff logic: material comes from the hopper and dosing side, the bag is supported and guided, then the outfeed section keeps it aligned for the next operation. That is exactly what a sewing-oriented bulk-products line needs.
Instead of treating packaging and sewing as two separate problems, PPLINE treats them as one continuous transfer problem. That is why the layout shown in the product photos matters: you can see the control cabinet, the conveyor path, the enclosed machine body, and the maintenance access points that keep the line stable in real production.
Structure and evidence from the images
The HMI, bagging body, and outfeed conveyor show a line designed for controlled transfer.The steel platform and safety cage keep the operator access point organized and safe.The full plant view shows how storage, transfer, and pallet handling connect in one layout.
What in the structure solves the problem
Элемент линии
What it does
Why it matters for sewing
Hopper and dosing section
Keeps feed steady before discharge
Prevents bag motion from becoming random at the exit
Enclosed main body
Protects the transfer path
Reduces manual correction and keeps the bag path more predictable
HMI touchscreen
Gives the operator direct control
Makes changeover and line tuning faster when bag behavior changes
Outfeed conveyor
Moves the filled bag in a straight line
Helps the bag reach the sewing station square and ready to stitch
Steel platform and safety access
Keeps maintenance practical
Supports stable uptime, which matters more than a pretty demo layout
What changed after the line was matched to the job
Once the line was organized around controlled transfer instead of loose discharge, the plant got a cleaner bag handoff, less need for manual bag straightening, and more stable sewing quality. The main gain was not only speed. It was consistency. For bulk products, consistency is what protects the downstream station, keeps labor under control, and makes the line easier to run shift after shift.
That is the real reason this PPLINE setup works for the customer scenario: it turns a difficult bag-transfer problem into a controlled packaging process with clear mechanical support, visible operator access, and a discharge path that is easier to trust.
Need the same kind of handoff stability?
If your bulk-products line has the same issue before sewing, we can match the layout, transfer method, and operator access to your material and bag format.
Live production is the final test: stable discharge, orderly stacking, and fewer corrections.
СТОП! ПРЕЖДЕ ЧЕМ ВЫ УЙДЁТЕ...
Не покупайте упаковочное оборудование без этого руководства.
Скачайте наш бесплатный Путеводитель по выбору и покупке 2026. Узнайте о 7 самых дорогостоящих ошибках в спецификациях (которые в среднем обходятся покупателям в $40К+).
✓ Матрица подбора оборудования (гранулы/порошок/жидкость)
✓ Анализ совокупной стоимости владения (TCO) за 10 лет
✓ Готовый шаблон запроса предложений (RFQ) для закупок
Куда отправить PDF?
100% бесплатно. Без спама. Мгновенная загрузка PDF (4.9 МБ).

 English
 Русский