
Granule Bagging Line for Bulk Products: QZK-1200 Setup for Cleaner Bag Handoff and Pallet Flow
For granules, bulk products, and woven sacks, this layout keeps feeding, bag handoff, discharge, and pallet movement steadier. It is the kind of bagging line buyers ask for when they want fewer floor corrections and a cleaner dispatch rhythm.
When granules move faster than the old packing rhythm
In a busy bulk-products workshop, the pain is rarely the bag itself. The problem starts upstream: feed is uneven, the weighing point gets interrupted, and the sack leaves the station with a twist that slows the next operator. That is why a granule bagging line has to solve the full route, not only the dosing step. If the line cannot keep the bag mouth stable, the warehouse will keep paying for manual correction, short pauses, and messy pallet build-up.
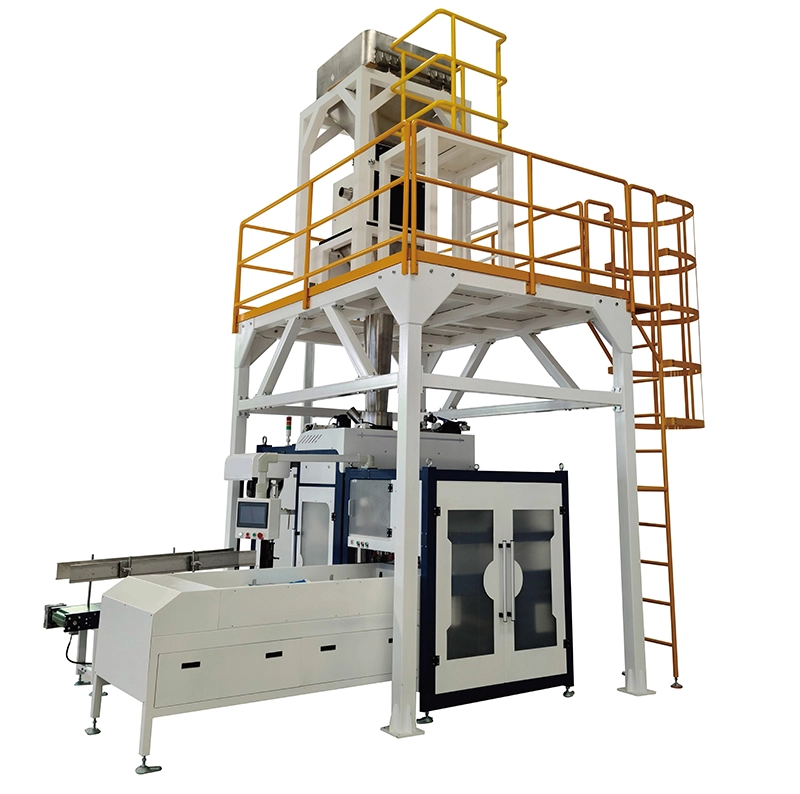
This is where the QZK-1200-style arrangement makes sense. The elevated structure, conveyor routing, and controlled bagging station are built for continuous bag transfer in a woven sack warehouse. In practical terms, it supports better bulk product packing: the bag arrives, opens, fills, exits, and reaches the pallet path without the operator having to fight the machine at every cycle.
Operators want a line that keeps granule feeding steady, protects the bag mouth during transfer, and avoids outfeed congestion when pallets start stacking up. Without that, the workshop gets more handwork, more bag rechecks, and a slower dispatch rhythm.
Why the line architecture fits the job
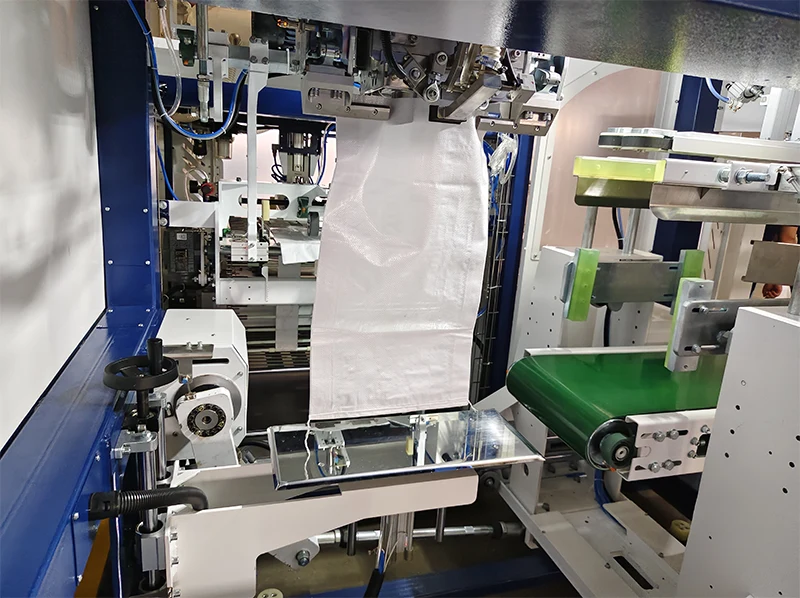
The machine evidence is visible in the hardware: a swing-arm HMI for controlled operation, a platform that keeps the work zone accessible, and an outfeed conveyor that reduces bag-to-pallet friction. The close-up of the bagging unit shows vacuum suction cups, a robotic placing arm, and a green conveyor working together. That combination matters because granule products are unforgiving: if the bag is not held correctly, the sack edge shifts, the fill point misaligns, and the next process slows down.
Compared with a loose, manual flow, this structure gives the workshop a more predictable result. It is easier to keep the bag mouth aligned, easier to supervise the transfer point, and easier to maintain a stable sequence from hopper to discharge. For searchers comparing a bagging line for bulk products or a secondary bagging layout in woven sacks, the value is not only speed. It is a steadier line that stays readable for the operator.
Operational note: when the line is built around controlled bag picking, guided outfeed, and clear access around the frame, the warehouse gets fewer stoppages and less product handling drift. That is the real reason the result feels calmer at the pallet end.
What the evidence says on the floor
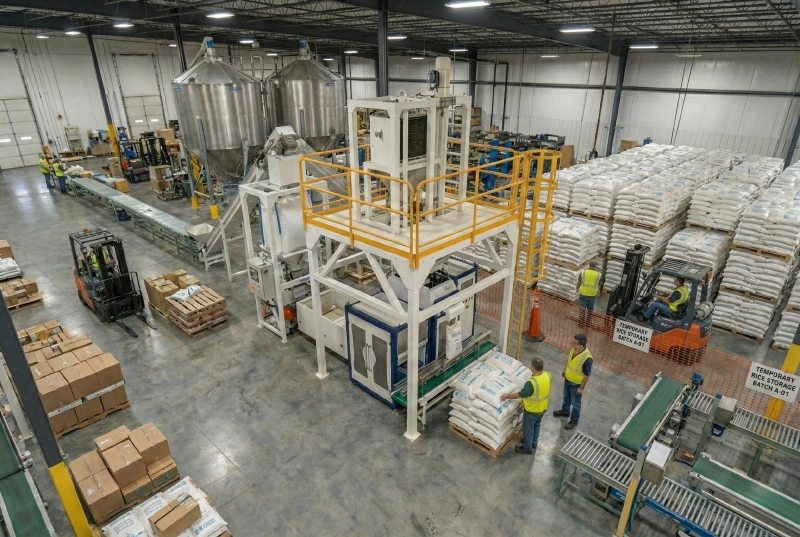
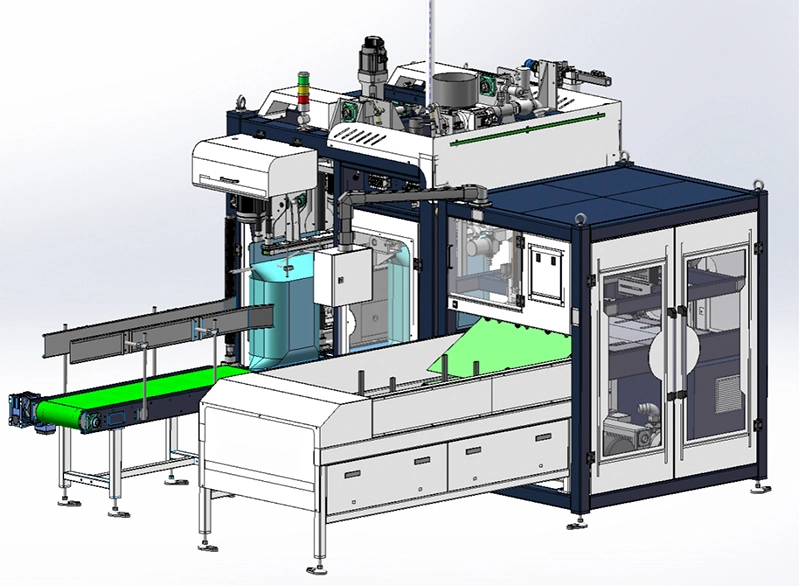
The strongest proof is in how the line ties feeding, bag handling, and discharge together. The high-angle plant photo shows twin stainless steel storage silos, conveyors, and active forklifts, which means the packaging line is not isolated from warehouse logistics. The secondary bagging layout image adds another layer: accumulation belt, large bag gripper, and discharge conveyor. Together they explain why the line fits a bulk-products site that needs flow continuity instead of stop-start packing.
In other words, this is not just equipment for sale. It is a working layout for a granule bagging line in a woven sack warehouse where the goal is steadier dispatch, fewer manual fixes, and a cleaner path from packing to pallet movement. If the buyer is trying to compare equipment for granule packing, the practical question is simple: can the line keep the bag stable while the rest of the operation keeps moving? This setup is designed to answer yes.
| Floor problem | What the line changes | Evidence in the images |
|---|---|---|
| Uneven feed and slow recovery after each cycle | Controlled hopper-to-bag sequence keeps the packing rhythm steadier | High-angle plant view with silos, conveyors, and active forklift flow |
| Bag mouth twist and unstable handoff | Vacuum suction cups and placing arm help guide the sack more cleanly | Internal close-up with suction cups, robotic placing arm, and green conveyor |
| Outfeed congestion near pallet build-up | Discharge conveyor separates the bagging point from pallet handling | Secondary bagging line render with accumulation belt and discharge conveyor |
| Operator fatigue during inspection and correction | HMI control and platform access make supervision simpler | Isometric machine view with swing-arm HMI touchscreen and platform |
Need a steadier granule packing layout?
If your line has to handle bulk products in woven sacks without constant hand correction, the QZK-1200-style bagging layout is a practical starting point. It combines controlled bag transfer, readable operator access, and a clearer discharge path so the warehouse can keep moving.
Talk to BPM about the right bagging line English
 Русский