
Mipline Powder Bagging Line for Stable 25 kg Bag Transfer Before Sewing
For dairy powder, flour, starch, feed, and other dry-powder plants, the difficult point is often not filling alone. It is the controlled handoff from a filled 25 kg bag to closure, sewing, inspection, and discharge. Mipline combines bag handling, bottom-up filling, closure, shaping, and guided conveying so the bag reaches the next station with less manual straightening.
Why the last meter becomes a production problem
A milk powder or flour plant may already have a filler and a sewing head, yet operators still need to open, hold, rotate, or square each heavy bag between them. A bag that twists on the conveyor can arrive with a skewed mouth. Powder on the closure area can make sewing or sealing less stable, while trapped air can leave the finished bag soft and uneven before palletizing. These are practical line-interface problems, not simply labor issues.
The old arrangement—manual bag placement followed by an ordinary transfer conveyor—does not control enough of the sequence. It moves the bag, but does not consistently manage bag opening, clamping, fill position, settling, shaping, and the handoff before sewing. The result is variable bag presentation and a final-meter correction task that is difficult to standardize across shifts.
If the filled bag mouth is skewed, dusty, or unstable, a faster filler can move the problem downstream. The line should make bag alignment and closure preparation part of the machine sequence.
How Mipline connects filling, closure, and bag handling
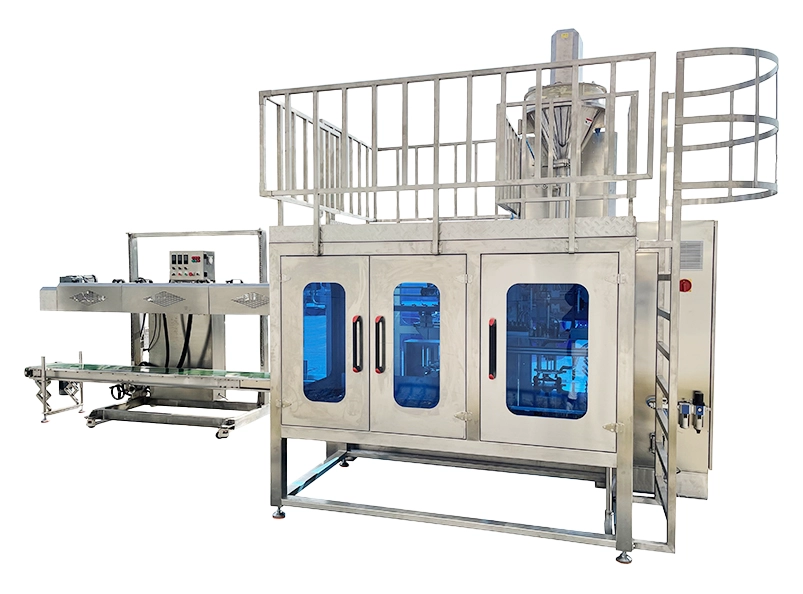
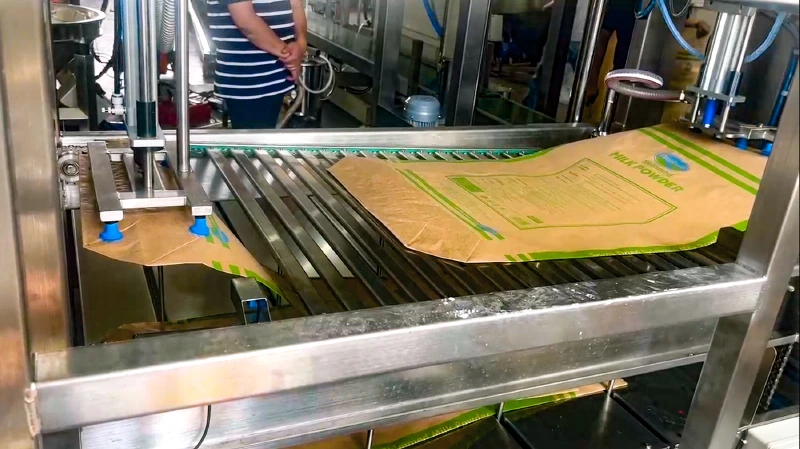
Mipline is configured as an automatic powder packaging line for industrial bags, typically 25 kg kraft paper, paper-plastic composite, or coated woven bags. A bag magazine and vacuum pickup supply the empty bag; opening and clamping hold it at the filling head. Bottom-up filling uses a lifting platform that follows the fill level, while three-stage screw feeding—fast, medium, and slow final dosing—supports controlled weighing instead of an uncontrolled free-fall stream at the bag mouth.
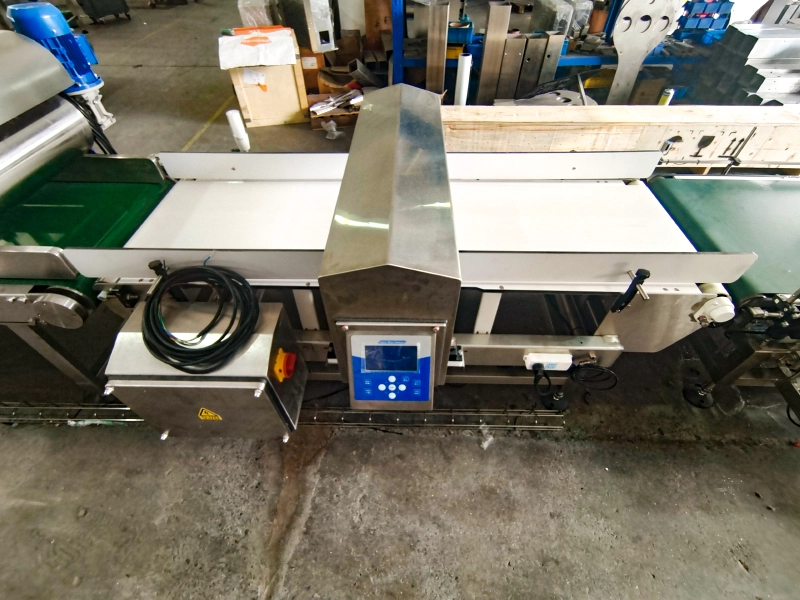
After filling, the selected configuration can add vacuum extraction or de-aeration, dust removal, trimming, inner heat sealing, sewing, paper-tape wrapping, pressing, settling, shaping, metal detection, checkweighing, reject, and roller discharge. This sequence is why the equipment fits a powder filling and bag sewing line: it treats the filled bag as a product that must be stabilized and inspected before dispatch.
Engineering view: The useful performance question is whether the bag remains square and controllable at each interface. Confirm powder bulk density, flowability, aeration, moisture, bag construction, target weight, closure method, line speed, and palletizing layout before freezing the configuration.
Visible structures that support a cleaner transfer
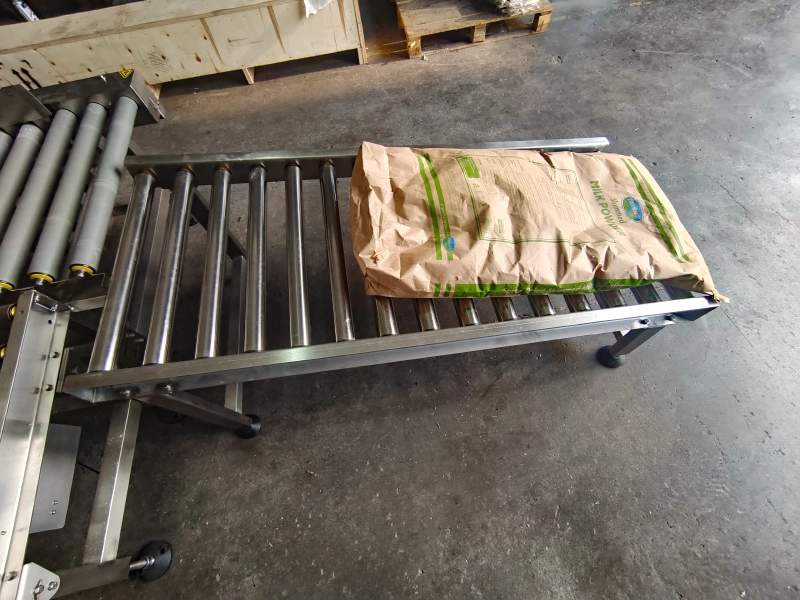
The factory images show the physical logic behind the line. The enclosed stainless-steel bagging station uses blue inspection windows and a top access platform, making the guarded bagging area and maintenance approach visible. Downstream, a twin-belt transfer conveyor with adjustable side guides provides a more deliberate path than a flat, unguided belt. A roller section with a kraft paper bag shows the type of bag transfer and support needed before closure or sewing.
For a 25 kg powder bagging line, these details matter because alignment is created mechanically: the clamp controls the bag during filling, the conveyor guides the bag after filling, and settling or shaping can be placed before final inspection. The final setup may also include a metal detector and checkweigher. Checkweigher values vary by selected model and product effect, so the approved project datasheet—not a universal marketing number—must define accuracy and throughput.
| Project point | Mipline reference or configuration logic |
|---|---|
| Bag and target weight | Industrial powder bags, commonly 25 kg; DS25K reference covers 5–25 kg. |
| Filling method | Vertical screw feeding with fast, medium, and slow dosing plus bottom-up tracked filling. |
| Reference capacity | Variant-dependent references include 1–2 bags/min and 1–3 bags/min; confirm the selected material and layout. |
| Bag transfer | Guided belt and roller sections support alignment, settling, shaping, and handoff before sewing. |
| Inspection | Optional metal detection, checkweighing, reject, and final roller discharge after forming and closure. |
Specify the bag handoff before you specify the machine
Tell BPM your powder, bag material and dimensions, target weight, closure method, required speed, available utilities, and downstream palletizing plan. We can then match the automatic powder packing machine, sealing steps, conveyors, inspection, and reject path to the real process.
Discuss Your Powder Packaging Line English
 Русский