
10 kg Bagging Line: Steady Woven Sack Output
A 10 kg woven sack is not a true workstation. Most plants still run a 10 kg bagging line with manual sack presentation, a stand-alone scale, separate sealing, and free-standing outfeed, then patch the rhythm with forklift movement. A purpose-built 10 kg bagging line ties feeding, weighing, bag transfer, sealing, and pallet-ready outfeed into one continuous flow so the workshop stops reacting to every single bag.
Why a 10 kg bagging line breaks rhythm under handheld stations
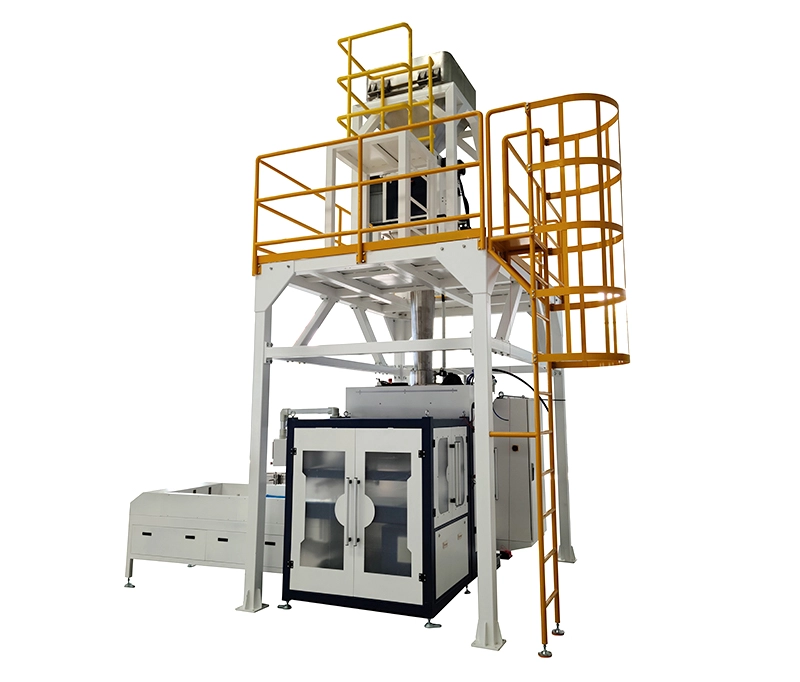
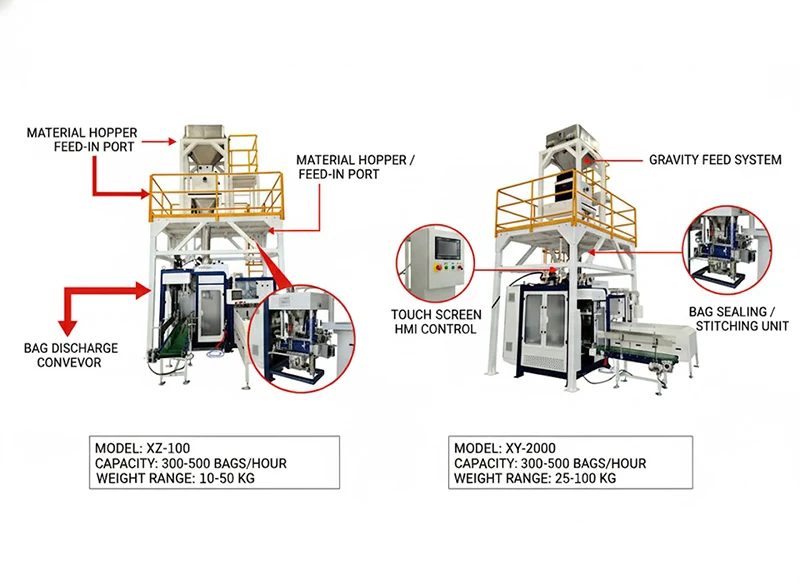
The first image shows the spec panel most buyers compare when they shortlist a 10 kg bagging line. XZ-100 is rated 300-500 bags/hour on a 10-50 kg bag range with hopper feed, gravity dosing, HMI touchscreen, and an inline sewing unit. On paper, the figures look fine. On the floor, the same numbers tell a different story when every station is operated by a different worker and the bag has to be carried between them.
A 10 kg bagging line under manual stations usually loses time at three points: sack presentation at the filling point, scale hand-off between weighing and clamping, and the gap between the sealer and the outfeed conveyor. Each gap is short, and each one is enough to break the cycle. Add a forklift waiting for a pallet at the end, and the line stops waiting with it. That is why most 10 kg bagging line projects end up running at 60-70% of the rated capacity on day one.
Manual sack opening, stand-alone weighing, free-fall clamping, separate heat seal, and an outfeed that has to be caught by the next operator. Three hand-offs per cycle, every cycle, and the line only runs as fast as the slowest hand-off.
Why the QZK-1200 layout fits a 10 kg woven sack
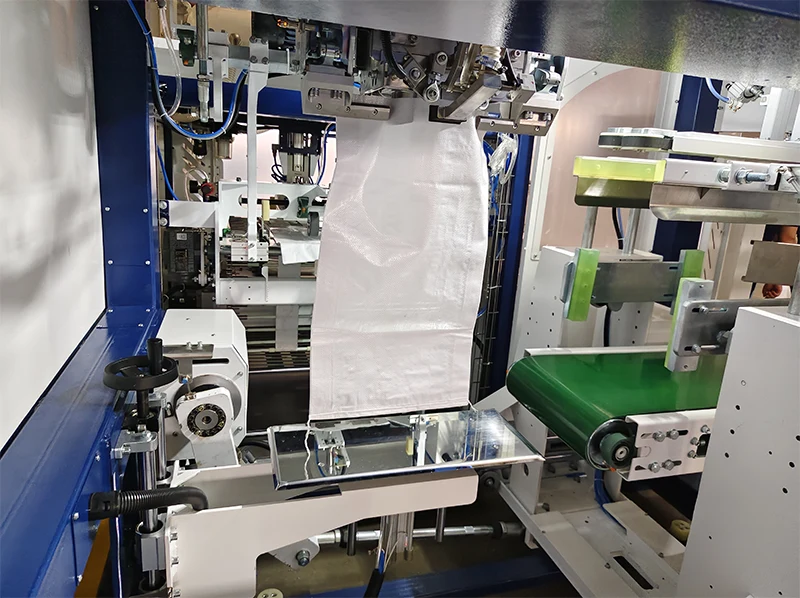
The close-up shows what the QZK-1200 does at the bag pickup station. Vacuum suction cups grip the woven PP sack, a robotic placing arm moves it onto the filling spout, and the green belt takes the bag into the pneumatic clamp. There is no operator step between pickup and clamp on this station. For a 10 kg bagging line, that alone removes one of the three hand-offs that manual stations create, and it removes the slow closing step that operators tend to skip when the line is behind.
The structural choice is just as important. The hopper is mounted directly above the dosing unit, so the 10 kg sack is filled from below by gravity rather than dropped from a free-fall chute. The HMI is mounted on a swing arm so the operator can see the recipe and the cycle counter without leaning over the bag. The enclosure keeps dust out of the bag mouth and keeps the sealer running at the same set temperature, which is what keeps a 10 kg bagging line accurate from the first bag to the 500th.
Engineering note: For a 10 kg woven sack line, the bottleneck is rarely the bagger itself. It is the gap between weighing and the next clamp, and the gap between the sealer and the outfeed. A 10 kg bagging line that closes both gaps inside one structural frame usually beats a faster standalone unit that leaves both gaps open, because those gaps are where operators compensate and where giveaway drifts.
Evidence from structure and operating scene
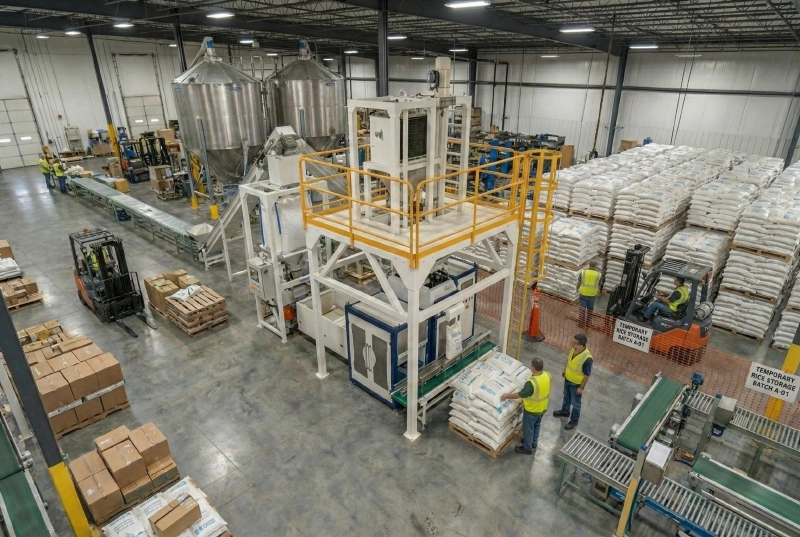
The operating scene shows the line working in a real plant, not as a showroom mockup. Twin stainless steel silos feed the line through inclined conveyors, the bagging tower drops 10 kg woven sacks onto the green outfeed belt, and a forklift clears the pallet stacks behind the line. That is the layout a 10 kg bagging line is meant to fit: silos at one end, dispatch at the other, and the bagging tower in between.
The structure tells the same story. The bagging tower is a single welded steel frame with a top platform, a safety cage ladder, a swing-arm HMI, and an enclosed filling cabinet. The weigh frame sits under the silo, the dosing unit sits under the weigh frame, and the outfeed belt sits on the same base. For a 10 kg woven sack project, this is the difference between a line that has to be re-engineered on site and a line that drops onto the floor plan.
| Module | What it does | Why it matters for a 10 kg bagging line |
|---|---|---|
| Bag magazine + vacuum placer | Pre-stages 10 kg woven PP bags and feeds them to the filling spout | Removes manual bag presentation and aligns the bag mouth at the fill point |
| Weigh frame + dosing unit | Hits plus or minus 0.2% target weight on 10 kg sacks | Keeps giveaway inside a tight band so a 10 kg bagging line does not over-fill and over-pay for material |
| Heat seal + sewing head | Closes the 10 kg sack with heat seal, sewing, or heat-seal-plus-sewing | Matches the bag spec without forcing the buyer to choose one closure before the bag type is locked |
| Outfeed belt + checkweigher | Carries the 10 kg sack to inspection, rejection, and pallet-ready outfeed | Stops the line waiting on a forklift and gives the line a clean handoff to palletizing |
| PLC + HMI + load cell stack | Inovance for standard 10 kg lines, Siemens for higher-speed or higher-demand projects | Matches the control option of the original project brief without forcing a re-spec |
Request a 10 kg bagging line proposal
Send your bag size, target output, material bulk density, and floor layout. BPMpack will return a QZK-1200 based 10 kg bagging line proposal with CAD layout, dosing spec, and PLC option so engineering can sign off before fabrication starts.
Talk to engineering English
 Русский