
Mipline Powder Packaging Line: Controlling the Bag Handoff Before Sewing
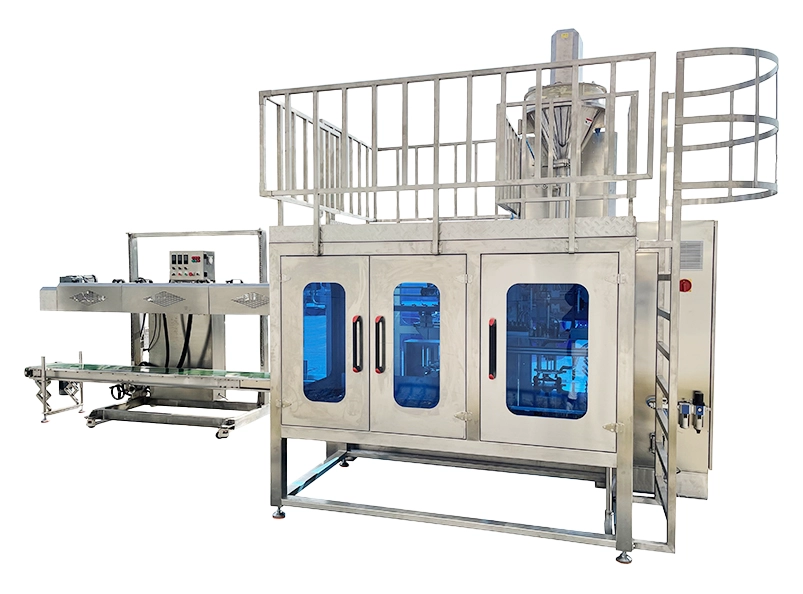
For dairy powder, flour, starch, feed, and other dry powders packed in 25 kg industrial bags, the final transfer before sewing or sealing often determines whether the line runs cleanly. Mipline links bag supply, bottom-up filling, closure, shaping, inspection, and discharge so bags reach the next station square, supported, and easier to control.
Why the last meter becomes a powder bagging problem
A plant may already have a filler and a sewing head, yet still lose time between them. A filled bag can twist as it leaves the clamp, retain air, or arrive with a dusty and skewed mouth. Operators then stop the flow to open, straighten, or reposition the bag by hand. That correction is slow, difficult to standardize, and especially uncomfortable when the line handles heavy milk powder, flour, starch, or feed bags.
The issue is not simply conveyor speed. A bag needs a controlled handoff: its base must settle, its sides must remain guided, and its mouth must present consistently to the closure station. A powder packaging line that treats filling and transfer as separate islands leaves the most sensitive part of the process to manual judgment.
Manual correction can hide the real failure point. It does not remove excess air, control powder at the bag mouth, or create a repeatable transfer reference. When bag shape changes from one cycle to the next, sewing and sealing quality becomes dependent on operator reaction.
How Mipline adapts the process to the bag, powder, and closure
Mipline is configured as an automatic bagging machine for powder rather than as a standalone filler. A bag magazine and pickup system supply the empty bag; opening, clamping, and controlled placement hold it at the filling head. The bottom-up lifting fill keeps the filling point close to the rising powder level, a design intended to reduce dust escape compared with open free-fall filling. Where the project requires it, vacuum extraction or de-aeration can be included before closure.
After filling, the line can combine dust removal, trimming, inner heat sealing, sewing, paper-tape wrapping, pressing, settling, shaping, metal detection, checkweighing, reject, and roller discharge. This sequence gives the filled bag a defined path instead of asking an operator to create alignment between independent machines. The final configuration must still be matched to bulk density, flowability, moisture, aeration, bag construction, target speed, and site layout.
Engineering view: stable bag transfer before sewing is created by the relationship between clamp alignment, guided conveyors, roller support, and closure timing—not by a single belt alone.
Structures and reference parameters to verify
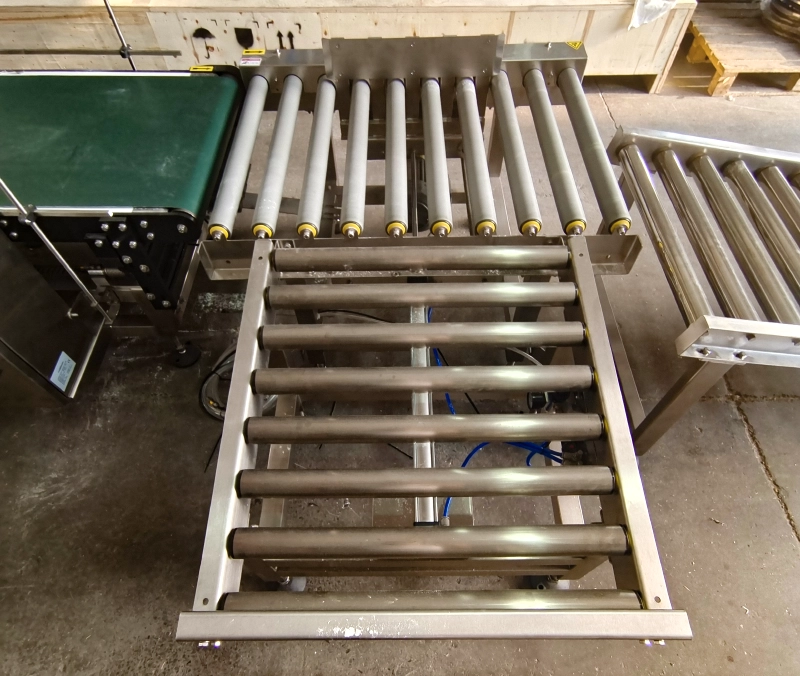
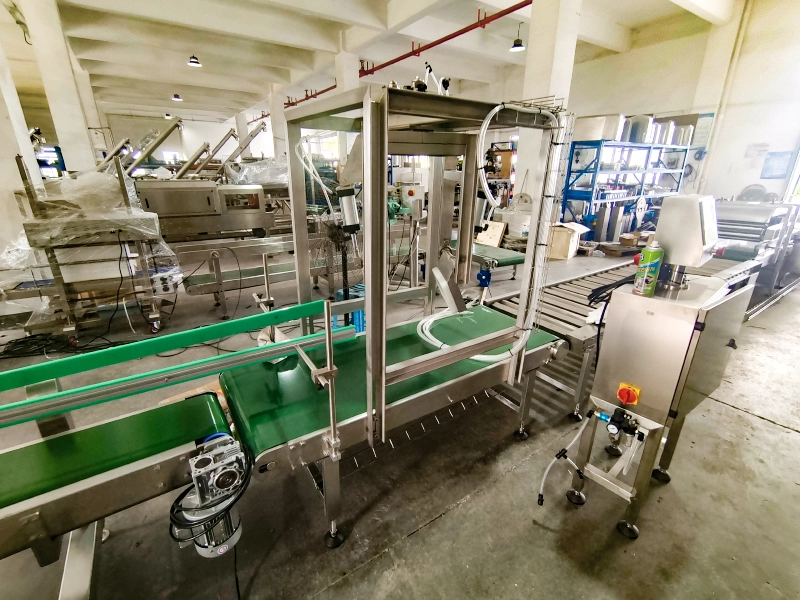
The production images show the physical evidence behind the layout: enclosed stainless-steel stations, blue inspection windows, bag magazine conveying, green belts, roller transfers, adjustable guides, emergency-stop controls, and maintenance access. The following reference points help an engineering team connect the powder application to the right configuration.
| Line requirement | Mipline reference or adaptation | Why it matters before sewing |
|---|---|---|
| 25 kg industrial bags | Nominal 25 kg application; 5–25 kg reference variant available | Defines bag dimensions, clamp range, fill sequence, and downstream handling |
| Controlled filling | Vertical screw feed with fast, medium, and slow dosing stages | Supports weight control and reduces the chance of a dusty, unstable bag mouth |
| Bag transfer | Guided belt and roller sections with adjustable support | Helps keep the bag square and reduces manual bag straightening |
| Closure and quality | Project-configured sewing or sealing, with optional metal detection and checkweighing | Creates a defined reject and inspection path before palletizing or dispatch |
| Utilities and hygiene | SUS304 body reference; one configuration lists 5 kW main power and 5.5 m³/h air | Provides a starting point for site review, subject to the approved configuration |
For a milk powder packaging machine or flour bagging line, the final proposal should confirm the powder test, bag material, target capacity, power, compressed air, dust extraction, closure method, and palletizing interface. Published reference values are variant-dependent: one line list states 1.5–2 bags/min with accuracy of ≤±0.1–0.2%, while another 5–25 kg reference states 1–3 bags/min and ≤±0.2%. These figures should not be treated as a universal promise.
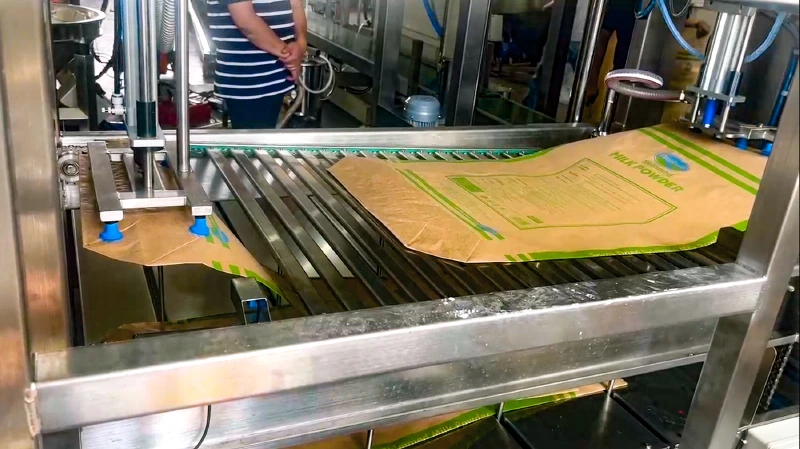
At the discharge end, stable settling and shaping give inspection equipment a more consistent product presentation. A checkweigher can then identify weight deviation, while a powder-line metal detector and defined reject path protect the dispatch process. The image evidence shows the bag transfer and handling hardware; exact detector effect and checkweigher accuracy require confirmation against the selected powder and project datasheets.
Specify the complete powder bagging line, not only the filler
Share the powder type, bulk density, bag construction, target weight, required bags per minute, closure method, utilities, and palletizing layout. BPM can use those inputs to review the Mipline bag handoff, filling, closure, inspection, and discharge configuration for your plant.
Discuss Your Powder Line English
 Русский