
Cement Bagging Equipment: Closed Loop 25 kg Cell
Most cement bagging equipment on the dispatch floor still runs as separate stations: a manual bag spotter, an open-mouth filler, a sewing head, and a forklift doing the pallet math. A closed-loop 25 kg valve sack cell replaces that hand-off chain with one continuous flow from bag magazine to wrapped pallet. The plant gets tighter dust control, steadier cycle time, and a real audit trail at the seam between production and logistics.
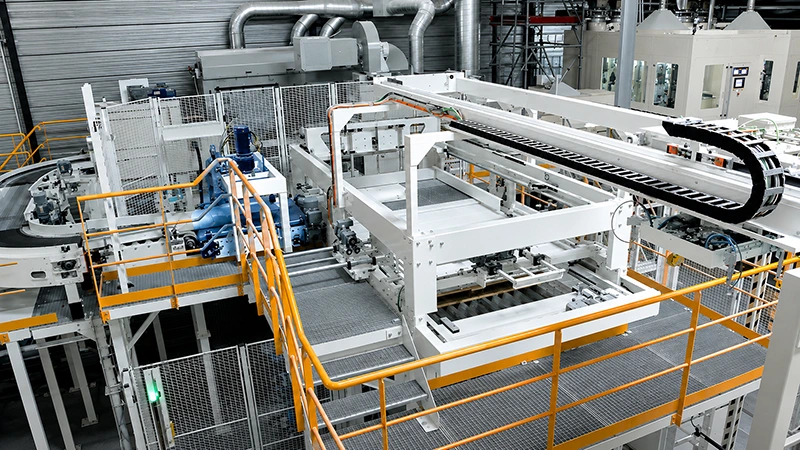
From Bag Magazine to Pallet Wrap in One Continuous Cell
A modern 25 kg cement bagging equipment cell starts at the wheeled bag magazine, where empty valve sacks are stacked, aligned, and lifted by a twin-arm pick-and-place head. Suction cups grip the top ply, open the valve, and sleeve it over the inflatable filling nozzle without an operator standing underneath. The cell wall keeps the dust inside the boot, not in the operator’s breathing zone.
Downstream, the same cement bagging equipment carries the bag through air-assisted filling, ultrasonic valve sealing, an inline checkweigher, and a metal-detection gate before negative-pressure shaping flattens the sack for stable pallet geometry. By the time the robotic pallet head places the bag on the layer, the cell has already weighed, sealed, shaped, and confirmed the unit — without a single bag leaving the steel frame. The result is a closed loop that survives a 12-hour shift without a manual hand-off, and that is the difference between a cement bagging equipment investment and a list of separate machines.
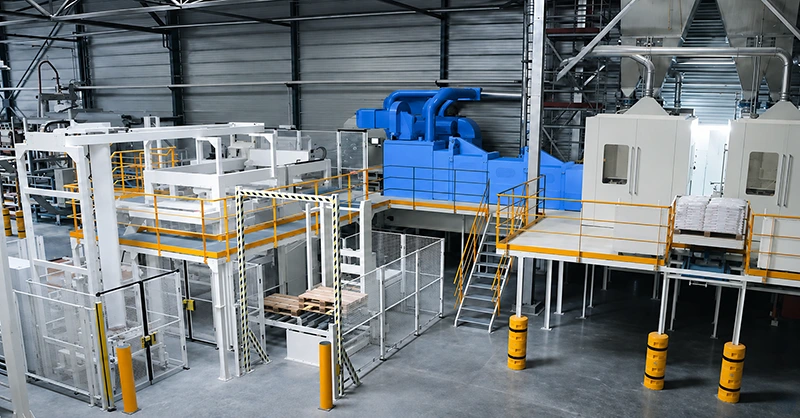
Every manual bag spot, every open-mouth fill, and every forklift trip is a line item your EHS manager cannot audit. In a 25 kg cement dispatch hall, those line items compound across three shifts.
What the Cement Floor Actually Pays For
The first pain is dust. An open-mouth screw or impeller fill on a 25 kg cement bag lets fines escape at the bag-machine interface; even with a hood, the operator’s gloves, sleeves, and the floor still carry the load. A closed-loop cement bagging equipment cell holds the bag mouth inside the boot through pick-and-place, air-assisted filling, and ultrasonic sealing, so the bag never opens to the room air. That cuts both visible plume and the long-term maintenance load on the bag-side dust collection duct.
The second pain is unstable pallet geometry. Air pockets left in the bag after filling turn into leaners, which turn into re-stacks, which turn into a load that arrives at the customer with a torn outer ply. Negative-pressure shaping on the same cement bagging equipment cell evacuates the headspace before the bag reaches the layer, and the layer pattern — typically three bags per layer with controlled rotation — keeps the stack square on the EPAL pallet. Cold-drawn stretch hood then locks the load against weather and shift handling.
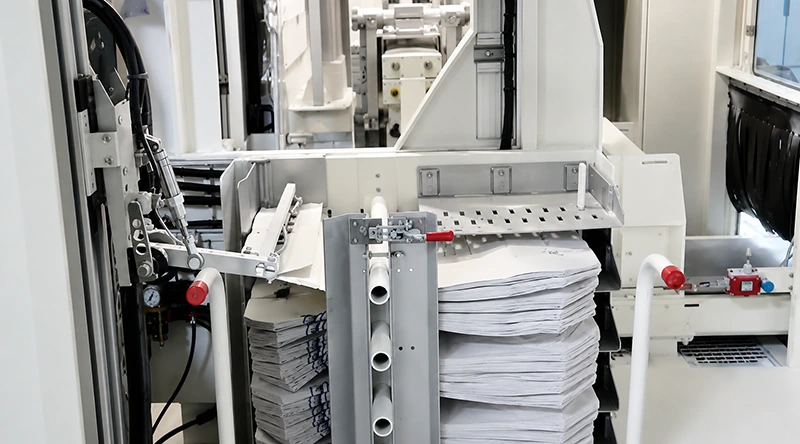
Engineering note: Bag tolerance, valve-flute geometry, and the cement’s bulk density are not optional details. A bag that is even 2 mm too tight on the valve will not seat on the inflatable nozzle, and ultrasonic sealing will not bond through a clay-heavy surface film. The same cement bagging equipment that runs at the higher end of its 5–12 bags/min band on a dry-mix plant will not run the same number on a fine cement with high LOI without a confirmed bag sample and a sealed-window test on the actual laminate.
Station-Level Specs for a 25 kg Cement Bagging Equipment Cell
Buyers who compare cement bagging equipment by station count rather than by interface usually end up with mismatched cycle times. The table below lists the stations a continuous 25 kg cell typically ties together and the interface each station carries into the next.
Values reflect the current BPMpack VPLINE valve sack cell reference and must be confirmed against the project’s bag sample, bulk density, plant air pressure, and dispatch throughput target. Throughput and accuracy depend on the cement grade and the dust-handling interface.
| Station | Function | Interface / Spec |
|---|---|---|
| Bag magazine | Empty valve sack stack, mobile frame with casters | ~200–300 bags per refill, stainless guide rails |
| Pick-and-place head | Suction cup bag pickup, valve opening, sleeve over nozzle | Twin-arm pneumatic, 0.5–0.7 MPa plant air |
| Inflatable filling nozzle | Closed-boot air-assisted cement fill | Inflatable seal, 304 SS product contact |
| Ultrasonic valve sealer | 20–40 kHz bond on valve flap | Sealed window depends on bag laminate |
| Inline checkweigher | Net-weight confirmation, auto-reject | ±1–2‰ of target weight (project-confirmed) |
| Metal-detection gate | Ferrous / non-ferrous / stainless reject | Mounted on the same conveyor as the checkweigher |
| Negative-pressure shaper | Evacuates headspace, flattens bag face | Vacuum head matched to bag face size |
| Robotic pallet head | Layer placement, controlled bag rotation | Typically three bags per layer |
| Stretch hood / wrap | Final pallet weather protection | Cold-drawn PE hood, full pallet coverage |
Ready to Map a 25 kg Cement Bagging Equipment Cell?
Send your bag sample, plant layout, and dispatch target. We will return a closed-loop proposal with confirmed cycle time, dust-handling interface, and pallet geometry for your specific cement grade.
Request a Project Review English
 Русский