
A Cleaner Woven-Sack Handoff Path for a Southern Grain Warehouse
ppline in a southern grain warehouse
A Cleaner Woven-Sack Handoff Path for a Southern Grain Warehouse
When woven sacks leave filling and move toward sewing, the weak point is not the filler. It is the handoff. A small twist, a loose mouth, or a drifting bag edge can slow the line, pull operators back into manual correction, and create a messy sewing station.
This project used the ppline bagging station to keep the sack square, keep the transfer steadier, and feed the next sewing step with less rework.
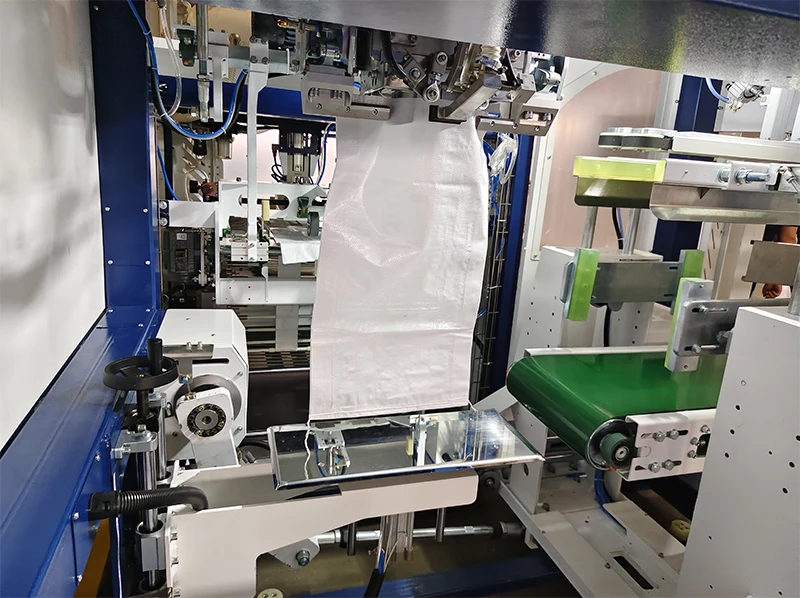
The problem was never just filling
In this warehouse, the old setup did a reasonable job of moving product into the sack, but the bag arrived at sewing in an inconsistent position. Operators had to re-square the mouth by hand. That meant more touches, more waiting, and more variation from one sack to the next.
The real pain showed up in three places:
- Bag mouth drift: the woven sack could lean or wrinkle before the sewing head.
- Manual correction: staff had to steady each sack before it was safe to stitch.
- Downstream mismatch: when transfer is unstable, sewing speed drops to the speed of human correction.
Why ppline fit this job
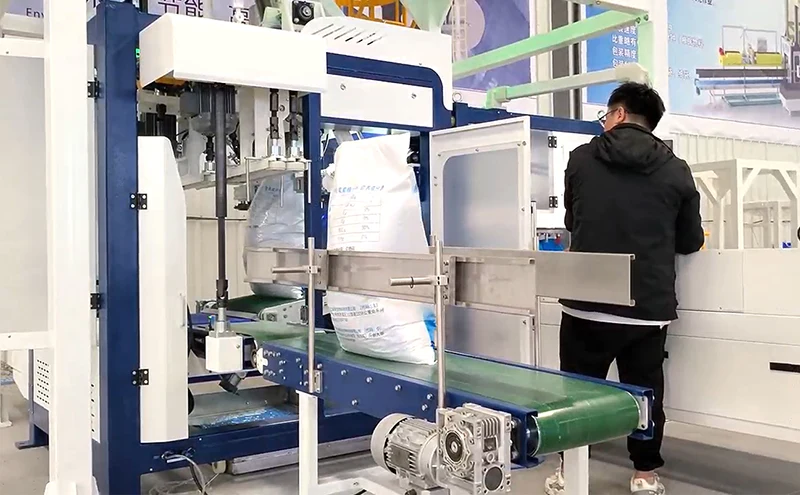
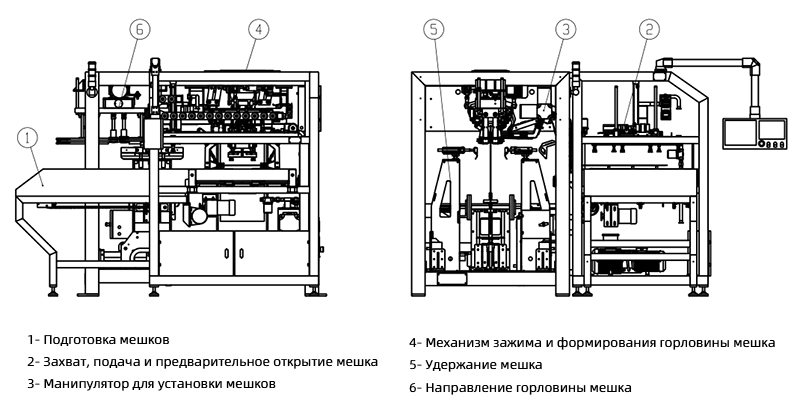
The ppline system matched the warehouse because it solves the handoff as a mechanical alignment problem, not a labor problem. The close-up bagging module uses vacuum suction cups, a robotic bag placer, and a controlled green conveyor to hold the woven sack in a repeatable position. Instead of relying on a worker to square the mouth after every transfer, the machine keeps the bag seated and guided.
The line also uses structural details that matter in day-to-day operation: a steel frame for stability, guide rails to reduce side movement, a bag clamp area to hold the mouth, and a bottom support assembly with pneumatic cylinders and servo adjustment to keep the bag aligned during the transition. Those details are visible in the image set, and they are the reason the line performs better than a loose conveyor handoff.
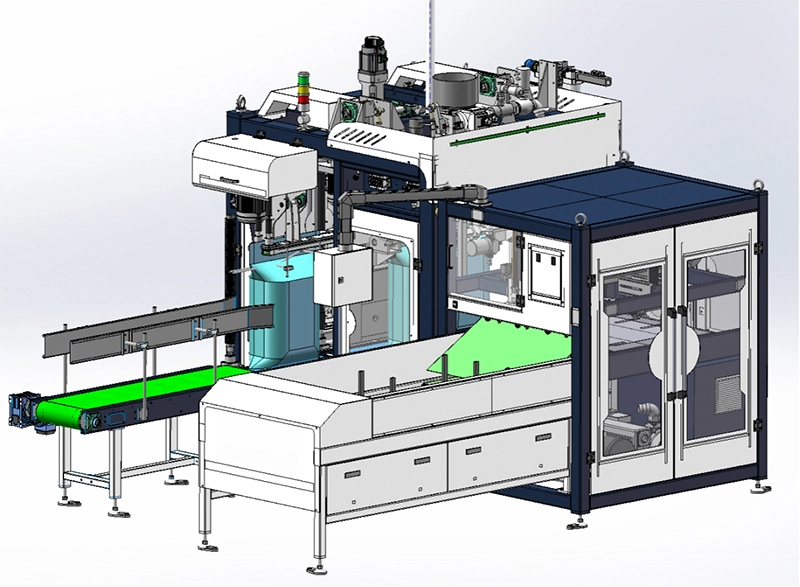
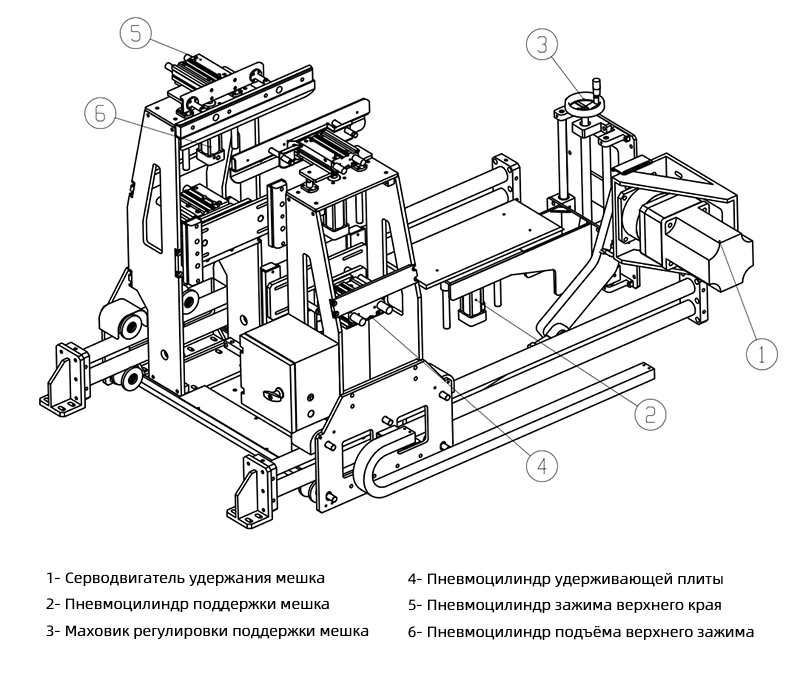
That is why the warehouse saw a practical improvement. The sewing station no longer had to absorb all the variation coming from upstream. The bag arrived straighter, the mouth was easier to catch, and the line felt less dependent on operator reflexes.
Что изменилось после модернизации
| Old situation | What ppline changed | Подтверждение по фотографиям |
|---|---|---|
| Bag mouth wandered before sewing | Vacuum placement and guided transfer held the sack in line | Close-up module with suction cups and green conveyor |
| Operators had to re-square every sack | Clamp, support, and servo positioning reduced manual correction | CAD detail of the clamping and bottom support assembly |
| Downstream sewing speed was limited by the handoff | Stable discharge made the sewing station easier to feed | System view of accumulation belt, gripper, and discharge conveyor |
The result: a steadier path to sewing
For a grain warehouse, the best packaging change is often the one that removes a small but constant delay. In this case, the ppline line did exactly that. It reduced the need for hand straightening, kept the woven sacks better controlled between filling and sewing, and made the whole transfer feel more predictable.
That matters because predictable handoff means cleaner flow, less operator fatigue, and fewer minor stoppages that never look dramatic on paper but always cost time on the floor.
If your line is losing time at the moment a woven sack leaves filling and reaches sewing, the fix is usually not more labor. It is better control of the handoff itself.
 English
 Русский