
ppline Packaging Line for Controlled Hopper Feed, Secure Bag Pickup, and Stable Dispatch
When the bagging area has to keep feed steady, avoid sloppy bag handling, and move filled sacks to pallets without creating transfer bottlenecks, the line needs more than a basic filler. This ppline layout combines hopper feed, elevated access, swing-arm HMI control, vacuum bag handling, and conveyor outfeed to keep the handoff cleaner from the first pickup to the last pallet.
Why the line fits a real bulk-material packing site
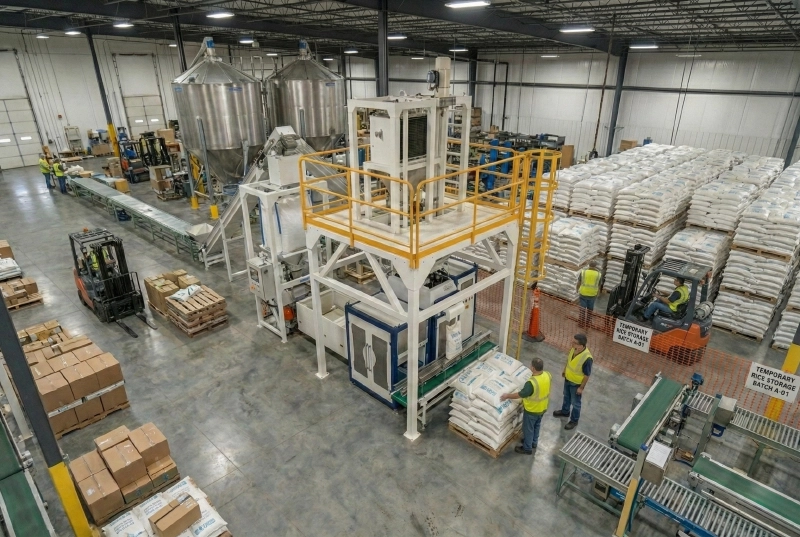
Bulk product packing rarely fails at one dramatic point. It usually slows down at small handoff gaps: the hopper feed is uneven, the operator access is awkward, bags do not settle cleanly, and the discharge side starts to back up. The first image shows a complete bagging line laid out around a hopper, an elevated working platform, and a downstream transfer path. That is exactly the kind of structure a plant needs when the goal is to keep the infeed stable and the output moving without constant manual correction.
The bagging station image makes the control side visible as well: a swing-arm HMI touchscreen, a steel platform, safety railing, and an outfeed conveyor. That combination matters because the operator can watch the process from one point, adjust the job without walking around the machine, and keep the bagging rhythm aligned with the rest of the line. For a packing operation, that is how you reduce small stoppages that turn into big hourly losses.
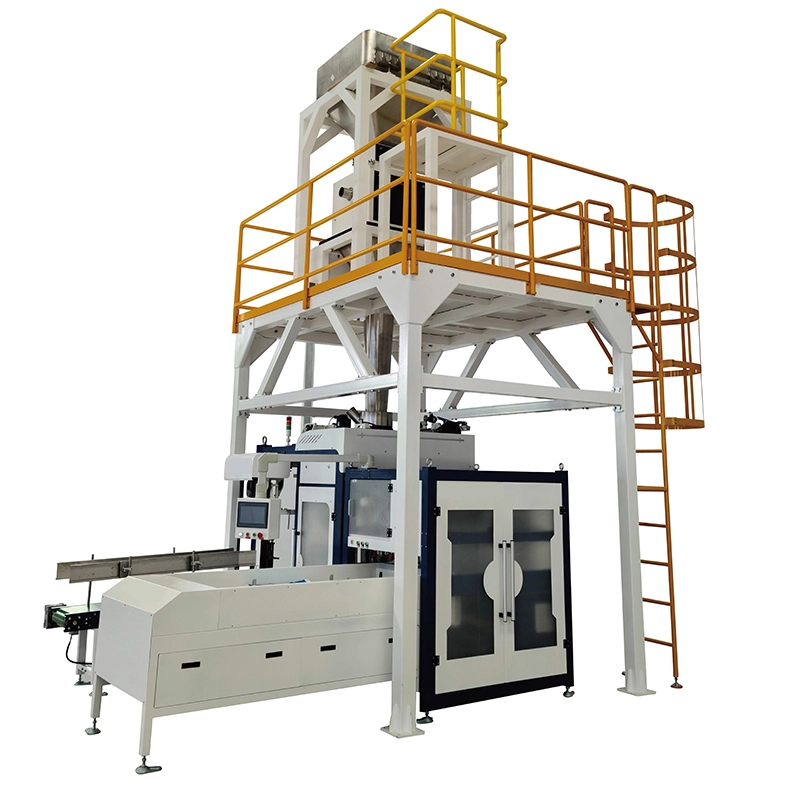
A packing line becomes unreliable when bag pickup is inconsistent, bag positioning is messy, and workers must compensate for the machine instead of the machine supporting the worker.
What the internal structure is doing for the operator
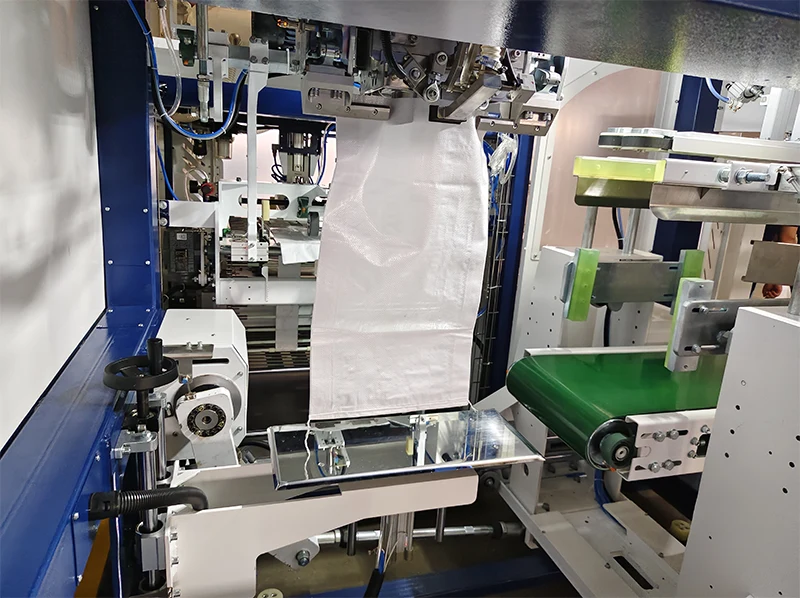
The close-up image shows the internal bagging unit with vacuum suction cups, a woven-bag handling zone, and a height adjustment handwheel. This is the part that explains why the line can keep the bag pickup cleaner. Vacuum pickup gives a more controlled handoff than a loose manual catch, while the height adjustment helps the unit match bag size and working height without forcing a rough setup.
That is the difference between a machine that simply fills and a machine that supports the whole packing rhythm. When the internal handling is controlled, the downstream conveyor does not have to absorb the mess. The pallet side runs steadier, and operators spend less time fixing placement issues or reworking a poorly presented sack. The result is a more predictable line from hopper to dispatch.
Operational insight: the best packing line layout is not only about throughput. It is also about reducing the number of times the bag must be touched, lifted, corrected, or re-aligned before it reaches the pallet.
What the running line proves in practice
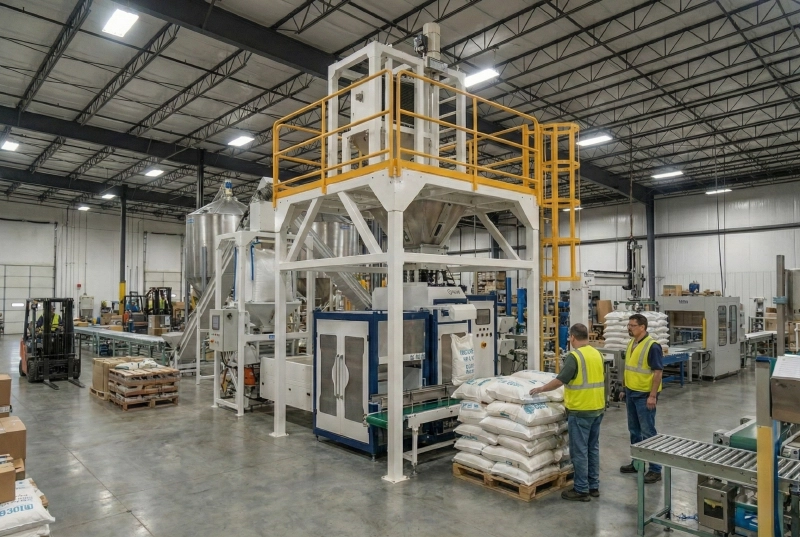
The production-floor image shows the machine working with operators around the pallet zone, which is the most practical proof point for any bagging installation. The line is not isolated in a lab. It is placed where people, conveyors, and pallets must cooperate. That is why the steel cage ladder, belt conveyor, and visible stacking area matter: they show the machine has been built for real access, real transfer, and real warehouse movement.
For a bulk-material packing site, that kind of structure supports three outcomes. First, the hopper feed stays more stable because the upstream section is organized. Second, the bag handoff is cleaner because the pickup and transfer path are controlled. Third, the dispatch side is easier to manage because the pallets are collected in a defined flow rather than scattered around the floor. If the target is fewer interruptions and a steadier daily output, this is the layout direction that makes sense.
| Evidence from the images | Operational meaning | Result for the packing site |
|---|---|---|
| Hopper feed and elevated platform | Better access and more organized infeed | Steadier material supply |
| Swing-arm HMI and outfeed conveyor | Easy control and cleaner bag transfer | Fewer interruptions during packing |
| Vacuum suction cups and height adjustment | Controlled bag pickup and easier setup | More reliable bag handling |
| Operators stacking sacks beside the conveyor | Defined pallet flow and practical line integration | Cleaner dispatch and steadier warehouse movement |
Need a steadier bagging layout?
If your current line is losing time at the hopper, at the bag pickup point, or at the pallet side, the ppline layout shows the kind of structure that can tighten the whole flow. Share the bag size, target output, and material type, and we can match the packing line to the real working condition instead of forcing a generic setup.
Talk to BPM English
 Русский