
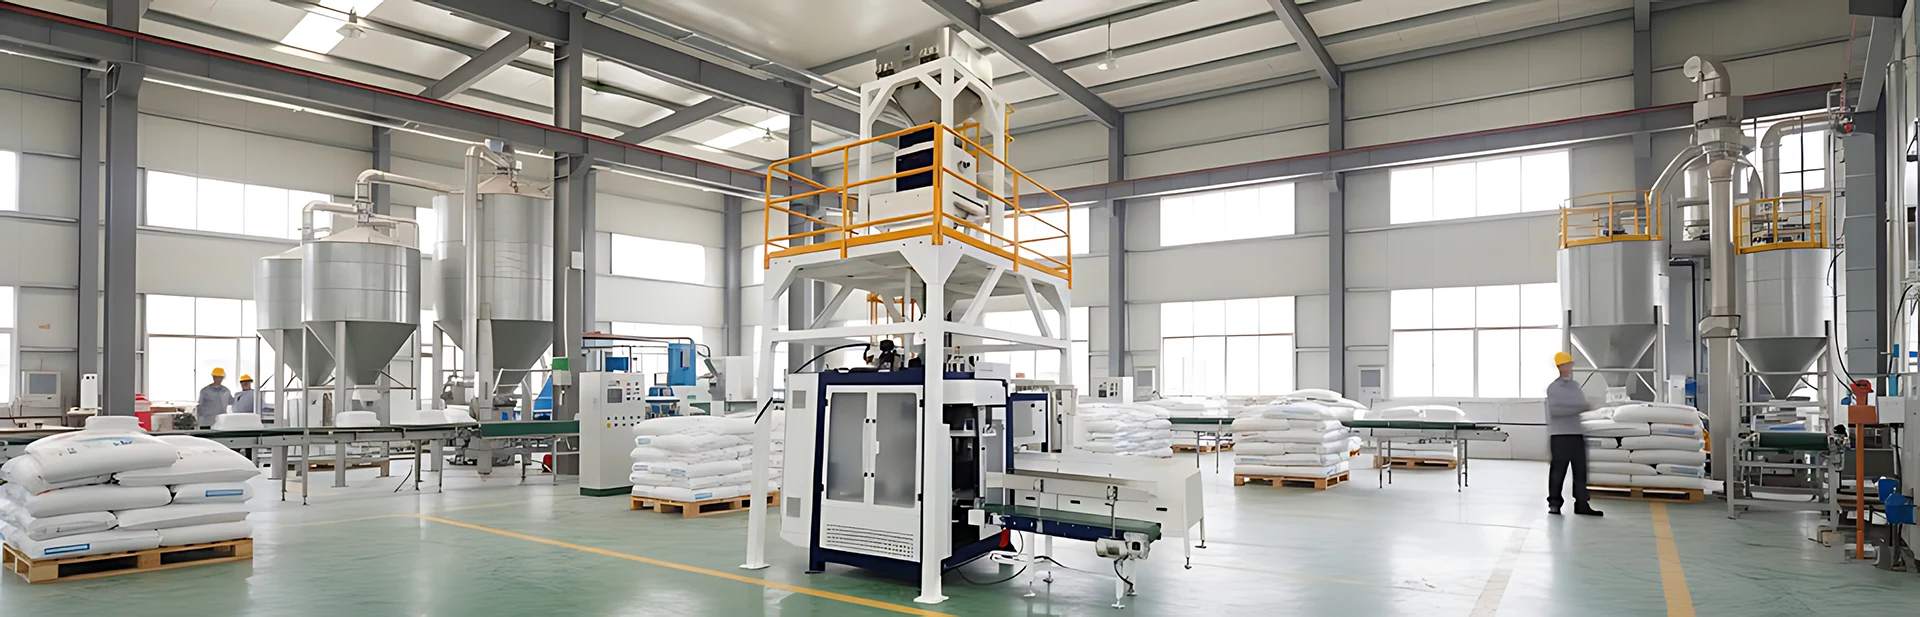
What the old method was doing wrong
In many lines for сыпучих продуктов, the first setup is still a mix of manual bag correction and loosely coordinated conveyor movement. Operators pull the bag back into position, the bag mouth twists, the seam drifts, and the line slows down while someone fixes the next problem by hand. That approach can work for a small batch, but it becomes expensive as soon as the plant wants steadier output.
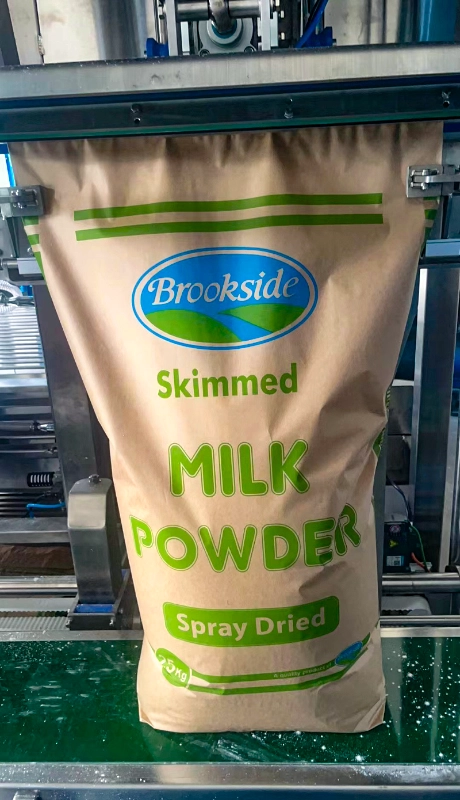
The customer scenario was familiar: a bulk-material line with a good upstream supply, but inconsistent bag posture at the sewing point. The plant did not need a completely new process idea. It needed a line that could keep the bag flat, aligned, and predictable while moving it from filling to sewing.
Why PPLINE fits this type of line
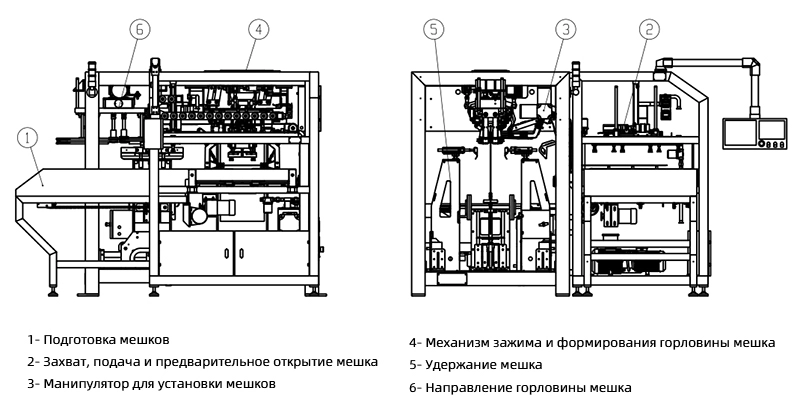
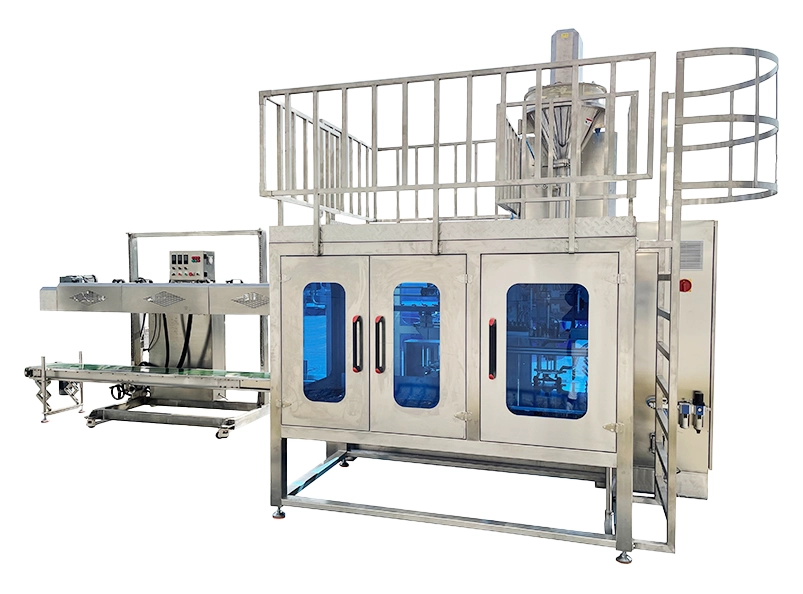
PPLINE is a better fit because it treats the handoff as a mechanical problem, not a human correction problem. The line combines a top hopper feed, an enclosed cabinet section, guided transfer, and a controlled conveyor path so the bag arrives at the next station with less distortion. That matters when the plant wants fewer manual touches and cleaner stitching.
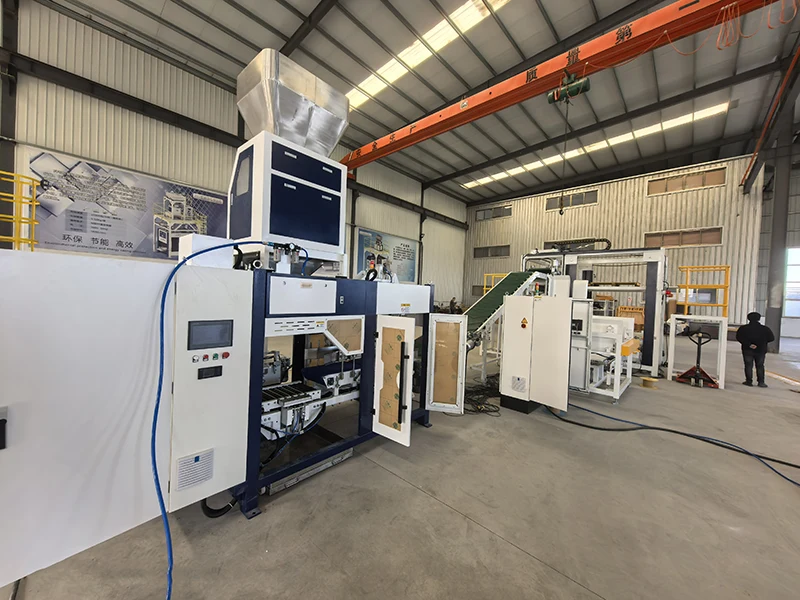
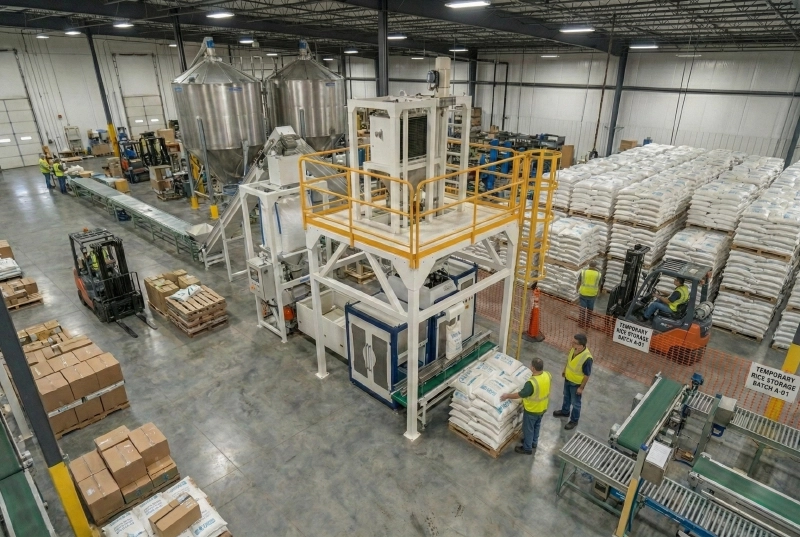
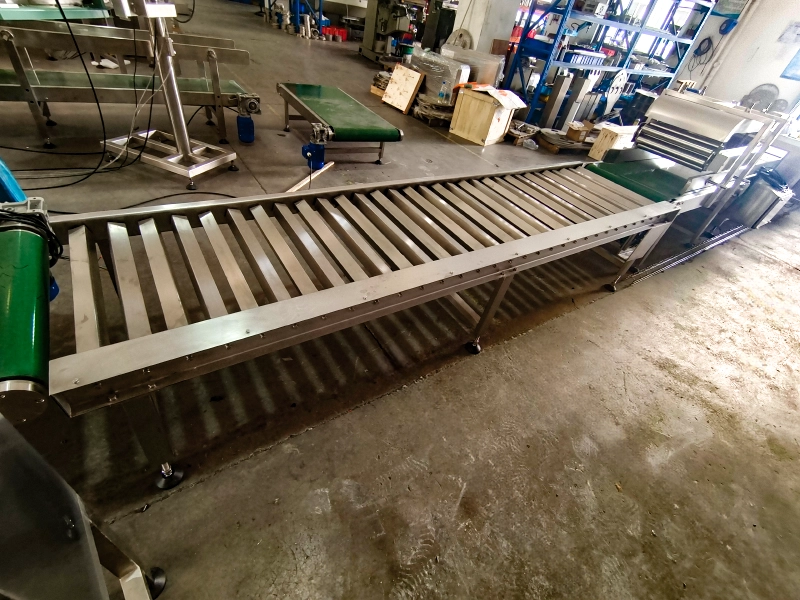
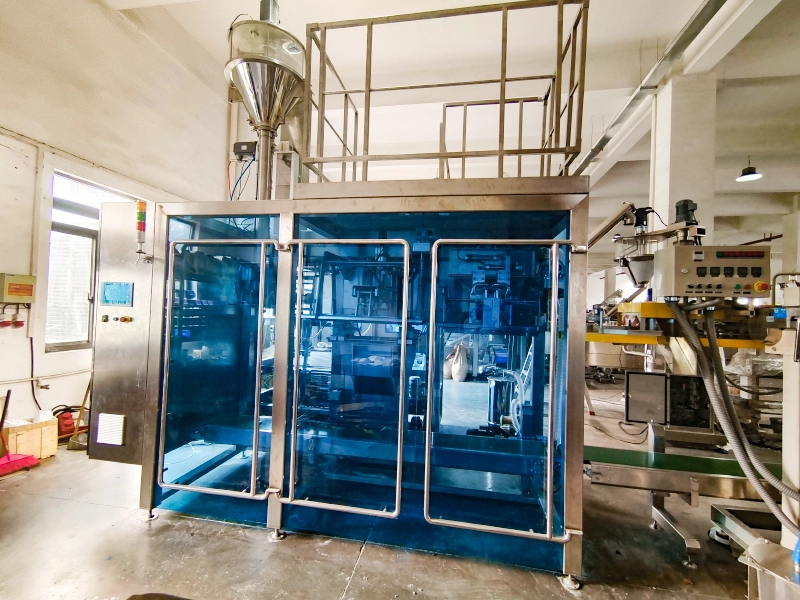
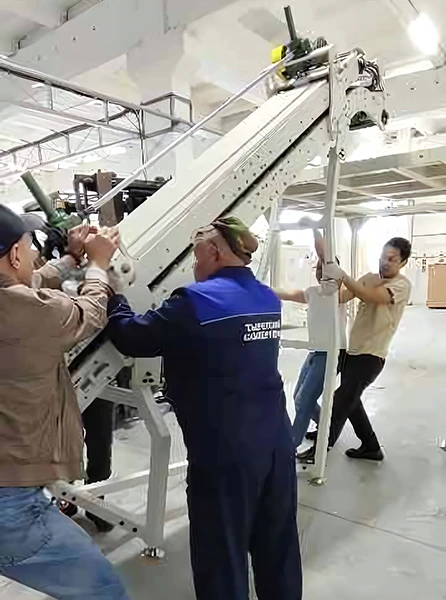
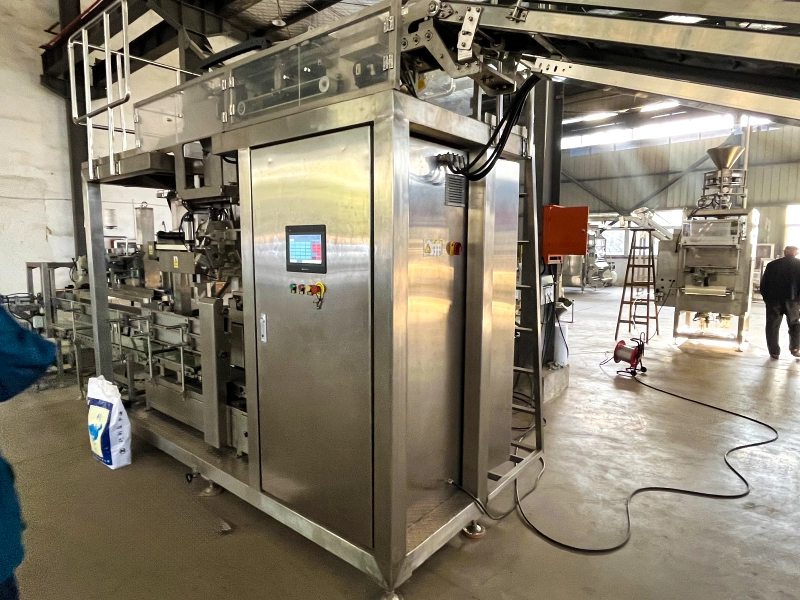
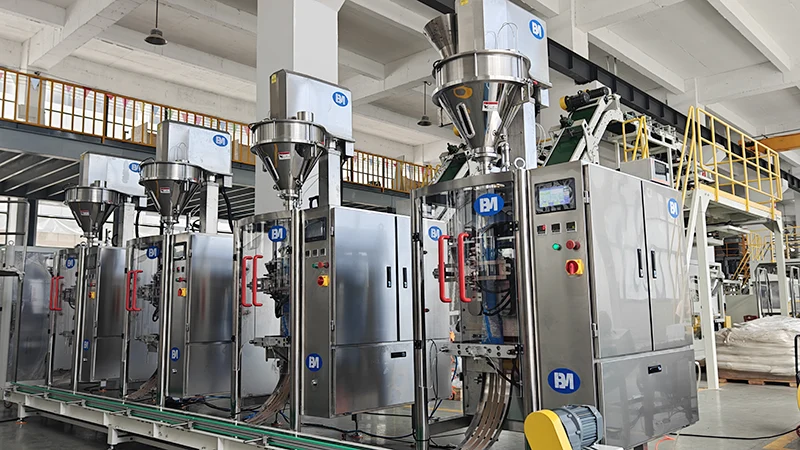
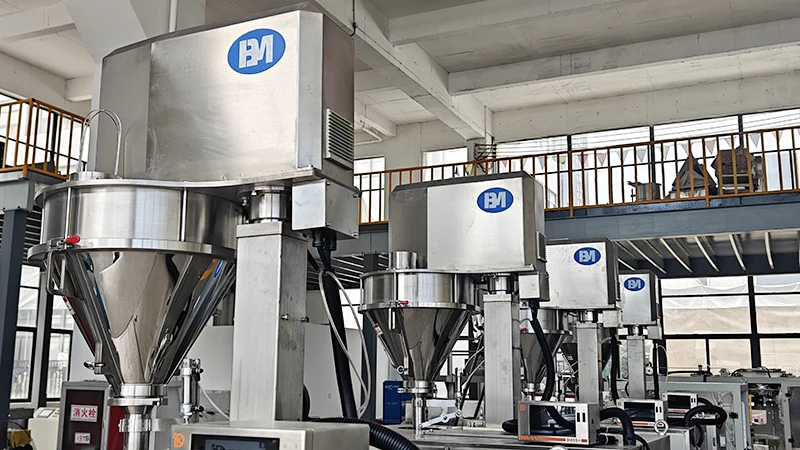
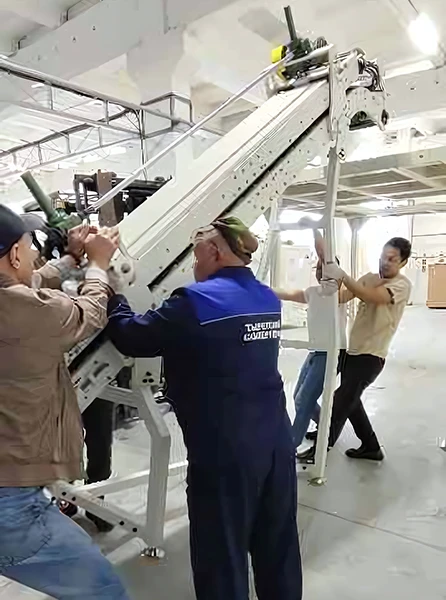
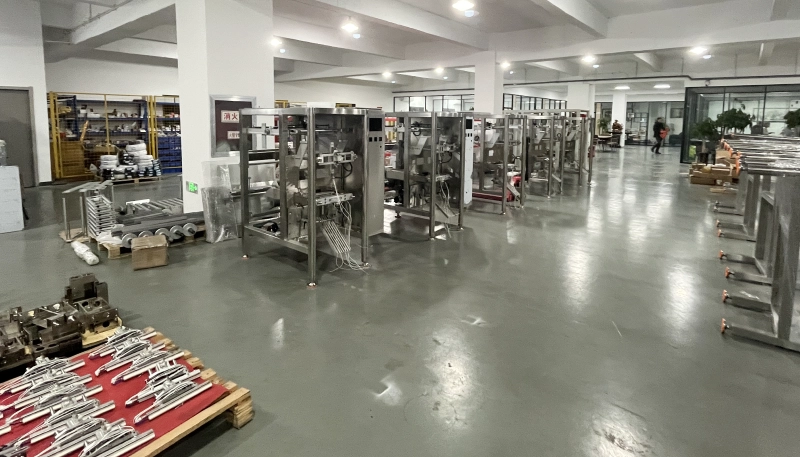
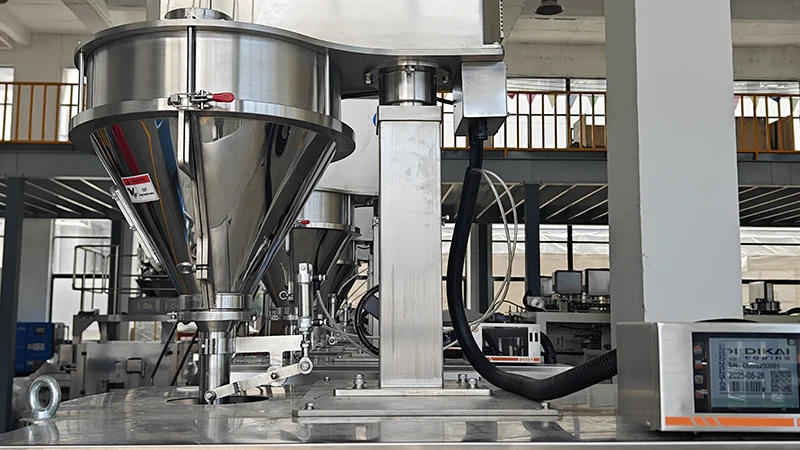
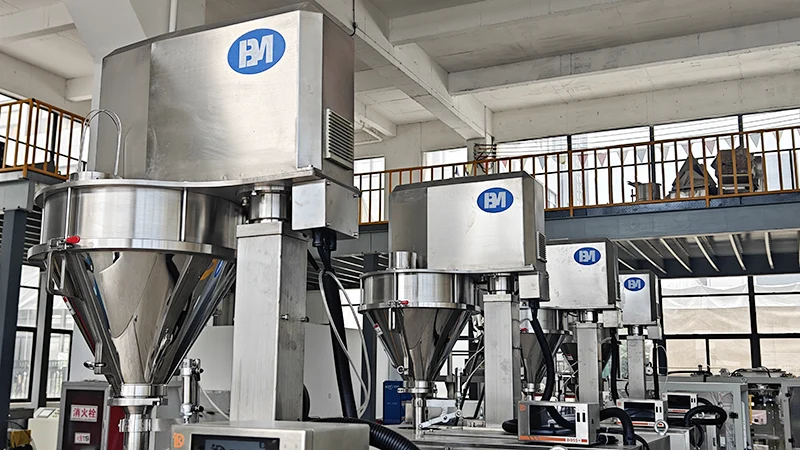
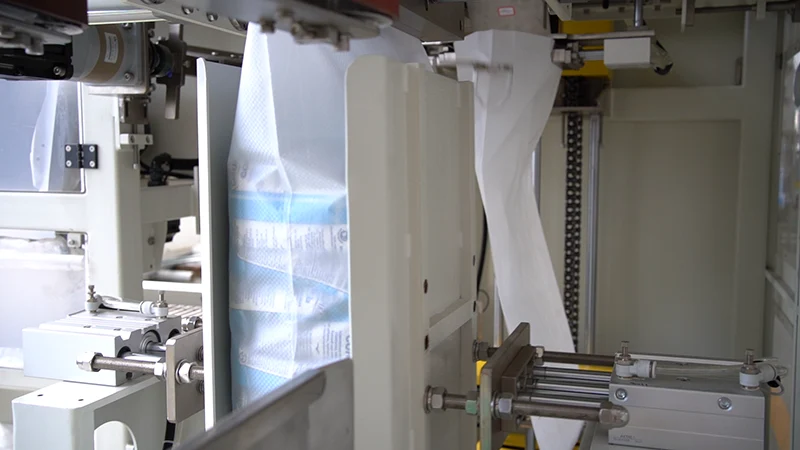
The machine structure shown in the factory photo is not decorative. The hopper gives the product a stable entry point, the cabinet organizes the working section, and the inclined conveyor keeps material flow moving in one direction. The photo also shows how the line is built around visible maintenance access, which helps operators keep the system in production instead of stopping for every small adjustment.
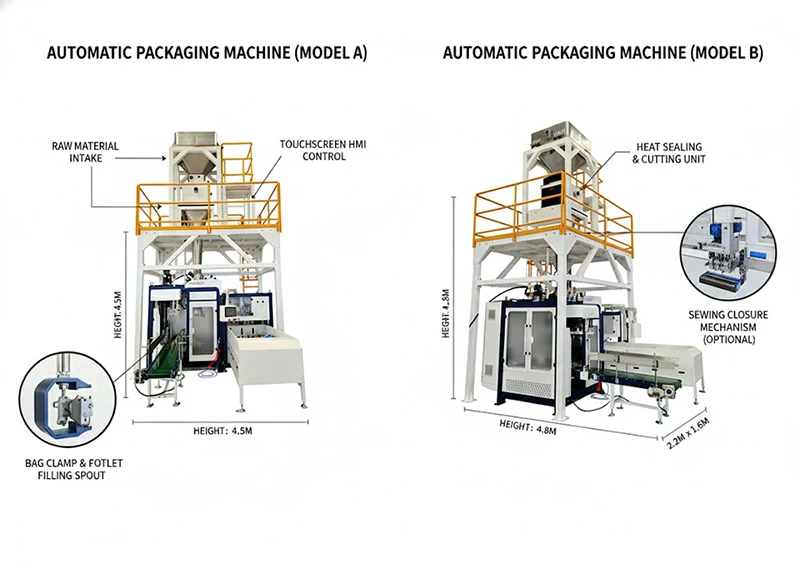
Image evidence and what each image proves
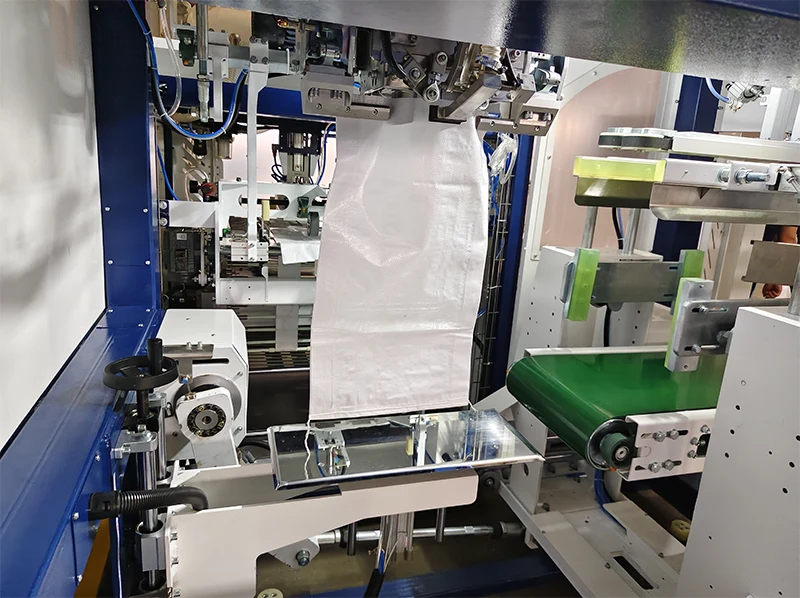
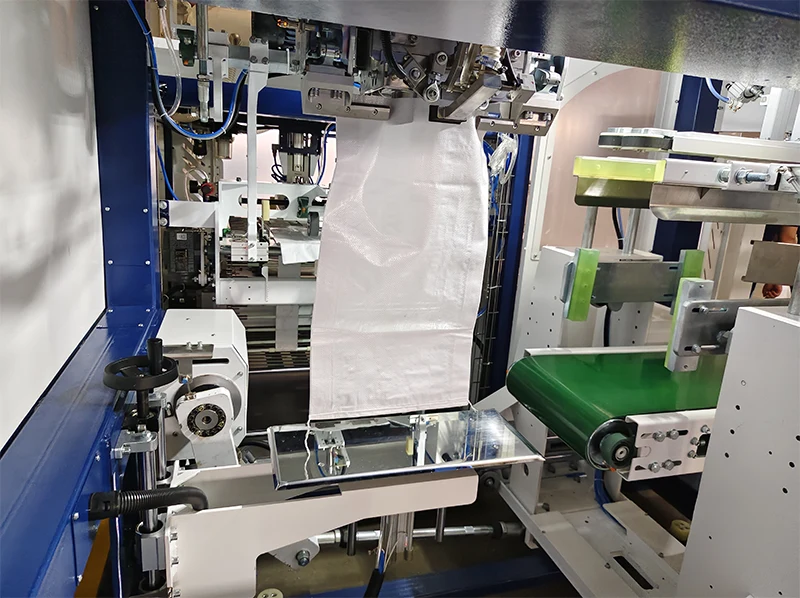
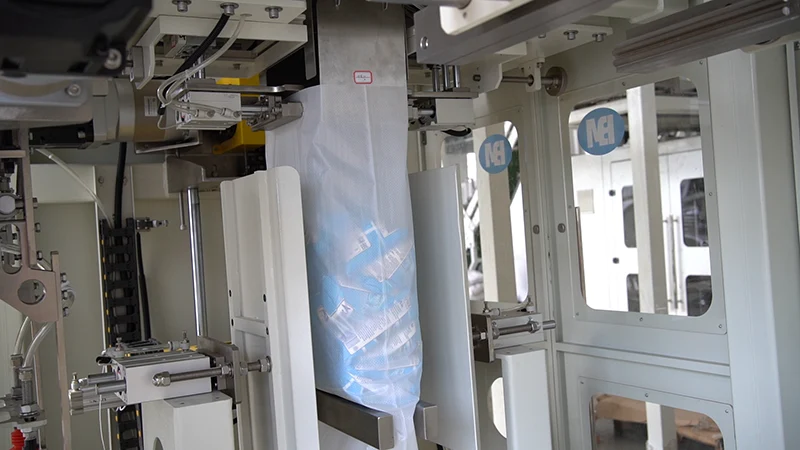
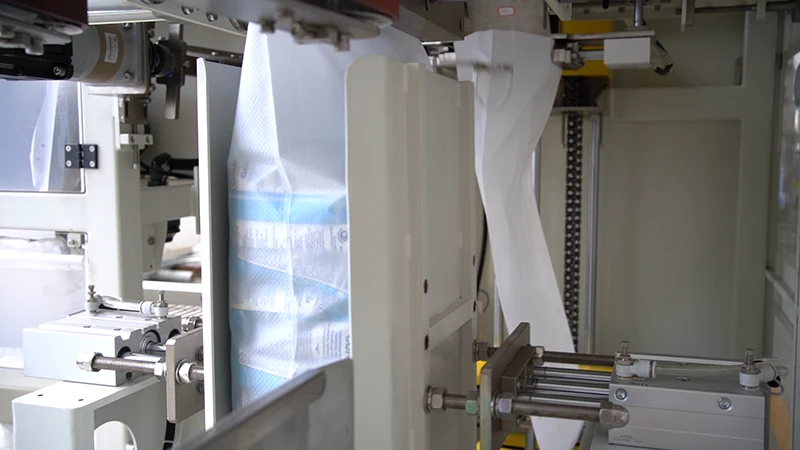
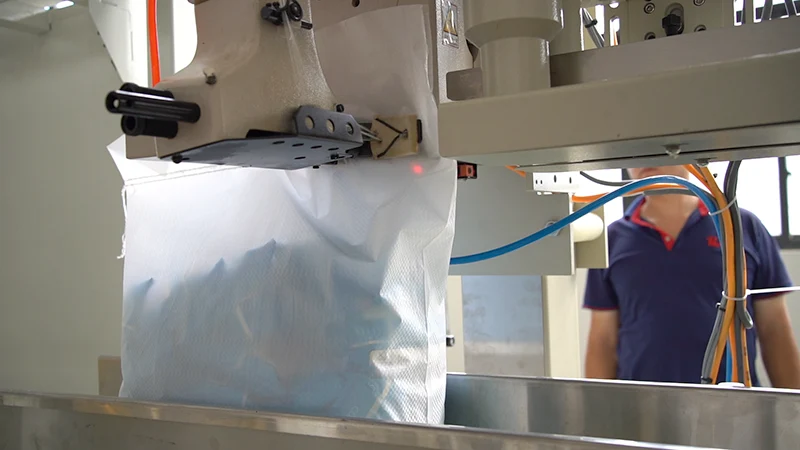
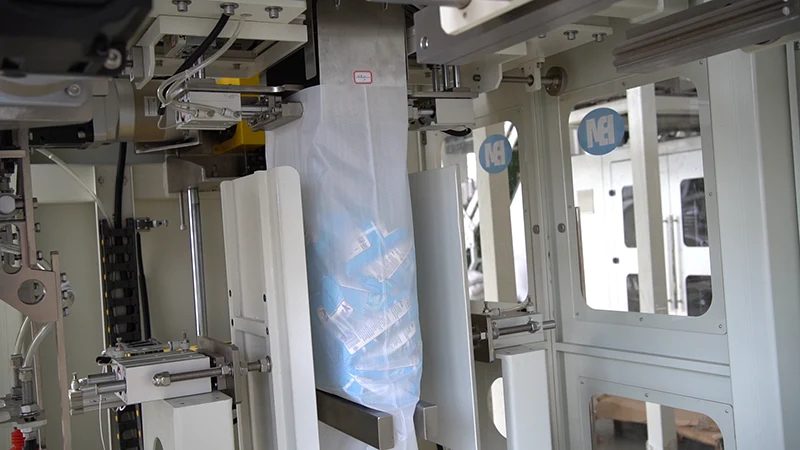
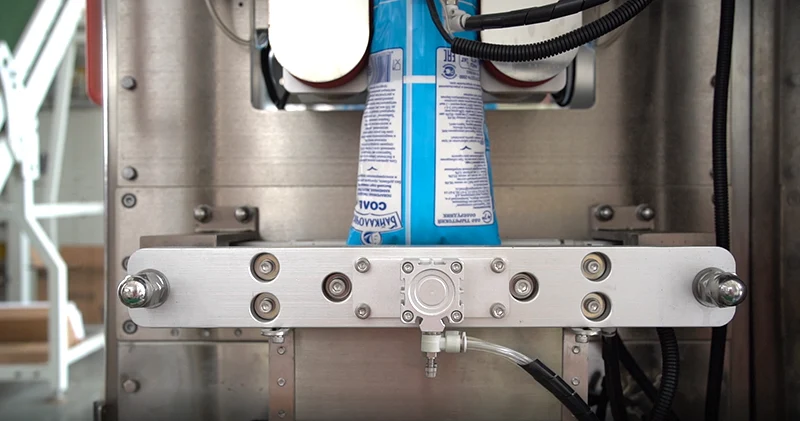
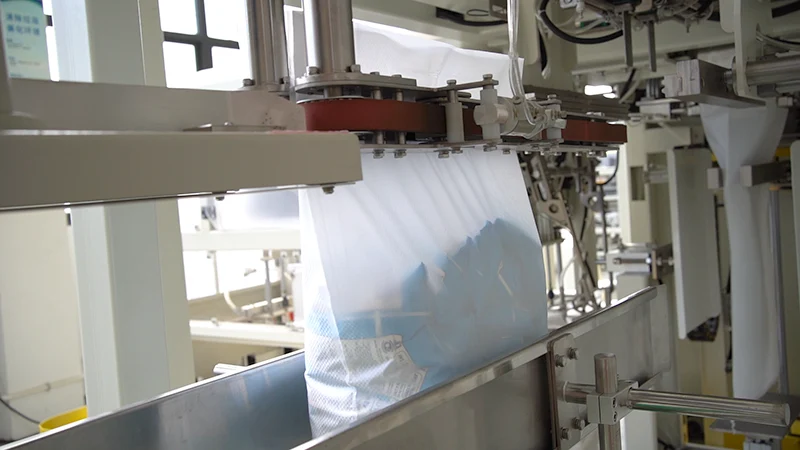
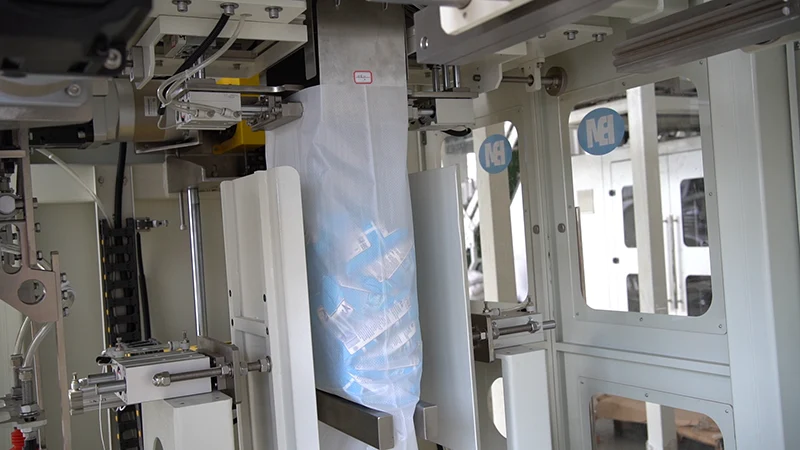
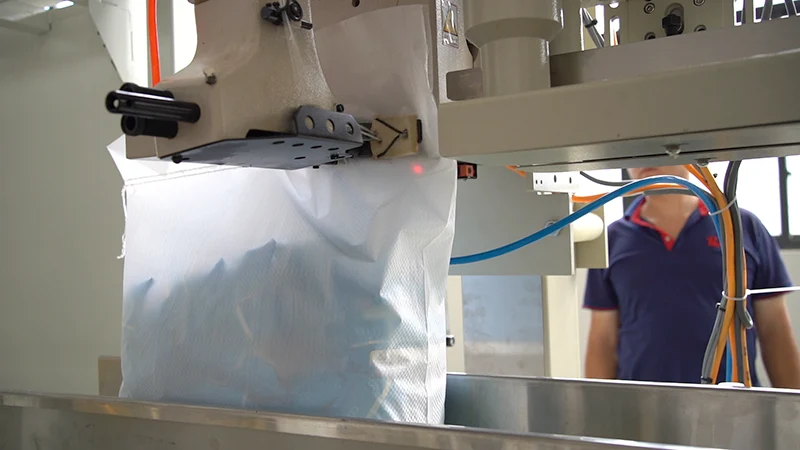
That last detail is what many plants miss. If the bag is not stabilized before sewing, the seam quality becomes a downstream symptom of an upstream alignment issue. PPLINE reduces that risk by keeping the bag supported through the transition zone.
Structure, function, and practical outcome
| Line element | What the image shows | Why it matters in production |
|---|---|---|
| Top hopper feed | A stable, centralized feed point above the working section | Reduces random bag handling and keeps material movement organized |
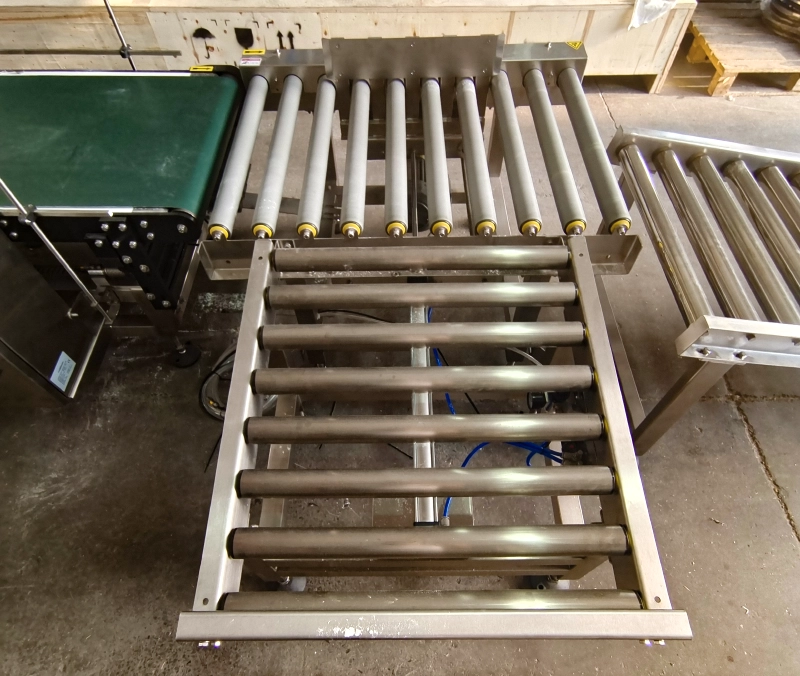
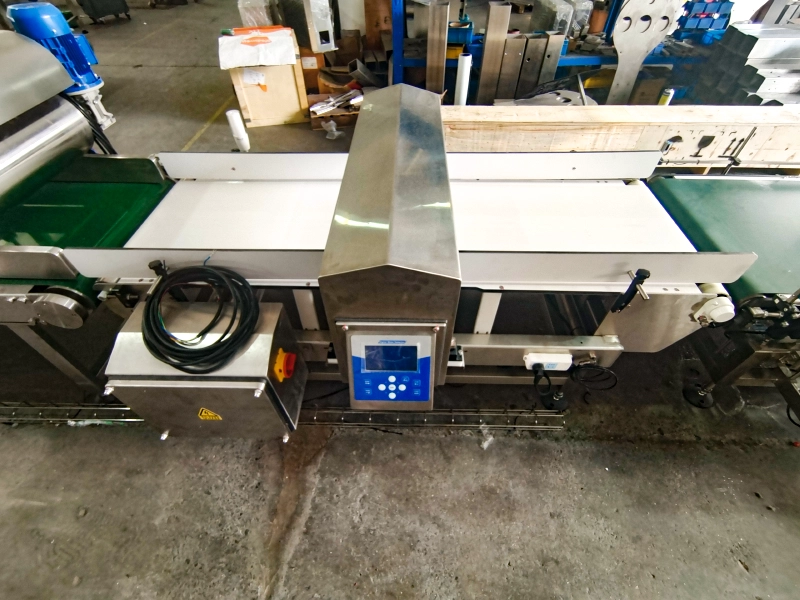
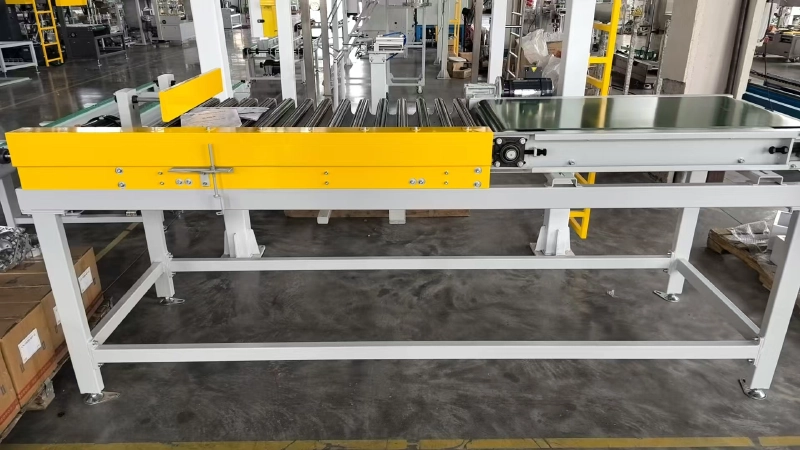
| Controlled conveyor transfer | Guided transport from the processing zone to the next station | Keeps the bag in line instead of letting it skew before sewing |
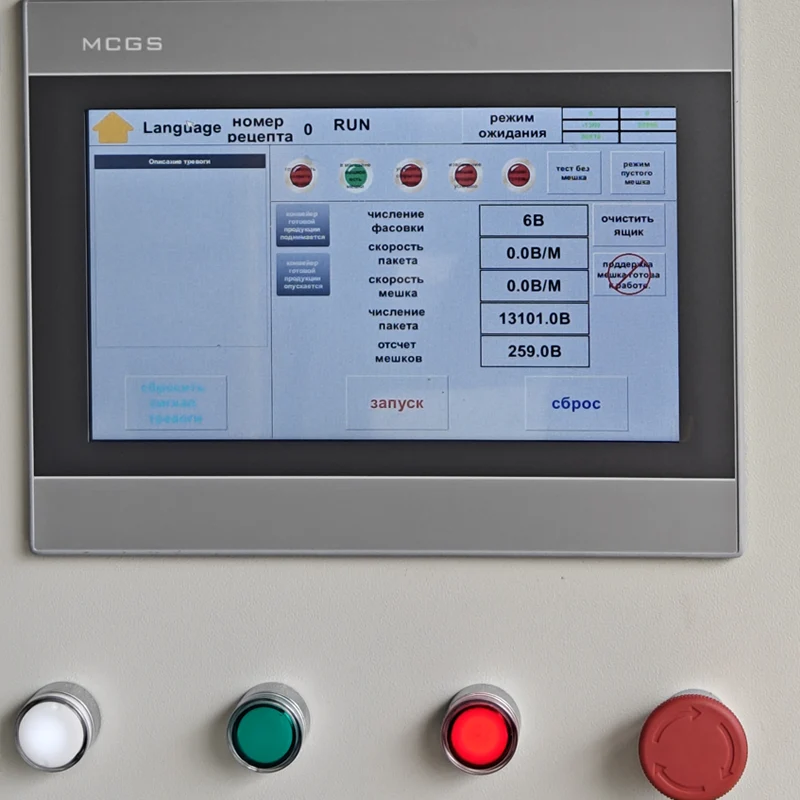
| HMI and enclosure | Visible operator interface and enclosed machine body | Makes line control clearer and maintenance easier for the crew |
| Vacuum hold and press section | Vacuum suction cups, bag press, and conveyor coordination | Improves bag posture at the exact moment when sewing quality is decided |
Result on the shop floor
After the line is set up around stable transfer instead of manual correction, the outcome is straightforward: fewer bag twists, fewer last-second adjustments, a cleaner sewing point, and smoother coordination between operators and equipment. That is especially valuable on bulk-product lines where the plant wants repeatable output, not heroic intervention from the crew on every bag.
For this kind of customer, the benefit is not a single machine headline. It is the way the full PPLINE layout keeps the product moving in a controlled path and gives the sewing station a better starting position. In practice, that means the plant spends less time fixing the bag and more time running the line.
Need a layout review for your bulk-product line?
Send us your bag size, target throughput, and the current transfer problem. We will map where the bag loses alignment and show how PPLINE can hold it straight before sewing.
 English
 Русский