Automatic Bagging Machine & Palletizing Systems Manufacturer

Category: English

  • 25 kg Milk Powder Bagging Line: Stable Bag Transfer Before Sewing

    25 KG MILK POWDER BAGGING LINE

    25 kg Milk Powder Bagging Line: Stable Bag Transfer Before Sewing

    A powder packaging line for dairy plants must do more than fill a bag. Mipline coordinates bag supply, controlled filling, closure and transfer so a 25 kg kraft or paper-plastic bag reaches sewing or sealing with a cleaner mouth and a more stable shape.
    Real factory photo of enclosed stainless-steel powder packaging line with safety doors and conveyor interface

    Why the last bag handoff becomes a dairy powder problem

    In a milk powder or whey powder plant, the difficult moment is often not the first contact between powder and bag. It is the short path after filling, when a heavy bag can twist, collapse, retain air or arrive with its mouth skewed. A conventional conveyor may move the bag forward, but it does not necessarily keep the bag square before sewing. Operators then straighten, open or reposition the package by hand, exposing the sealing area to more powder and making the sewing head less consistent.

    This is the operating context for an automatic powder bagging machine: bag handling, filling, closure and discharge need to be designed as one process. The Mipline concept is intended for 25 kg industrial bags used in dairy powder, flour, starch, feed and selected dry-powder applications. Final suitability still depends on bulk density, flowability, moisture, aeration, bag construction and the required closure method.
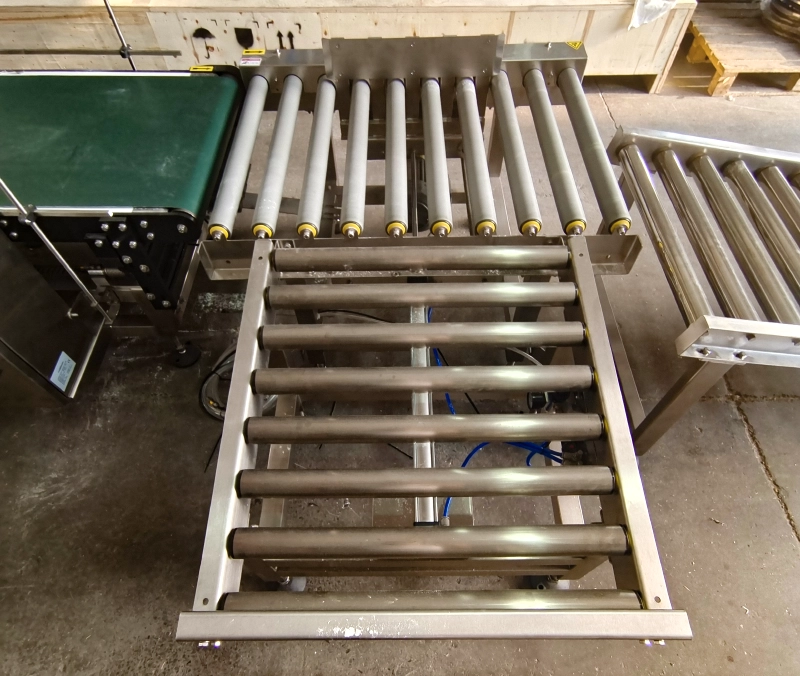
    Stainless steel roller conveyor transfer section with angled rollers for industrial bag handling and line integration
    The old approach: fill first, correct the bag later

    Manual bag straightening at the last meter creates a variable handoff. A dusty or tilted bag mouth can disturb sewing or heat sealing, while uneven settling can make the finished pack difficult to inspect or palletize. The line should control the bag before the operator has to correct it.

    How Mipline adapts the powder filling and bag sewing line

    Mipline uses a bag magazine, vacuum pickup where configured, bag opening, controlled placement and clamping before filling. The filling section is based on vertical screw feeding and weighing control. A bottom-up lifting fill follows the rising powder level, keeping the fill point close to the material rather than relying on open free-fall into an empty bag. This arrangement is designed to reduce powder escape around the bag mouth and leave a better starting condition for closure.

    Three-stage screw feeding—fast filling, medium filling and slow final dosing—supports a controlled weight transition. Depending on the selected configuration, the line can add vacuum extraction or de-aeration before closure. Composite-bag closure may include dust removal, trimming, inner heat sealing, pressing, sewing, hot-melt paper tape and final pressing. The result is not a single generic automatic bagging machine for powder, but a configurable line matched to the bag, powder behavior, target speed and downstream palletizing layout.

    Engineering insight: Stable bag transfer before sewing is created by the complete sequence—clamp alignment, bottom-up filling, settling or shaping, guided conveyor handoff and final inspection—not by a conveyor motor alone.

    Visible structure and project parameters to verify

    The factory evidence shows the physical logic behind the line: enclosed stainless-steel stations, blue inspection windows, a bag magazine conveyor, green belts, roller transfer sections, adjustable guides, control cabinets and emergency-stop protection. One indexed image shows a kraft-paper milk powder bag held at an automatic clamp station; another shows angled rollers used for industrial bag handling. Together, these details support a guided handoff rather than an unsupported claim about capacity or customer performance.

    Reference configurations include a nominal 25 kg application, while published variant data ranges from 1.5–2 bags/min on one 11889 line list to 1–3 bags/min for a DS25K reference. A 5 kW main power reference and SUS304 body are also configuration-dependent inputs. Confirm the bag dimensions, material, target weight, powder properties, closure sequence, air supply, dust extraction, detector effect and checkweigher datasheet during project engineering.
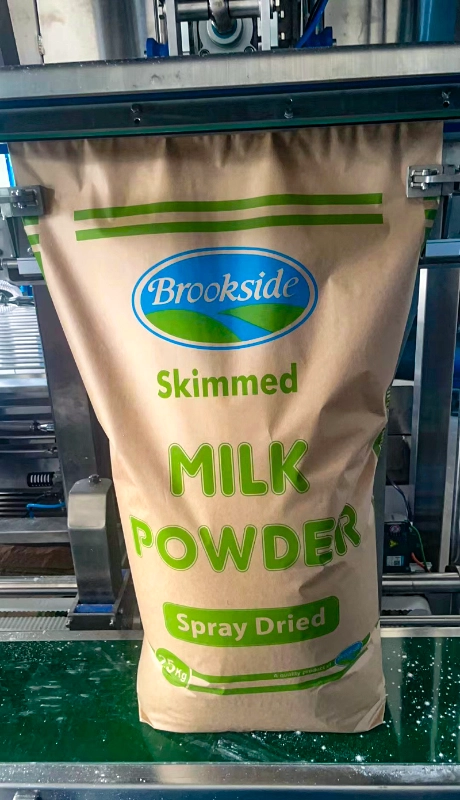
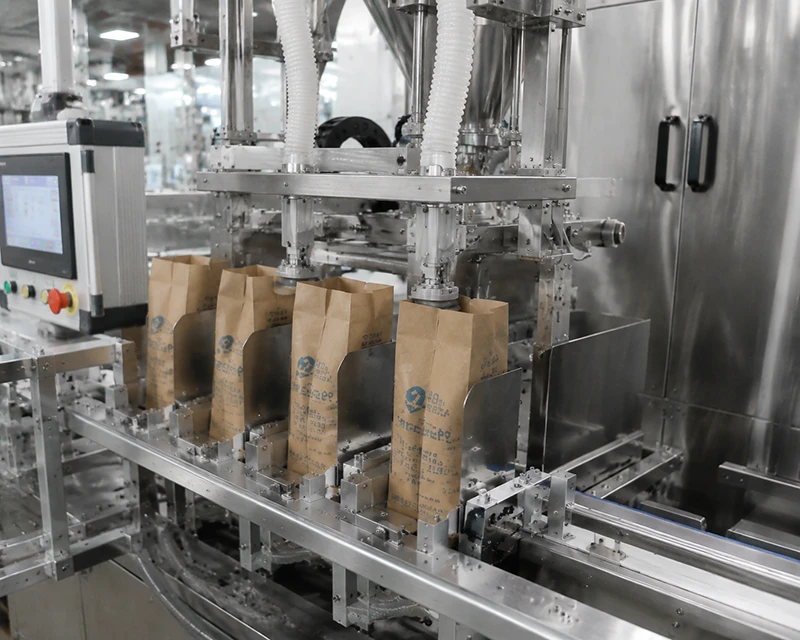
    Real industrial photo of a milk powder kraft bag held at an automatic bagging clamp station
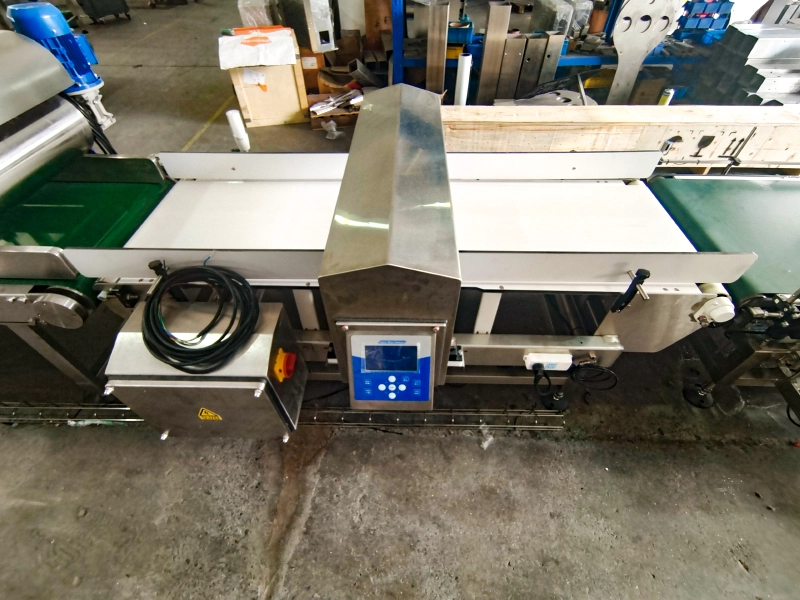
    Stainless-steel twin-belt transfer conveyor with central control housing and adjustable side guides
    Line pointWhat Mipline addressesWhat to confirm
    Bag supply and clampMagazine, pickup, opening and bag clamp alignmentBag construction, dimensions and opening behavior
    Powder fillingBottom-up lift fill with three-stage screw dosingBulk density, flowability, target weight and dust control
    Closure and handoffSealing or sewing sequence with guided roller or belt transferClosure method, line speed and downstream layout
    Final inspectionSettling, shaping, metal detection, checkweighing and reject pathApproved detector and checkweigher configuration
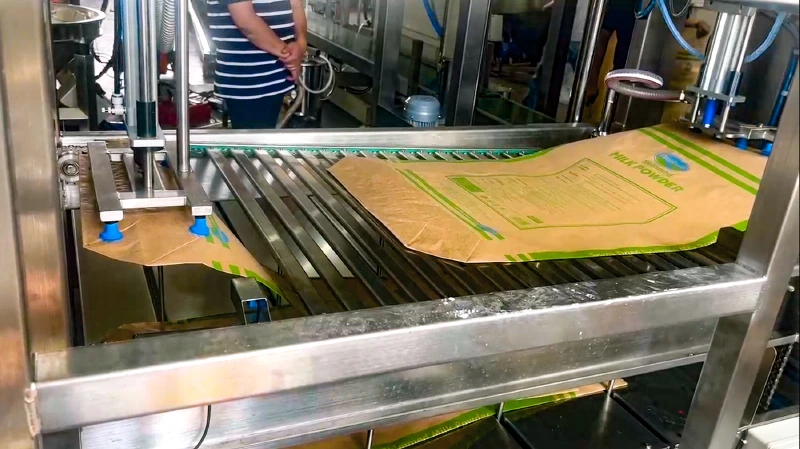
    Stainless steel roller conveyor with vacuum grippers handling kraft paper powder bags on a packaging line

    Specify the powder, bag and sewing handoff

    For a milk powder packaging machine or another dry powder packaging equipment project, share the material, bag type, target weight, required closure, speed and palletizing route. BPM can then define the suitable filling, transfer, inspection and reject configuration instead of applying a generic line specification.

    Discuss Your Powder Packaging Line
  • 25 kg Powder Bagging Line: Keeping Bags Stable Before Sewing

    25 kg Powder Bagging Line: Keeping Bags Stable Before Sewing

    Mipline powder packaging line

    25 kg Powder Bagging Line: Keeping Bags Stable Before Sewing

    For milk powder, flour, starch, feed, and other dry powders, the last transfer before sewing or sealing can decide whether a filled bag arrives square, clean, and ready for the next operation. Mipline combines controlled filling, bag handling, guided transfer, shaping, inspection, and discharge into one automatic powder packaging line.

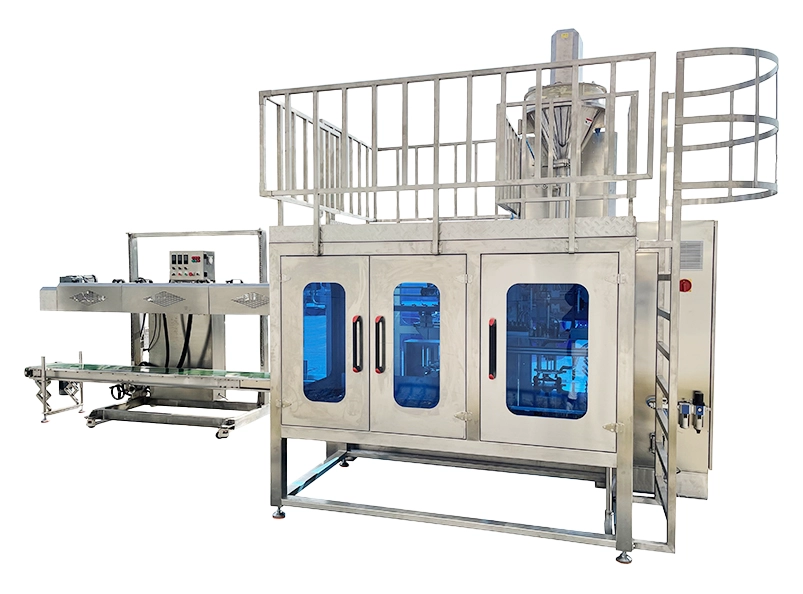
    Stainless steel automatic bagging machine with blue inspection windows, bag magazine conveyor, and top access platform
    Enclosed stainless-steel bagging station with inspection windows, bag magazine conveyor, and access platform.

    Why the last meter becomes a production problem

    A dairy powder or flour plant may have a capable filler and a reliable sewing head, yet still lose stability between them. A filled 25 kg bag can twist, collapse, retain air, or arrive with a skewed mouth. When operators manually straighten the bag at the last meter, the line gains a hidden labor step and the sewing head receives inconsistent material. Dust around the bag mouth can also affect closure quality and housekeeping.

    The issue is not simply conveyor speed. The handoff needs a controlled relationship between the bag clamp, supporting surface, side guides, roller transfer, and the next closure station. That is the practical difference between moving bags and managing bag transfer.

    How Mipline fits the powder-bagging application

    Mipline is configured for industrial dry-powder bags, especially 25 kg kraft paper, paper-plastic composite, and coated woven bags when the material and bag construction are confirmed for the project. The process can include bag magazine supply, vacuum pickup, bag opening, controlled clamping, bottom-up filling, closure, transfer, settling, shaping, inspection, reject, and roller discharge.

    For powders that become aerated or dusty during filling, the bottom-up tracked filling concept keeps the fill point close to the material as the lifting platform follows the fill level. Where specified, vacuum extraction or de-aeration can be integrated before closure. These functions address the earlier problem at its source instead of asking the sewing operator to correct every bag downstream.

    Bag handling evidence: clamp, guides, and transfer

    Real industrial photo of a milk powder kraft bag held at an automatic bagging clamp station
    A kraft-paper milk powder bag held at an automatic bagging clamp station.

    The bag shown at the clamp station illustrates the operating requirement: the bag must be opened, held, and presented to the filling and closure sequence without relying on continuous manual repositioning. A bag magazine, pickup and opening sequence, and controlled clamp can be selected around the bag material, dimensions, powder behavior, and target speed.

    Stainless steel roller conveyor transfer section with angled rollers for industrial bag handling and line integration
    Angled roller transfer section for a stable handoff between powder-bagging stations.

    After filling and closure, roller sections support a more predictable handoff than an un-guided transfer. The Mipline image evidence shows stainless-steel rollers, supporting frames, and a connected transfer layout suited to bag movement and station integration. Adjustable guides and leveling details help the conveyor match the installed line, but final dimensions and speeds remain project-specific.

    From filling to final-bag inspection

    Stainless-steel twin-belt transfer conveyor with central control housing and adjustable side guides
    Twin-belt transfer conveyor with central control housing and adjustable side guides.

    A complete powder filling and bag sewing line should not stop at the filler. Depending on the project, Mipline can combine dust removal, trimming, inner heat sealing, sewing, paper-tape wrapping, pressing, settling, shaping, metal detection, checkweighing, reject, and discharge. Inspection therefore takes place on the finished bag after forming and closure, not only during the filling event.

    Checkweigher and metal-detector performance must be selected from the approved project datasheet because product effect, bag construction, range, and throughput influence the result. The same principle applies to stated capacity: reference configurations include 1–3 bags per minute or 1.5–2 bags per minute, but the applicable figure depends on material, bag, closure method, and line configuration.

    What the plant gains

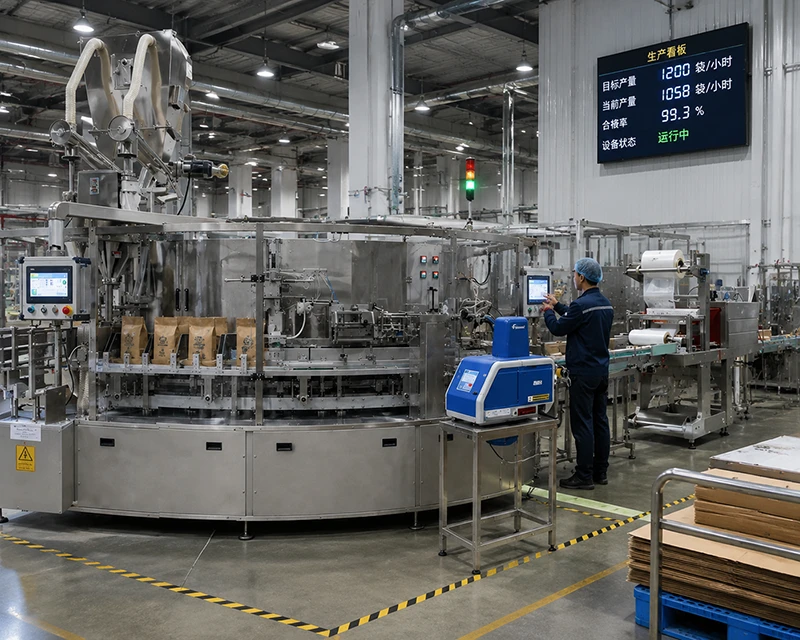
    Real-world automated powder packaging line with safety enclosure, conveyor section, and stacked finished bags
    Enclosed powder packaging equipment with conveying and finished-bag handling in one production environment.

    For a plant replacing manual bag correction, the result is a more controlled path from bag supply to dispatch: cleaner bag-mouth preparation, fewer manual straightening actions, more stable transfer before sewing, and a defined route for inspection and reject. Stainless-steel guarding, blue viewing windows, HMI control, green belts, roller conveyors, and access structures also make the line easier to understand during operation and maintenance.

    The correct Mipline configuration should be confirmed against powder bulk density, flowability, moisture, aeration, bag dimensions, target weight, closure method, available utilities, dust extraction, and palletizing layout. When those inputs are fixed, the powder packaging line can be engineered as a coordinated process rather than a series of disconnected machines.

    Plan a more stable 25 kg powder bag transfer

    Share your powder type, bag construction, target weight, closure method, and required throughput with BPM to define the right automatic bagging machine, transfer conveyor, inspection, and discharge configuration.

  • Mipline Powder Packaging Line for Cleaner Bag Handoff Before Sewing

    Mipline Powder Packaging Line for Cleaner Bag Handoff Before Sewing

    Powder packaging equipment

    Mipline Powder Packaging Line for Cleaner Bag Handoff Before Sewing

    For dairy powder, flour, starch, and other dry powders packed in 25 kg kraft paper or woven bags, the last transfer before sewing can determine whether the finished bag arrives square, stable, and ready for a consistent closure. Mipline combines an automatic powder bagging machine, guided conveyors, bag clamping, and roller transfer sections to reduce manual bag straightening between filling and sewing.

    Stainless steel automatic bagging machine with blue inspection windows, bag magazine conveyor, and top access platform for a powder packaging line

    Why the final meter creates trouble for powder bags

    A filled industrial bag is not a rigid container. After dosing, its center of gravity can shift, the mouth can arrive skewed, and the bag body can twist or collapse while moving toward the sewing head. In a manual arrangement, operators often pull the bag straight at the last meter. That intervention may keep one bag moving, but it makes alignment dependent on operator timing and creates an unstable handoff to the sewing or sealing station.

    For a milk powder packaging machine or flour bagging line, the practical requirement is more specific than simply “convey the bag.” The line must control the bag from filling through transfer: support the base, guide the sides, keep the mouth accessible, and present the bag in a repeatable orientation before sewing.

    Mipline matches the process, not just the filling step

    Mipline is configured as an automatic powder packaging and bagging line for dry powders in industrial bags, especially 25 kg formats. The enclosed stainless steel bagging station provides a defined location for bag handling, while the bag magazine conveyor and upstream feeding devices keep empty bags available for the automatic cycle. Blue inspection windows make the operating area visible without removing the guarding, and the top access platform supports practical maintenance access.

    This matters when a dairy powder plant needs a cleaner transfer between filling, conveying, and sewing. Instead of treating the sewing head as an isolated machine, the line uses the upstream bag handoff as part of the packaging result.

    Roller transfer supports a squarer bag before sewing

    Stainless steel roller conveyor transfer section with angled rollers for stable powder bag transfer before sewing

    The roller conveyor transfer section uses multiple support points to carry the filled bag through a line transition. The visible angled roller arrangement is suited to a controlled change of direction or elevation, while the welded frame and adjustable feet provide a stable base for line integration. Supporting the bag over a broader contact area helps reduce sudden folding or dragging as it leaves the filling area.

    For the operator, the benefit is a more predictable bag handoff before sewing: less time spent catching a collapsing bag, fewer corrections at the conveyor edge, and a better chance of keeping 25 kg bags square as they approach the closure process.

    Guided conveying reduces manual straightening

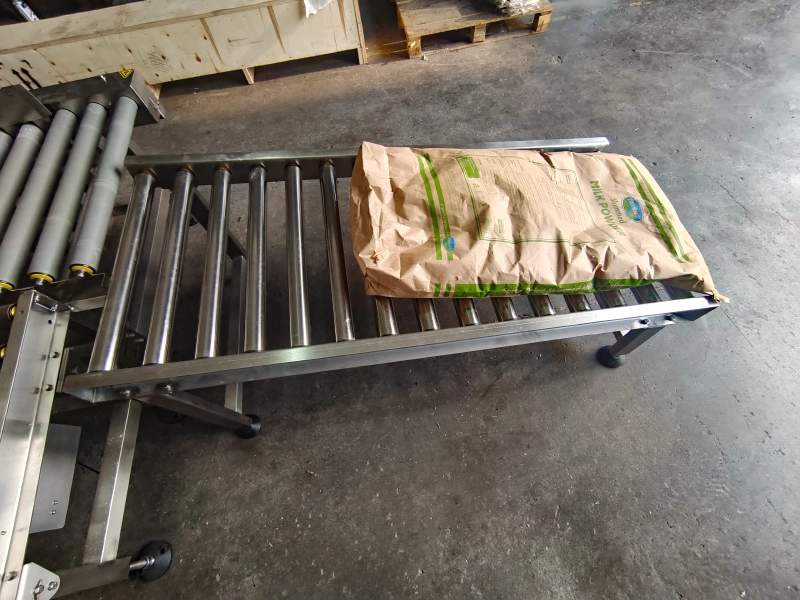
    Stainless steel roller conveyor with kraft paper bag for 25 kg powder bag transfer and line integration
    Kraft paper bag supported on a stainless steel roller conveyor for controlled transfer.
    Stainless-steel twin-belt transfer conveyor with adjustable side guides for cleaner bag alignment before sewing
    Twin-belt transfer with adjustable side guides for stable bag handling.

    The line’s conveying modules address the point where many conventional layouts lose control. A roller conveyor can support and transfer the bag, while a twin-belt section can hold the bag between guided surfaces during a handoff. Adjustable side guides help maintain the travel path without relying on a person to repeatedly push the bag back into position.

    Bag clamping and guided movement work together: the clamp establishes a repeatable reference at the handling station, and the conveyor sections carry that orientation forward. This arrangement is useful for automatic bagging machine applications where the sewing head becomes unstable when the bag mouth arrives skewed.

    Enclosed construction supports a cleaner production area

    Enclosed stainless-steel powder packaging line with safety doors and conveyor interface for dairy powder and flour bags

    Powder handling also places demands on the machine environment. Mipline’s stainless steel enclosure, safety doors, inspection access, conveyor interfaces, and integrated control equipment create a more organized powder packaging line around the bagging operation. The enclosed station separates the handling mechanism from the surrounding production area while allowing visual checks during operation.

    For food powder applications, this structure gives the project team a clearer basis for maintenance planning and line-side cleaning. Final material choices, dosing range, bag dimensions, sewing equipment, and capacity should be confirmed against the actual powder and plant layout, but the visible design establishes the core principle: control the bag continuously instead of correcting it only at the sewing head.

    Result: a more stable powder filling and bag sewing line

    When the customer’s problem is a twisted or collapsing bag before closure, the solution is not another manual adjustment point. It is a coordinated handoff: automatic bag supply, clamping, supported roller transfer, guided belt conveying, and a protected stainless steel bagging station. Mipline applies those elements to 25 kg powder packaging so operators can reduce manual bag straightening, improve bag alignment, and send a cleaner, more stable bag toward sewing or sealing.

    If your application involves milk powder, flour, starch, or another dry powder, share the powder characteristics, bag format, target output, and sewing interface. BPM can then define the appropriate automatic powder packing machine and conveyor handoff around the complete line.

  • Mipline Powder Bagging Line for Stable 25 kg Bag Transfer Before Sewing

    Mipline Powder Bagging Line for Stable 25 kg Bag Transfer Before Sewing

    POWDER BAGGING LINE ENGINEERING

    Mipline Powder Bagging Line for Stable 25 kg Bag Transfer Before Sewing

    For dairy powder, flour, starch, feed, and other dry-powder plants, the difficult point is often not filling alone. It is the controlled handoff from a filled 25 kg bag to closure, sewing, inspection, and discharge. Mipline combines bag handling, bottom-up filling, closure, shaping, and guided conveying so the bag reaches the next station with less manual straightening.

    Stainless steel automatic bagging machine with blue inspection windows, bag magazine conveyor, and top access platform

    Why the last meter becomes a production problem

    A milk powder or flour plant may already have a filler and a sewing head, yet operators still need to open, hold, rotate, or square each heavy bag between them. A bag that twists on the conveyor can arrive with a skewed mouth. Powder on the closure area can make sewing or sealing less stable, while trapped air can leave the finished bag soft and uneven before palletizing. These are practical line-interface problems, not simply labor issues.

    The old arrangement—manual bag placement followed by an ordinary transfer conveyor—does not control enough of the sequence. It moves the bag, but does not consistently manage bag opening, clamping, fill position, settling, shaping, and the handoff before sewing. The result is variable bag presentation and a final-meter correction task that is difficult to standardize across shifts.

    Stainless steel roller conveyor with kraft paper bag for stable powder bag transfer before sewing
    The buyer problem is a controlled handoff, not just a higher filling speed

    If the filled bag mouth is skewed, dusty, or unstable, a faster filler can move the problem downstream. The line should make bag alignment and closure preparation part of the machine sequence.

    How Mipline connects filling, closure, and bag handling

    Mipline is configured as an automatic powder packaging line for industrial bags, typically 25 kg kraft paper, paper-plastic composite, or coated woven bags. A bag magazine and vacuum pickup supply the empty bag; opening and clamping hold it at the filling head. Bottom-up filling uses a lifting platform that follows the fill level, while three-stage screw feeding—fast, medium, and slow final dosing—supports controlled weighing instead of an uncontrolled free-fall stream at the bag mouth.

    After filling, the selected configuration can add vacuum extraction or de-aeration, dust removal, trimming, inner heat sealing, sewing, paper-tape wrapping, pressing, settling, shaping, metal detection, checkweighing, reject, and roller discharge. This sequence is why the equipment fits a powder filling and bag sewing line: it treats the filled bag as a product that must be stabilized and inspected before dispatch.

    Engineering view: The useful performance question is whether the bag remains square and controllable at each interface. Confirm powder bulk density, flowability, aeration, moisture, bag construction, target weight, closure method, line speed, and palletizing layout before freezing the configuration.

    Visible structures that support a cleaner transfer

    The factory images show the physical logic behind the line. The enclosed stainless-steel bagging station uses blue inspection windows and a top access platform, making the guarded bagging area and maintenance approach visible. Downstream, a twin-belt transfer conveyor with adjustable side guides provides a more deliberate path than a flat, unguided belt. A roller section with a kraft paper bag shows the type of bag transfer and support needed before closure or sewing.

    For a 25 kg powder bagging line, these details matter because alignment is created mechanically: the clamp controls the bag during filling, the conveyor guides the bag after filling, and settling or shaping can be placed before final inspection. The final setup may also include a metal detector and checkweigher. Checkweigher values vary by selected model and product effect, so the approved project datasheet—not a universal marketing number—must define accuracy and throughput.

    Stainless-steel twin-belt transfer conveyor with central control housing and adjustable side guides for powder bags
    Stainless steel roller conveyor with vacuum grippers handling kraft paper powder bags at a bag transfer station
    Project pointMipline reference or configuration logic
    Bag and target weightIndustrial powder bags, commonly 25 kg; DS25K reference covers 5–25 kg.
    Filling methodVertical screw feeding with fast, medium, and slow dosing plus bottom-up tracked filling.
    Reference capacityVariant-dependent references include 1–2 bags/min and 1–3 bags/min; confirm the selected material and layout.
    Bag transferGuided belt and roller sections support alignment, settling, shaping, and handoff before sewing.
    InspectionOptional metal detection, checkweighing, reject, and final roller discharge after forming and closure.
    3D render of an automated flour bag conveyor line inside a food processing factory

    Specify the bag handoff before you specify the machine

    Tell BPM your powder, bag material and dimensions, target weight, closure method, required speed, available utilities, and downstream palletizing plan. We can then match the automatic powder packing machine, sealing steps, conveyors, inspection, and reject path to the real process.

    Discuss Your Powder Packaging Line
  • 25 kg Powder Bagging Line for Stable Bag Transfer Before Sewing

    25 kg Powder Bagging Line for Stable Bag Transfer Before Sewing

    POWDER PACKAGING LINE | MIPLINE

    25 kg Powder Bagging Line for Stable Bag Transfer Before Sewing

    For dairy powder, flour, and starch plants, Mipline’s 25 kg powder bagging line combines automatic powder bagging with guided conveying so filled 25 kg kraft paper or woven bags arrive at the sewing or sealing point cleaner, straighter, and with less manual correction.

    Real-world automated powder packaging line with safety enclosure, conveyor section, and stacked finished bags

    Why the last meter matters in powder bagging

    A dairy powder or flour plant may already have a reliable powder filler, yet still lose stability after the bag leaves the filling point of a 25 kg powder bagging line. A soft 25 kg bag can twist, collapse, or drift sideways while it is being moved toward the sewing head. When operators must straighten each bag by hand, the final transfer becomes a variable step rather than a controlled part of the powder filling and bag sewing line.

    Mipline is suited to this scenario because the line is arranged around the complete bag journey: bag magazine and automatic bagging station, bag clamping, guided belt transfer, roller conveyor sections, and the handoff before sewing or sealing. The objective is practical—keep the bag square enough for the next operation while reducing manual bag straightening at the last meter.

    Stainless steel roller conveyor transfer section with angled rollers for industrial bag handling and line integration
    The old transfer problem

    Without a guided handoff, a filled bag can arrive skewed at the sewing head. The operator then has to pull the bag back into line, support its base, or reshape the mouth while the upstream equipment continues running. That interrupts rhythm, makes sewing less stable, and is especially undesirable where a food powder plant needs a cleaner, guarded transfer between filling, conveying, and closure.

    How Mipline adapts the line to the bag

    The Mipline automatic powder packing machine uses a coordinated sequence instead of relying on a single conveyor. The bag magazine presents the empty bag to the bagging station. The clamp holds the bag during filling and handoff. Downstream roller and belt sections support the bag body, while side guides and transfer geometry help control its path before sewing. This is the core reason the system fits 25 kg powder bagging line applications: each stage addresses a different source of movement.

    The equipment is also built as an integrated industrial line rather than a loose collection of machines. Stainless steel enclosures, blue inspection windows, emergency-stop controls, green transfer conveyors, and access points are visible in the factory assets. These details support guarding, operator visibility, and maintenance access around a 25 kg powder bagging line layout.

    Engineering view: The most useful specification is not only the filler itself. It is the controlled relationship between bag clamp alignment, support under the filled bag, guide position, and the roller conveyor bag transfer immediately before sewing.

    Stainless steel roller conveyor with kraft paper bag, used for bag transfer in packaging line

    Visible structures that support cleaner bag handoff

    For a buyer comparing an automatic bagging machine for powder, the following evidence is more useful than a generic automation claim. It shows how the line manages the bag between filling and sewing, where shape and alignment can otherwise be lost.

    Line requirementMipline responseVisible evidence
    Present bags consistentlyBag magazine and automatic bagging stationEnclosed stainless steel station with inspection windows
    Hold the bag during filling and releaseBag clamp alignment at the bagging pointKraft paper bag shown in a clamped industrial work position
    Limit sideways movementGuided belt and roller conveyor transferAngled rollers, side guides, and adjustable support frames
    Connect filling to sewing or sealingModular handoff sections and twin-belt transferGreen conveyors with central control housing and guide rails
    Stainless-steel twin-belt transfer conveyor with central control housing and adjustable side guides

    For milk powder projects, this 25 kg powder bagging line layout can be reviewed against bag material, filled-bag behavior, sewing-head position, and required upstream and downstream interfaces. For flour or starch powder packaging lines, the same review helps define where guides, rollers, guarding, and inspection access should be placed. Final dimensions and operating parameters should be confirmed against the product, bag construction, target output, and closure method.

    Stainless steel roller conveyor with vacuum grippers handling kraft paper powder bags on a packaging line

    Plan a more stable 25 kg powder bagging line

    Share your powder type, bag material, filled-bag size, target capacity, and sewing or sealing arrangement with BPM. The Mipline team can then match the automatic powder packing machine, bag handoff, guides, and conveyor interfaces to the complete line.

    Discuss Your Powder Packaging Line
  • 25 kg Powder Packaging Line for Stable Bag Transfer Before Sewing

    25 kg Powder Packaging Line for Stable Bag Transfer Before Sewing

    Mipline powder packaging solution

    25 kg Powder Bagging Line for Stable Bag Transfer

    For dairy powder, flour, starch, and other dry-powder plants, the last metre before sewing often decides whether a filled bag reaches the closure station square, stable, and ready for a consistent seam. Mipline combines automatic bag handling, guided conveying, and enclosed stainless-steel equipment to create a cleaner handoff from filling to sewing or sealing.

    Stainless steel automatic bagging machine with blue inspection windows, bag magazine conveyor, and top access platform
    Enclosed automatic bagging equipment with a bag magazine interface and access platform.

    When a 25 kg bag arrives at sewing out of square

    A powder plant buying a powder bagging line is not only looking for a filling machine. The complete route must move a flexible kraft paper or woven bag through bag placement, clamping, transfer, and final closure without allowing the bag body to twist or collapse. This is especially important in a milk powder packaging machine, dairy powder bagging line, flour bagging line, or starch powder packaging line where filled bags must continue through the line at a repeatable rhythm.

    With a basic conveyor arrangement, the filled bag can lose its orientation during the last transfer. Operators then straighten the bag by hand, compensate for inconsistent alignment, or slow the sewing head to avoid a skewed bag mouth. That manual correction consumes attention, creates an uneven handoff, and makes the sewing station more dependent on operator timing than on the equipment layout.

    Why Mipline is adapted to the handoff before sewing

    Mipline is configured as an automatic powder packing machine for industrial bags, with the bag path treated as one connected process rather than a series of isolated machines. The enclosed stainless steel bagging station provides a controlled area for bag loading and handling. In any powder bagging line, a stable bag at this stage protects the downstream sewing quality. Blue inspection windows make the active zone visible, while the bag magazine conveyor gives the upstream bag supply a defined entry point.

    After filling, the transfer route can use clamping, side guidance, belt conveying, and roller conveyor sections to keep the bag supported while it changes direction or passes between modules. The result is a more stable bag handoff before sewing: the bag has a guided path, the mouth is less likely to arrive skewed, and operators have less need to perform manual bag straightening at the final metre.

    Visible machine evidence in the powder bagging line

    Stainless steel roller conveyor with vacuum grippers handling kraft paper powder bags on a packaging line
    Vacuum gripping and roller support demonstrate controlled bag handling at the transfer point.

    Bag placement and clamping

    The bag-contact equipment is visible rather than hidden behind a generic line description. Vacuum grippers handle the kraft paper bag at the loading and transfer point, while the surrounding stainless steel frame provides a defined working envelope. This arrangement supports the practical requirement of an automatic bagging machine for a powder bagging line: place the bag, hold it, and hand it into the next movement without relying on an operator to recover its position.

    Stainless steel roller conveyor transfer section with angled rollers for stable powder bag handling before sewing
    Angled rollers create a visible transfer section for industrial bag movement and line integration.

    Roller transfer and alignment

    The stainless steel roller section is suited to the portion of the line where a filled bag must remain supported while transferring between conveying directions. Angled rollers and the supporting frame help define the bag route, providing a more repeatable approach to sewing or sealing than an open, unsupported gap. For plants handling 25 kg bags, this is the physical link between filling performance and closure consistency.

    Stainless-steel twin-belt transfer conveyor with central control housing and adjustable side guides for clean bag handoff
    Twin-belt conveying with adjustable side guides supports a controlled bag handoff.

    Guided transfer before closure

    The twin-belt transfer conveyor adds side guidance and a central control housing to the conveying path. These visible elements address the common buyer concern in a powder bagging line that a filled bag twists or arrives collapsed before the sewing head. By keeping the bag supported and guided through the transfer, the line is designed to reduce correction work and provide a cleaner interface with downstream sewing or sealing equipment.

    From filling to a more predictable final result

    The practical outcome is not simply a more automated conveyor. A properly connected powder filling and bag sewing line gives the plant a clearer process: the bag is supplied from the magazine, handled at the enclosed station, transferred on supported conveyor sections, and guided toward closure. Stainless steel construction, inspection access, bag clamping, roller conveyor transfer, and adjustable side guidance are all visible parts of that process.

    For a buyer comparing a 25 kg powder bagging line, the key question is whether the machine addresses the last handoff as carefully as the filling step. Mipline is built around that requirement. It helps keep bags square before sewing, supports stable bag transfer, and gives dairy powder, flour, starch, and other dry-powder operations a cleaner route from filled bag to finished, closed package.

    Real-world automatic powder packaging line with safety enclosure, conveyor section, and stacked finished bags
    Automatic powder packaging equipment with enclosed handling and finished-bag output.
  • Tomato Cubes Packaging: Is a Zpacker Automatic Paper Bag Packing Machine the Right Fit?

    Tomato Cubes Packaging: Is a Zpacker Automatic Paper Bag Packing Machine the Right Fit?

    ZPACKER APPLICATION ASSESSMENT

    Tomato Cubes Packaging: Is a Zpacker the Right Fit?

    For tomato-cube production, the first question is not simply whether a packaging machine can fill a bag. The material shape, moisture, flow behaviour and premade bag format must match the process. Zpacker is built primarily as an automatic paper bag packing machine for flour and compatible powders; tomato cubes should therefore be treated as a test-led application rather than an assumed standard fit.

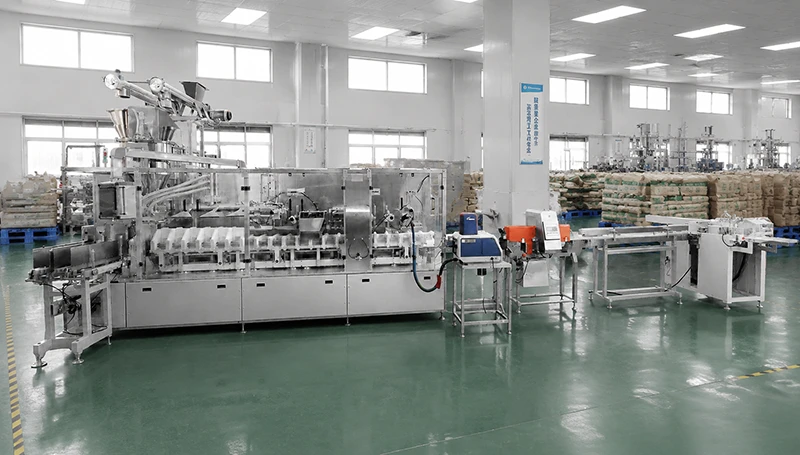
    Zpacker automatic paper bag packing machine with touchscreen for food production packaging assessment

    Start with the customer process, not the machine name

    A tomato-processing plant may need to move diced tomato pieces from production into retail or food-service bags while keeping product shape, fill weight and sealing quality consistent. That requirement is different from the normal Zpacker application: 1 kg, 2 kg and 5 kg flour packing into premade paper bags, kraft bags or M-fold side-gusset bags. For tomato cubes packaging, that flour-focused baseline is the comparison reference.

    That distinction matters because tomato cubes are not automatically equivalent to powder. Pieces can bridge in a hopper, behave differently in a screw dosing system and carry moisture into the sealing zone. Before specifying an automatic packaging line for tomato cubes packaging, the buyer should provide representative tomato cubes, target weights, bag samples, product temperature, moisture range, bulk density and the required rate. A material test is the correct next step; a catalogue assumption is not.

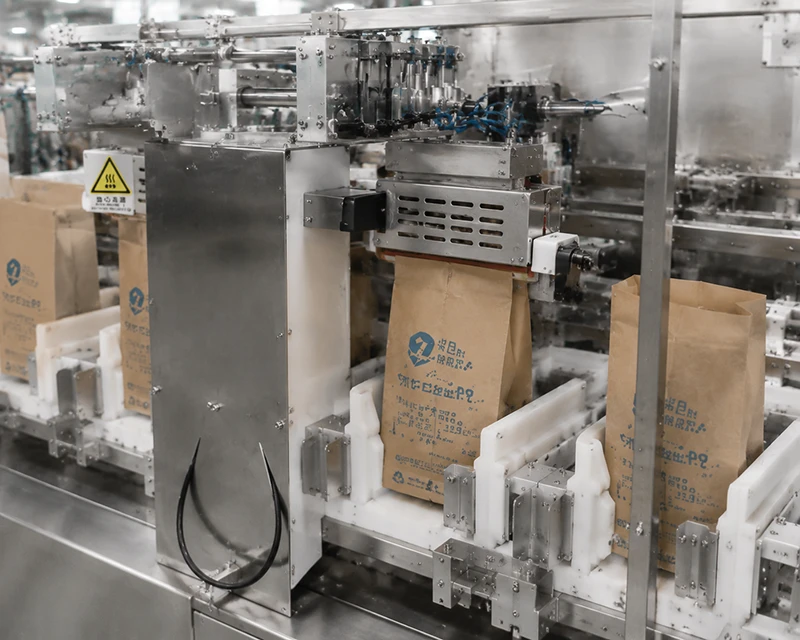
    Zpacker automatic paper bag feeding and opening station for premade kraft bag packaging
    The main risk is process mismatch

    Manual filling can create variable weights, slow bag handling and inconsistent sealing. A standard powder line can create a different problem: its screw dosing, dust-removal sequence and paper-bag forming stations are designed around powder flow, not necessarily around discrete tomato pieces. The machine must be accepted against a tested product-and-bag combination.

    Why Zpacker may still be relevant to a tomato-cube project

    Zpacker has a complete premade-bag process rather than a simple open-fill station. The bag is picked from the magazine, opened and positioned, then transferred through filling, settling, edge preparation, glue application and top pressing. For its intended powder applications, multiple vibration and dust-removal stages help the material settle and keep powder away from the sealing area. For tomato cubes, those same stations must be reviewed carefully so that vibration, transfer height and compression do not damage the product.

    The line architecture is also suitable for a structured feasibility discussion. A 10.4-inch touchscreen and PLC-based controls support recipe and sequence management, while the downstream layout can be connected to conveying, checkweighing, metal detection, date printing and secondary packaging where the tested product requires them. These are configuration options to validate, not promised tomato-cube performance.

    Engineering checkpoint: Tomato cubes should be evaluated as a possible extension application. Confirm product integrity, hopper discharge, bag orientation, sealing cleanliness and achievable speed with actual samples before selecting the screw dosing and premade-bag configuration.

    What to verify before approving the packaging line

    The visible equipment provides useful evidence of the process boundary. The paper-bag station shows the bag magazine, clamps and touchscreen; the complete-line views show how dosing, the main bagging machine and outfeed conveyor can be arranged; the factory-floor view shows the need to coordinate operator access, upstream feeding and downstream handling.

    For a tomato-cube production project, the following checkpoints for tomato cubes packaging should be recorded in the final technical proposal. Zpacker reference values below belong to the powder-oriented configuration and must be confirmed or revised after testing.

    CheckpointZpacker referenceTomato-cube approval question
    Product and dosingPowder-focused screw dosing; about ±0.5% reference accuracyCan the product discharge without bridging or damage, and what dosing method is validated?
    Bag formatPremade paper or paper-plastic M-fold square-bottom bags; 1–2 kg and 2.5–5 kg rangesDo the tomato-cube bags match the tested dimensions, orientation and material strength?
    SealingHot-melt glue point or line spray followed by top pressingDoes moisture remain outside the adhesive and sealing path at the target temperature?
    Line speedAbout 30–35 bags/min for the 1–2 kg powder reference; final rate depends on material and feedingWhat stable rate is demonstrated with real tomato cubes and the selected bag?
    Downstream checksConveyor, checkweigher, metal detector, date printer and secondary packing can be consideredWhich inspection, grouping and pallet or case-packing steps are required after filling?
    Utilities and layout15.5 kW; 380 V ±10%, 50 Hz; compressed air values require final confirmationAre air, power, cleaning access and the available installation space suitable for the tested line?
    Zpacker factory floor packaging machine with touchscreen, hopper, and production line

    Use the test to define the final result

    For tomato cubes packaging, a suitable result is not an unverified promise of automatic packing. It is a documented decision: either the tested Zpacker configuration can handle the product and premade bag at the required weight and rate, or the project needs a different dosing and sealing route. This approach prevents the common failure of replacing manual filling with equipment that solves bag handling but not product flow or seal contamination.

    If the tests confirm compatibility, the project can be developed as an automatic packaging line with defined feeding, bag opening, dosing, inspection and secondary-packaging interfaces. If they do not, the test data still gives the food producer a precise basis for selecting another machine type. Send the product sample information, target bag and production rate for a configuration review.

    Wide Zpacker automatic packaging line with feeding system, conveyor, and bag handling area

    Discuss the tomato-cube packaging test

    Share the tomato-cube sample, target fill weight, bag drawing, moisture range and required output. BPM can then confirm whether the Zpacker premade paper-bag process is technically suitable and define the equipment interfaces.

    Request an application review
  • How Flour Is Packed at a Pasta Factory: The Zpacker Automatic Packaging Line

    How Flour Is Packed at a Pasta Factory: The Zpacker Automatic Packaging Line

    FLOUR PACKAGING LINE FOR PASTA PRODUCTION

    How Flour Is Packed at a Pasta Factory: The Zpacker Automatic Packaging Line

    At a pasta factory, packing flour into 1 kg, 2 kg, and 5 kg paper bags requires more than accurate dosing. The line must handle a premade M-fold bag, control flour dust, close the bag cleanly, and connect with downstream inspection. Zpacker combines bag feeding, screw dosing, dust removal, sealing, and product transfer in one automatic packaging line.

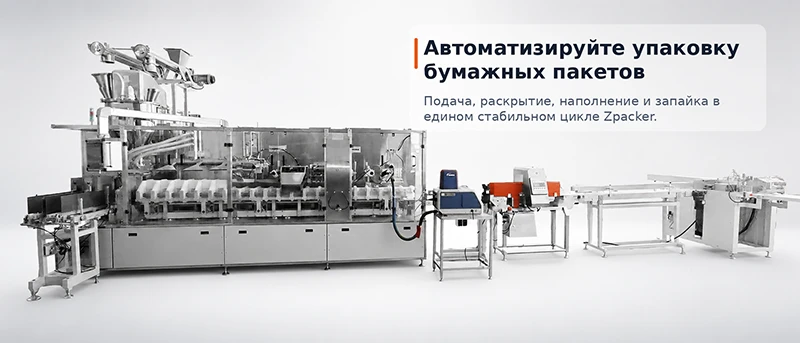
    Wide zpacker automatic flour packaging line in a pasta factory with horizontal paper bag machine, feeding system, conveyor, and bag handling area

    From flour storage to a finished paper bag

    A typical flour packaging line starts with a flour storage silo or buffer hopper. A screw conveyor transfers the product to the dosing section, where a twin screw dosing system is configured for powder filling. The premade kraft bag then enters the horizontal paper bag packaging machine. This is a key distinction: Zpacker handles a finished paper or paper-plastic bag rather than forming a bag from roll film.

    For a pasta factory, this format supports common retail sizes. One configuration covers approximately 1–2 kg, while another covers approximately 2.5–5 kg. Reference output is about 30–35 bags per minute for the 1–2 kg range and 15–20 bags per minute for the 2.5–5 kg range. Final speed depends on flour properties, the feeding system, and agreed acceptance conditions.

    Close view of zpacker automatic paper bag feeding and opening station with kraft bags, bag clamps, stainless frame, and touchscreen control
    Why manual flour filling creates instability

    In a manual process, operators must pick up a flat bag, open it, hold it during filling, and then form and close the top. Flour dust can reach the sealing area, the product may not settle evenly, and extra handling is needed before checkweighing. A semi-automatic machine removes some labor, but it can still leave a gap between filling the premade bag and connecting inspection, conveying, and secondary packaging.

    How Zpacker processes an M-fold premade bag

    A belt feeder transfers each bag from the magazine to the gripping station. The bag with side gussets is opened into its stable shape, positioned, and held beneath the filling point. After automatic screw dosing, vibration and dust removal help the flour settle and reduce material around the bag mouth. The line then reforms the M-fold, trims and rolls the edge, applies hot-melt adhesive by spot or line spraying, and presses the top closed.

    This sequence covers the full process that a standard machine for filling ready-made bags may not provide without dedicated forming operations. When no bag is available, the system does not open, fill, or seal. Air-pressure errors, open safety protection, drive faults, and abnormal glue temperature can trigger a stop and operator alarm.

    Production insight: When evaluating powder packaging equipment, check more than target weight. The bag sample, feed direction, side-gusset size, flour behavior, and available feed capacity determine whether the automatic packaging line will run consistently.

    Which line functions create the final result

    The visible modules connect flour filling with the next logistics steps. Product-contact areas use 304 stainless steel, while the touchscreen supports recipe and operation control. A PLC controller coordinates gripping, dosing, settling, dust removal, and sealing. After the main machine, the line can be connected to a checkweigher, metal detector, date printer, conveyor, bag arranger, and secondary packaging equipment.

    This gives a pasta factory a practical choice between grouped shrink-film packaging and manual bagging or case packing, depending on warehouse requirements and the desired automation level. Before engineering, confirm the paper bag format, 1–5 kg product range, target speed, air consumption of approximately 0.76 m³/min, 380 V ±10% and 50 Hz power supply, and available installation area. These are reference values and must be confirmed in the final specification.

    Item to confirmZpacker referenceCustomer input
    Bag material and formPremade paper or paper-plastic M-fold bag with square bottomBag samples, feed direction, and layer bonding
    Filling rangeApproximately 1–2 kg or 2.5–5 kgTarget SKUs and allowable weight deviation
    DosingTwin screw dosing; approximately ±0.5% reference accuracyFlowability, dust behavior, and test flour
    Downstream processCheckweigher, metal detector, date printer, arranging, and grouped packingInspection and warehouse logistics requirements
    Clean full zpacker flour packaging line with paper bag machine, screw dosing unit, outfeed conveyor, and downstream equipment

    Specify a flour packaging line for your paper bags

    Prepare a bag sample, 1 kg, 2 kg, or 5 kg SKU requirements, flour characteristics, target speed, and downstream inspection needs before requesting a configuration. BPM can match the screw dosing system, dust removal, sealing process, and equipment after the Zpacker packaging machine.

    Request a packaging line review
  • Flour Packaging Equipment for Mills: How Zpacker Controls Dust and Cuts Manual Handling

    Flour Packaging Equipment for Mills: How Zpacker Controls Dust and Cuts Manual Handling

    ZPACKER | AUTOMATIC PAPER BAG PACKAGING

    Flour Packaging Equipment for Mills: How Zpacker Controls Dust and Cuts Manual Handling

    For a flour mill, food factory, or bakery plant, an automatic flour packaging line must do more than dose powder. Zpacker connects premade paper-bag handling, screw dosing, bag settling, dust removal, sealing, and downstream inspection for practical 1–5 kg retail formats. This overview shows where the equipment fits, what a manual or semi-automatic process leaves unresolved, and which bag, utility, and line conditions should be confirmed before quotation.

    Wide bright workshop view of zpacker full packaging line with horizontal bagging machine, upper feeding system, conveyor, and bag handling area

    From flour storage to a controlled paper-bag process

    A mill or food production plant normally starts with flour storage silos or a buffer hopper, then moves powder through a screw conveyor or elevator to the packing area. The requirement is not simply a powder filling machine. The line must take a preformed paper or paper-plastic bag, open and orient it, dose the flour, settle the material, close the top, and transfer a stable finished pack to inspection or secondary packing.

    Zpacker is built around this sequence. Its full automatic, two-station linear format is intended for M-fold, square-bottom premade bags rather than roll film. A typical configuration covers about 1–2 kg on one specification and about 2.5–5 kg on another, with the final range confirmed through the customer’s bag samples and material test. That makes it relevant to the 1 kg, 2 kg, and 5 kg paper-bag formats commonly planned for retail flour.

    Close view of zpacker automatic paper bag feeding and opening station with kraft bags, bag clamps, stainless frame, and touchscreen
    What manual and semi-automatic packing leaves exposed

    With manual filling, operators repeatedly pick bags, open them, hold the mouth below the filling point, and close each pack. A semi-automatic machine may improve dosing but still leave bag opening, M-fold forming, trimming, gluing, and hand-off between stations to people. The result is an uneven workflow: powder can escape around the mouth, flour may not settle before sealing, and a dusty seal area can weaken the finished closure. Changing between retail weights also creates repeated adjustment and handling work.

    Why the bag shape and powder route matter

    After the premade bag is picked from its magazine, the clamps open it into a three-dimensional bag for filling. Once the flour is dosed, the process continues with several vibration and dust-removal positions to help release air and settle the powder. The M-fold is then folded back, the top can be trimmed and rolled, and hot-melt adhesive is applied by dot or line spray before the top is pressed into shape. This is a paper-bag sealing process, not heat sealing of a film pouch.

    The two bag magazines, feeding action, dosing positions, and safety logic are coordinated in one line. If a bag is missing, the machine is designed not to open, fill, or seal that position and can alarm; the exact interlock and acceptance logic belong in the final configuration. A 10.4-inch touchscreen and PLC-based control give the operator a clear point for recipe and status management, while the exposed product-contact areas use 304 stainless steel.

    Side detail of zpacker paper bag packaging machine with bag magazine, opening area, vertical mechanism, air lines, and standing paper bags

    Engineering view: The key selection question is not only whether a screw doser can weigh flour. It is whether the bag magazine, clamps, dust-removal path, M-fold handling, adhesive sealing, and downstream conveyor can keep the complete paper-bag cycle together. Confirm bag direction, mouth construction, M-side, paper or paper-plastic bonding, and adhesive compatibility before treating a nominal speed as a production promise.

    Match the flour packaging line to weight, bag, and downstream checks

    For a quotation, the mill should provide the actual flour properties, target weights, bag drawings or samples, and the required downstream route. Zpacker can be arranged with screw feeding and twin screw dosing, then connected to a conveyor, checkweigher, metal detector, date printer, bag arranger, and either group shrink wrapping or manual outer-bag packing. These additions turn an isolated packaging machine into an automatic packaging line without assuming that every project needs the same equipment.

    The table below separates reference values from items that must be validated. The approximate speeds are planning figures affected by flour flowability, feeding stability, bag construction, and the final acceptance method. The machine reference power is 15.5 kW, with 380 V ±10%, 50 Hz supply; compressed-air pressure should be confirmed from the final BOM because project documents use different reference ranges.

    Quotation checkZpacker referenceWhy it affects the result
    Retail weightAbout 1–2 kg or 2.5–5 kg by configurationSets the dosing and bag-handling range; test 1 kg, 2 kg, or 5 kg samples.
    Reference throughputAbout 30–35 bags/min for 1–2 kg; about 15–20 bags/min for 2.5–5 kgUse as a planning reference only; final speed depends on material and acceptance conditions.
    Bag formatPremade M-fold square-bottom bag; W about 80–140 mm, L about 240–320 mm, M-side about 60–80 mmBag direction, dimensions, and paper-layer bonding determine opening and sealing stability.
    Dosing and quality controlScrew dosing, about ±0.5% reference accuracy; checkweigher and metal detector can be addedWeight control and foreign-metal detection support retail compliance and product protection.
    Utilities and layoutAbout 0.76 m³/min air consumption; pressure and layout confirmed by final designStable air, feed capacity, and installation space protect cycle continuity and dust control.
    Clean full-line view of zpacker paper bag packaging system with main bagging machine, upper dosing structure, conveyor platform, and right-side downstream unit

    Plan a flour packaging equipment test around your real bags

    Send the flour specification, target 1–5 kg weights, bag samples, expected output, and downstream inspection requirements. BPM can use those inputs to confirm the zpacker configuration, dust-removal route, adhesive sealing method, utilities, and layout before a final offer and acceptance plan.

    Request a Zpacker Packaging Line Review
  • Flour Packaging Line for 1–5 kg Paper Bags: How Zpacker Automates Packing and Dust Removal

    Flour Packaging Line for 1–5 kg Paper Bags: How Zpacker Automates Packing and Dust Removal

    ZPACKER APPLICATION NOTE · FLOUR PACKAGING LINE

    Flour Packaging Line for 1–5 kg Paper Bags: How Zpacker Automates Packing and Dust Removal

    For flour mills, milling complexes, bakeries, and food production plants, Zpacker is a full automatic paper bag packaging machine for pre-made M-fold bags. Its linked bag feeding, screw dosing, filling, settling, dust removal, sealing, and downstream inspection path turns a labor-heavy packing task into a controlled automatic packaging line for common 1 kg, 2 kg, and 5 kg retail formats.

    Wide bright workshop view of zpacker full packaging line with horizontal bagging machine, upper feeding system, conveyor, and bag handling area

    Why flour producers move beyond manual and semi-automatic packing

    A flour mill or food plant serving retail distribution may need several paper-bag formats during the same production week. Manual filling still requires an operator to pick a kraft bag, open it, hold it under the filling point, settle the powder, clean the mouth, fold the M-shaped side gussets, and close the top. A semi-automatic machine can improve dosing, but it may leave bag handling, sealing, and handover to the next process as separate operations.

    This separation becomes costly when the material is dusty and the bag is a pre-made paper or paper-plastic package rather than a film roll. Powder can escape around the mouth, the product may not settle evenly, and a bag that is not correctly oriented cannot move smoothly through folding and sealing. The line therefore needs more than a powder filling machine: it needs a coordinated paper bag handling and sealing sequence.

    Close view of zpacker automatic paper bag feeding and opening station with kraft bags, bag clamps, stainless frame, and touchscreen
    Typical control points in a flour bagging project

    The plant must match the product flow, target weight, bag dimensions, M-fold geometry, bag direction, air supply, and available floor space before selecting equipment. Ignoring any one of these points can create stops between dosing, bag closing, checkweighing, and secondary packaging.

    How Zpacker fits the pre-made M-fold paper bag process

    Zpacker is designed around the actual sequence of a square-bottom, M-fold pre-made bag. A belt-fed bag system takes a flat bag from the magazine, opens it into a stable three-dimensional form, and positions it for filling. The dosing stage can be configured around a twin-screw dosing arrangement for flour and compatible powders. After filling, vibration and dust-removal stations help release air and settle the product before the bag returns to its M-fold shape.

    The closing sequence continues with edge trimming, edge rolling, hot-melt glue application by dot or line spray, and top pressing. This is different from heat sealing a film pouch, so the correct comparison is a premade paper bag packaging machine against the customer’s existing paper-bag workflow—not an assumption that a vertical packaging machine can replace every operation. Paper-plastic bags require confirmation of layer bonding and glue compatibility through the final bag sample.

    Engineering note. The automatic line is strongest when the bag sample and powder are tested together. Bag width, length, side gusset, orientation, flowability, dust behavior, and required speed should be fixed in the final technical proposal and acceptance conditions.

    Reference configuration for 1–5 kg flour packaging

    The available reference range separates smaller and larger retail formats: approximately 30–35 bags per minute for 1–2 kg and approximately 15–20 bags per minute for 2.5–5 kg. Other recorded project discussions cite about 40–50 bags per minute for 1 kg, about 30–35 for 2 kg, and about 16–20 for 5 kg. These figures are reference values only; flour properties, screw dosing, feeding capacity, bag quality, and site conditions determine the final speed.

    A complete flour packaging line can connect a silo or buffer hopper, screw conveyor or elevator, the Zpacker bagging machine, conveyor transfer, checkweigher, metal detector, date printer, bag arranger, and secondary packaging. Multiple small bags may then be grouped in shrink film or placed into a larger outer bag. The PLC controller and touchscreen provide the operating interface, while no-bag, air-pressure, safety, motor, and glue-temperature conditions can trigger protective stops and alarms.

    Selection pointZpacker referenceWhy it matters
    Retail weight1–2 kg or 2.5–5 kg configurationsSets dosing range, bag handling, and expected line speed
    Bag formatPre-made paper or paper-plastic M-fold square-bottom bagControls opening, orientation, folding, glue, and top pressing
    Bag dimensionsReference width 80–140 mm; length 240–320 mm; side gusset about 60–80 mmMust be checked against the actual sample before quotation
    Accuracy and utilitiesAbout ±0.5%; 15.5 kW; 380 V ±10%, 50 Hz; air consumption about 0.76 m³/minSupports utility planning and acceptance discussions
    Quality and logisticsOptional checkweigher, metal detector, marking, arranging, and secondary packagingReduces manual handover after the bag is sealed

    Start with the flour, bag sample, and target format

    Send the powder characteristics, 1 kg/2 kg/5 kg target, bag drawings or samples, expected output, and site utilities. BPM can then define the screw dosing, dust-removal, sealing, inspection, and secondary-packaging path around the actual Zpacker application.

    Discuss your flour packaging line